Why Machine Compliance Matters Before You Place an Order
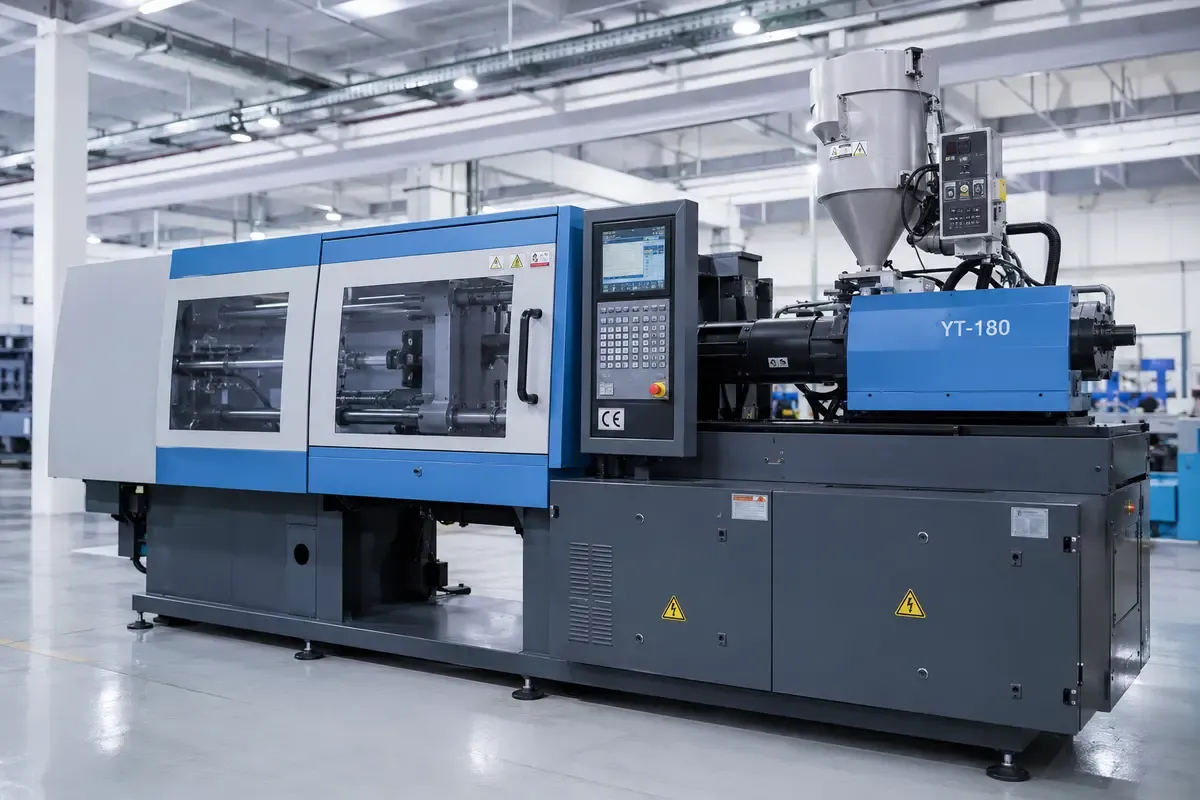
Importing zipper manufacturing machinery is a six-figure decision. A single injection molding machine for zipper components costs $25,000–$120,000, and a complete production line can exceed $500,000. Yet many first-time buyers focus exclusively on price and delivery time — overlooking the certifications that determine whether the equipment clears customs, passes factory inspection, and operates safely under local regulations.
This guide walks you through the three pillars of informed machinery purchasing: mandatory certifications for your target market, technical specifications that drive real throughput, and factory acceptance testing before shipment.
1. Mandatory Certifications by Target Market
European Union: CE Marking
Any zipper machine entering the EU market — injection molding machines, die casting equipment, slitter-rewinders, or ultrasonic welding units — must carry CE marking under the Machinery Directive 2006/42/EC. This is not optional for customs clearance. A valid CE declaration confirms compliance with:
- EN ISO 12100:2010 — Risk assessment and hazard analysis for the entire machine lifecycle
- EN 60204-1 — Electrical safety requirements (critical for PLC-controlled zipper forming machines)
- EN ISO 13849-1 — Safety-related control system performance levels
Buyer's checklist: Request the Declaration of Conformity (not just a CE sticker). Verify the notified body number if Annex IV machinery is involved. Machines with integrated robotic arms or automated feeding systems often require Annex IV assessment.
North America: UL / CSA
For the US and Canadian markets, electrical components on zipper machinery must meet UL 508A (industrial control panels) or CSA C22.2 No. 301 standards. While full machine UL listing is not always mandatory, local electrical inspectors will require evidence of compliance for installation permits. Many zipper machine exporters now pre-fit UL-listed components (Siemens, Allen-Bradley, Schneider) to streamline buyer-side approval.
Southeast Asia & Middle East: ISO 9001 + Local Variants
Markets like Vietnam, Indonesia, and the UAE accept ISO 9001:2015 as the baseline quality management credential. However, specific machinery may require additional local certifications — for example, SIRIM in Malaysia or SASO in Saudi Arabia. Confirm with your importer before finalizing the purchase agreement.
2. Technical Specifications: What the Brochure Won't Tell You
Datasheets list cycle times and motor power, but three often-overlooked specs determine real-world profitability:
| Specification | Why It Matters | What to Verify |
|---|---|---|
| Actual vs. Theoretical Cycle Time | Brochure numbers assume ideal conditions. Real production involves material variation, mold changes, and operator breaks. | Request a video of continuous operation over 2+ hours. Calculate average cycle time from the recording — not the spec sheet. |
| Changeover Time | A machine producing 5 zipper sizes can lose 15-20% of shift time to changeovers if not designed for quick mold swaps. | Ask for the SOP on mold/size changeover. Target: under 30 minutes per changeover for injection molding machines. |
| Energy Consumption per Unit | Energy costs represent 8-15% of zipper manufacturing overhead. Servo-driven machines consume 30-50% less than hydraulic equivalents. | Request kWh-per-1000-cycles data. Compare servo-hydraulic vs. full-electric configurations. |
3. Factory Acceptance Testing (FAT): Your Last Line of Defense
The FAT is your opportunity to verify every specification before the machine leaves the supplier's floor. A well-structured FAT for zipper machinery should include:
- Dimensional accuracy test — Run 500 consecutive zipper components and measure key dimensions against tolerances (typically ±0.05mm for injection-molded slider bodies)
- Endurance run — 8-hour continuous operation with your specified raw material. Monitor temperature, noise level, and reject rate
- Safety interlock verification — Test every emergency stop, light curtain, and guard switch under operating conditions
- Spare parts audit — Verify the recommended spare parts kit against the machine BOM. Critical wear components (heating bands, nozzles, seals) should be included
Pro tip: Document the FAT with time-stamped photos and video. This evidence is invaluable if disputes arise during installation and commissioning at your factory.
4. Supplier Evaluation Beyond the Trade Show Booth
A glossy catalog does not equal manufacturing capability. Before committing to a purchase order, verify:
- Export track record: Request at least three references for machines shipped to your region within the last 24 months. Contact them.
- After-sales infrastructure: Does the supplier have English-speaking service engineers? What is the guaranteed response time for remote troubleshooting? Is there a local agent or partner in your country?
- Spare parts availability: Ask for the delivery lead time on five critical spare parts. If any part exceeds 14 days, negotiate a consignment stock arrangement.
5. Total Cost of Ownership: Look Beyond the Invoice Price
| Cost Component | Typical % of Machine Price | Timing |
|---|---|---|
| Machine purchase | 100% | Pre-shipment |
| Ocean freight + insurance | 5–8% | Pre-shipment |
| Import duties & customs brokerage | 3–15% (varies by HS code & country) | At arrival |
| Installation & commissioning | 3–5% | Post-arrival |
| Annual maintenance & spares | 5–8% per year | Ongoing |
| Operator training | 1–2% | Post-installation |
A $50,000 machine typically incurs an additional $10,000–$18,000 in logistics, duties, and first-year operating costs. Factor this into your capital expenditure planning from day one.
Key Takeaways for Zipper Machinery Buyers
✅ Verify CE/UL/ISO 9001 certifications before issuing a purchase order — not after production starts.
✅ Look past brochure cycle times. Validate throughput with continuous-operation video and request energy consumption data per 1,000 cycles.
✅ Invest 3–5 days in an on-site Factory Acceptance Test. The cost of travel is trivial compared to the cost of commissioning a non-compliant machine.
✅ Budget freight, duties, installation, and first-year spares as part of the total investment — not as afterthoughts.
✅ Evaluate the supplier's after-sales capability with the same rigor you apply to machine specifications. A machine without service support is a liability.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| Factory quality system | ISO 9001-style management with QC gates | Continuous | Documented procedures for each process |
| Incoming material | Yarn, wire, pellets, chemicals certificate | Every batch | Material traceability to supplier batch |
| In-process control | Process checkpoints per line | Per shift | Parameters recorded and signed |
| Final inspection | Pull force, slider, appearance, AQL | Per lot | AQL 2.5 sampling; records kept for claims |
| Testing equipment | Pull-force, cycling, salt spray, color fastness | Calibrated | Calibration schedule and records |
| Staff assessment | Skill matrix and first-pass yield per operator | Weekly | Training plan tied to defect data |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Raw material & warehouse | 15% | Yarn, wire, pellets and chemicals with FIFO storage |
| Production zones | 55% | One flow per product line; separate dyeing/plating/painting zones |
| QC & lab | 10% | Pull-force, cycling, salt spray and color fastness equipment |
| Packing & finished goods | 15% | Dust-free packing and storage |
| Utilities & treatment | 5% | Air, cooling water, wastewater and exhaust |
| Planning reference | — | Small 200–400 m²/150–250 kW; medium 600–1,000 m²/300–500 kW |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Line operators | Machine operation and process checks | 1–2 weeks per station | Output/shift; defect rate; stop time |
| Technicians | Mechanical, electrical and mold maintenance | 2–4 weeks + on-site | MTTR; preventive maintenance compliance |
| Process engineer | Parameter setting, problem solving, training | Project-based | First-pass yield; complaint rate |
| QC inspectors | Inspection, testing, AQL sampling | 1–2 weeks | Missed-defect rate; report accuracy |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Capacity mismatch after start-up | Line designed without real product mix | Define sizes and mix first; start one line, stabilize, then expand |
| Color contamination between materials | Different fibers dyed in same machine | Separate dyeing by material; acid dyes for nylon, disperse for polyester, reactive for cotton |
| Wastewater/environment approval delays | Treatment planned too late | Plan dyeing/plating/painting permits before line design |
| Power instability | No power plan before installation | Confirm local voltage/frequency and total kW; add stabilizers if needed |
| Operator quality varies | No training or assessment system | Use skill matrix, weekly defect review and first-pass-yield targets |
| Machine downtime high | No spare parts stock | Keep critical wear parts in stock; QLQ supplies spares with long-term support |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Factory Planning Data
Reference values from QLQ new-factory quick tables and real customer projects. Confirm with your line supplier before specification.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| Small factory reference | 10,000–20,000 pcs/day: USD 80k–150k equipment; 200–400 m²; 150–250 kW; 15–35 staff | Under-budgeting utilities or staff = slow start-up and quality swings |
| Medium factory reference | 30,000–50,000 pcs/day: USD 150k–300k equipment; 600–1,000 m²; 300–500 kW; 30–90 staff | Scope creep on product mix raises both area and power needs |
| First-line rule | Start with one complete line for one product type | Mixed lines at start = training gaps and higher defect rates |
| Stabilization period | 3–6 months before adding capacity | Expanding too early multiplies problems before they are solved |
| Voltage options | 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz, 480V/60Hz | Confirm before order; wrong voltage costs installation time |
| On-site support | 1–2 engineers for 7–15 days; longer support by arrangement | First factories benefit most from on-site commissioning and training |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Complete equipment line | Front-end, finishing and surface treatment machines for nylon, metal and plastic zippers |
| Molds & tooling | Slider, teeth and stop molds with 0.02 mm precision and long-life steel |
| Materials & consumables | Chemicals, lacquer, polishing media, films, wires and spare parts with long-term supply |
| Full-process capability | From raw material through weaving, forming, finishing, electroplating and painting - one responsible supplier |
| Turnkey services | Layout design, installation, commissioning, operator/technician training and remote support |
| Proven delivery | 10,000 m² self-owned plant, 35 senior engineers, export to 60+ countries |
Frequently Asked Questions
Where should a new zipper factory start?
Start with a clear product plan: product type, target daily output, workshop size, power supply and whether you have technical staff. QLQ prepares a customized machine list, layout and quotation from these answers.
How much investment does a new factory need?
A small factory at 10,000–20,000 pieces/day is around USD 80,000–150,000 for equipment; a medium factory at 30,000–50,000 pieces/day is around USD 150,000–300,000. This excludes building, utilities and working capital.
Should I buy one line at a time or the full line?
For a first factory, buy one complete line for one product type, run it 3–6 months, train the team, then expand. QLQ supports phased investment.
Can QLQ send engineers to install and train?
Yes. Online support is free; on-site commissioning with 1–2 engineers for 7–15 days is recommended for new factories, and longer technical support can be arranged. The customer covers visa, flights, hotel and meals.
Do zipper factories need environmental approval?
Usually yes when dyeing, plating or painting is in-house. Small factories can outsource plating/dyeing; medium factories should plan wastewater treatment and exhaust with the line design.
Can machines be customized for our voltage and frequency?
Yes. Common options include 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz and 480V/60Hz three-phase. Confirm the local standard and it is included in the PI.
What support is available after delivery?
Installation and commissioning, operator/technician training, spare parts and consumables supply, process optimization and remote troubleshooting form a closed support loop.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Zipper Production Workshop
Whether you produce nylon, metal or plastic zippers, every profitable factory starts with the same planning data: quality standards, space, people, power and output targets. The table below summarizes realistic planning figures for a typical mid-size multi-type zipper workshop.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | ISO 9001 quality system with BS 3084 / ASTM D2061 / QB/T 2171 testing; incoming material inspection; in-process QC at each station; pull-force, slider cycling and color-fastness tests per batch; final AQL 2.5 sampling before packing. |
| Workshop Area Required | 1,000–2,500 m² for a complete multi-type line (nylon and plastic, or metal), plus 200–400 m² warehouse; ceiling height above 4.5 m; separate dyeing, plating (if any), assembly and packing zones. |
| Workforce Needed | 20–50 workers across two shifts: line operators, 2–4 machine technicians, 2–4 QC inspectors and 1–2 production managers; more staff are required when plating is done in-house. |
| Power Supply | 150–400 kW connected load depending on line type; 380V/50Hz three-phase (or 220V/480V 60Hz); compressed air at 0.6–0.8 MPa; water supply for dyeing, cooling or plating. |
| Daily Production Capacity | Finished zippers: 8,000–20,000 pcs/day across sizes #3–#10; chain production: 5,000–15,000 m/day, depending on the number and type of lines. |
| Estimated Gross Margin | 18%–30% on finished zippers; in-house dyeing, finishing and a balanced product mix support the higher end of the range. |
| Typical Investment Range | $150,000–350,000 for a complete mid-size multi-type line, excluding building construction and local environmental permits. |
| Typical Payback Period | 18–30 months at 70% average utilization with steady order volume. |
Quality First
- Test pull force and slider cycling on every batch
- Run incoming material inspection on all yarns and parts
- Keep in-process QC records at every handover
- Use AQL 2.5 sampling before shipping
Workshop & Power
- Plan production, warehouse and utility zones clearly
- Provide stable three-phase power with surge protection
- Ensure ventilation for dyeing, heating or plating areas
- Keep a dust-free packing and storage zone
People & Profit
- Train operators and technicians before production starts
- Assign QC inspectors to each major process
- Gross margin target: 18%–30%
- Payback target: 18–30 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Planning a new zipper factory or upgrading an existing workshop? Contact QLQ Machinery for a complete line design, equipment list and quotation matched to your target capacity.