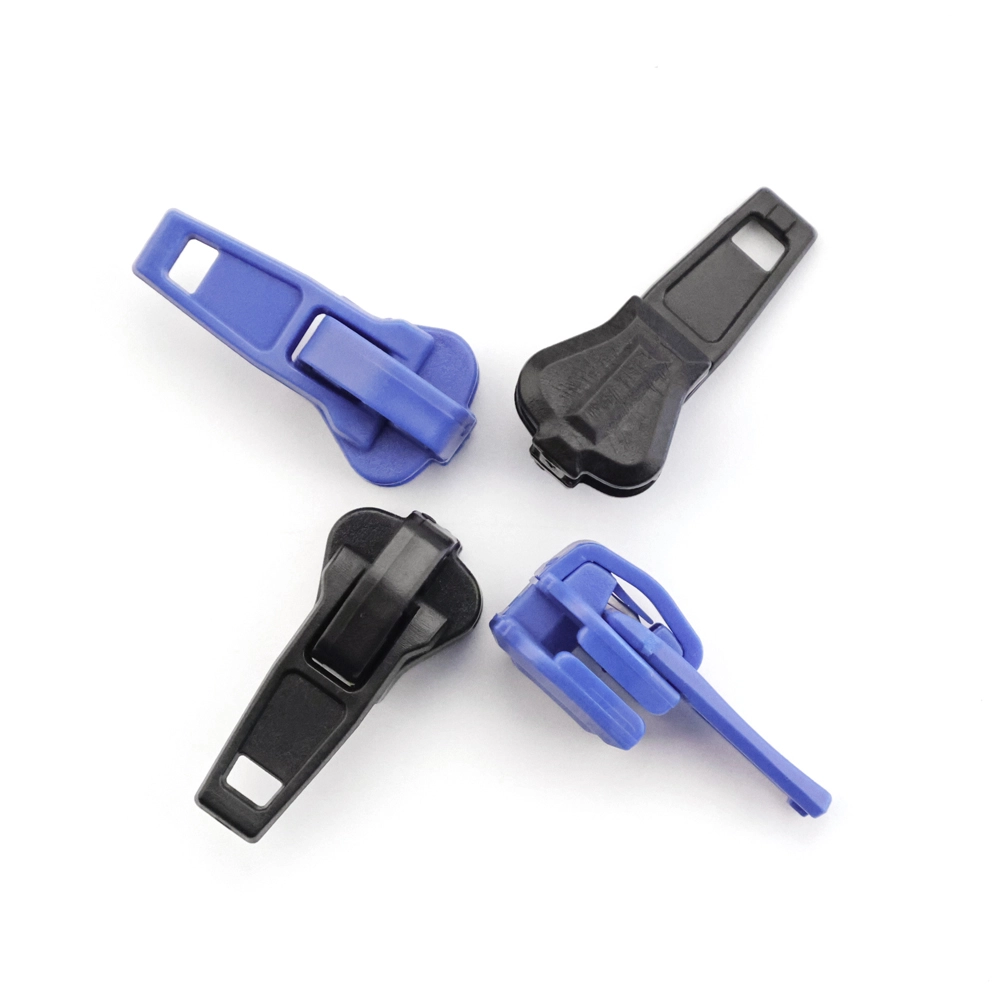
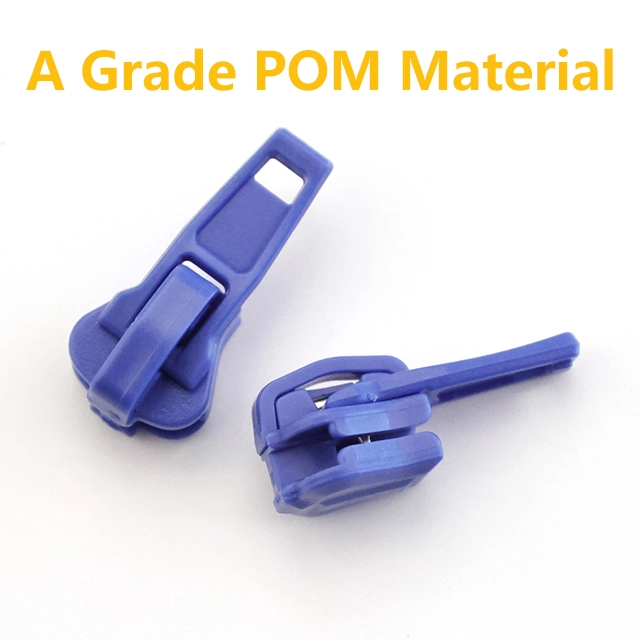
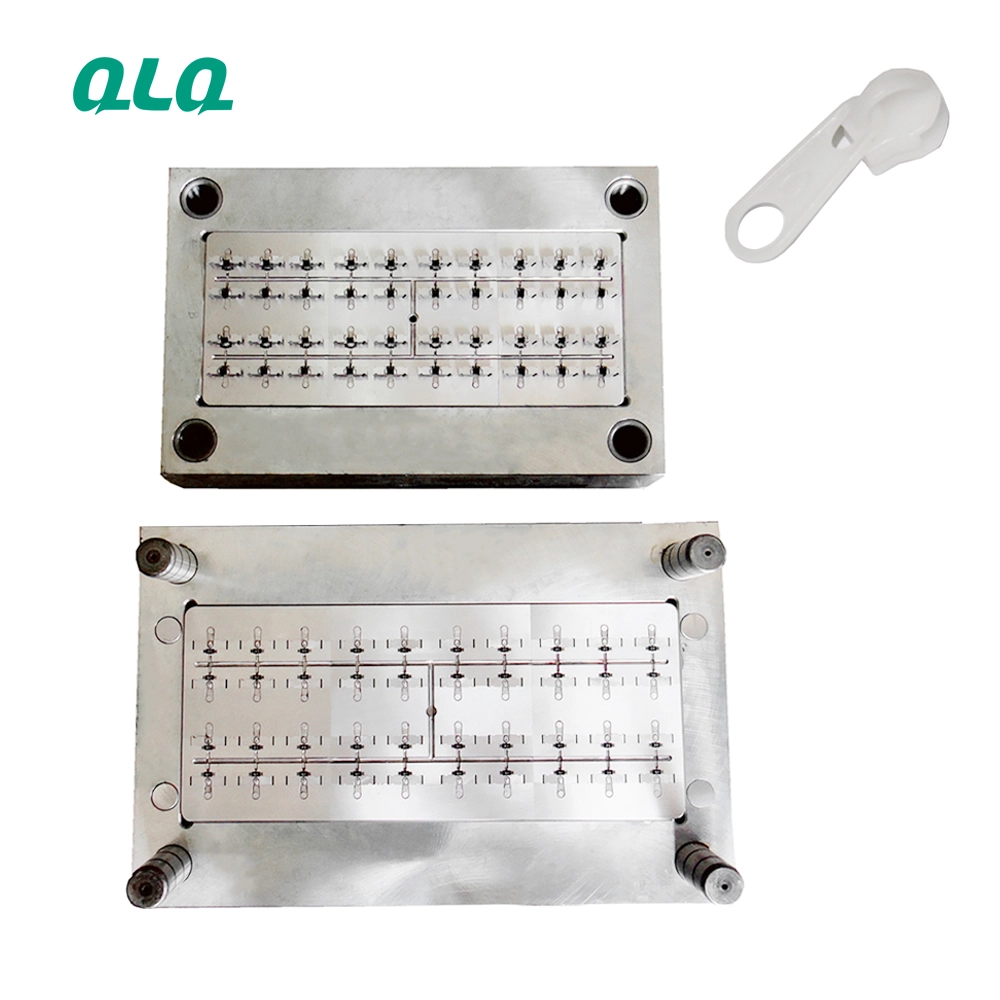
A POM slider either fits the chain or it does not, and the difference is measured in tenths of a millimeter. The channel that runs on the chain teeth, the hole that holds the puller and the locking surfaces all start as a steel cavity enlarged for 1.8-2.5% POM shrinkage, and every degree of mould temperature drift moves the finished size.
This guide explains dimensional control for POM sliders: what to measure, which tolerances matter, how shrinkage and mould temperature change dimensions, and how to check fit against #3, #5 and #8 zipper chain before the slider reaches assembly.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Measuring only length | Channel and hole defects pass unnoticed | Measure channel width, puller hole and lock geometry too |
| 2. Checking size when cold only | Parts measured hot differ after full cooling | Allow parts to reach room temperature before measuring |
| 3. Ignoring mould temperature drift | Same settings, different size on a cold morning | Record mould temperature; keep 60-90C stable |
| 4. One caliper for everything | Operator pressure changes readings | Use fixed gauges for channel and hole dimensions |
| 5. No fit gauge for the chain | Slider passes caliper but jams on the actual chain | Run the slider on a reference chain sample |
| 6. Sampling only the first cavity | Cavity-to-cavity differences hidden | Check each cavity group at setup and hourly |
| 7. No tolerance written on the drawing | Operators guess what is acceptable | Define critical dimensions and limits per size |
| 8. Reusing worn gauges | Calibration drift passes bad parts | Calibrate and check gauges on a schedule |
| 9. Mixing sizes in one box | Wrong slider reaches assembly | Separate and label by size after inspection |
| 10. No record of measurements | You cannot prove or improve fit | Log measurements per batch and size |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Define critical dimensions and tolerances for every slider size
- Measure at room temperature after full cooling
- Use fixed gauges for channel and puller-hole dimensions
- Run a reference chain fit test at setup and hourly
- Check every cavity group during setup
- Keep mould temperature stable in the 60-90C window
- Calibrate calipers, gauges and projectors on a schedule
- Log batch measurements for traceability
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Dimensional control data for POM sliders
Reference values from QLQ slider notes; the drawing of your specific size defines the exact tolerances.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| POM shrinkage | 1.8-2.5% | The cavity is cut larger; if the allowance is wrong the part is undersized or oversized |
| Channel width | Must match the chain teeth of the size | Too tight gives rough slide feel; too loose gives rattling and weak grip |
| Puller hole diameter | Per puller design | Too small breaks assembly; too large gives a loose puller |
| Mould temperature | 60-90C stable | A 10C drift can move dimensions enough to change fit |
| Cooling time | 3-8 seconds | Short cooling causes warpage and size drift |
| Measurement condition | Room temperature | Hot parts measure differently and mislead the process |
| Gauge precision | 0.02 mm where possible | Match gauge resolution to the tolerance being checked |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Which dimensions matter by function
| Channel width | Runs on chain teeth | Slide feel and grip |
| Puller hole / slot | Holds the puller | Assembly and puller retention |
| Lock geometry | Engages the locking tooth | Auto-lock function |
| Overall length / width | Product envelope | Customer fit and appearance |
| Top and bottom clearance | Runs between teeth and tape | Smooth movement |
Measurement method by dimension
| Overall length | Digital caliper | Caliper calibrated and zeroed |
| Channel width | Fixed go/no-go gauge | Removes operator pressure error |
| Puller hole | Pin gauge or projector | Pin gauge is fastest in production |
| Lock geometry | Projection gauge | Check against the master profile |
| Chain fit | Run on reference chain | Final functional check |
Inspection frequency
| At setup | First pieces from every cavity group | Full dimension and fit check |
| Hourly | Sample per machine | Channel, hole and fit |
| Every color change | First pieces after purge | Size and appearance |
| Per batch before packing | Final sample set | Records with batch label |
| Weekly | Gauge check against master | Calibration drift control |
Implementation Cases
Case 1 - rough slide feel traced to channel tolerance drift
Situation. A POM slider user in Turkey reported rough slide feel on #5 nylon chain, although length measurements were in tolerance.
Approach. The factory added a fixed channel-width gauge and a reference chain fit test. The mould temperature log showed the channel dimension drifting when the mould ran cooler in the morning shift.
Outcome. The temperature was stabilized at the set value, the channel went back into range, and the rough-feel complaints stopped.
Case 2 - cavity-to-cavity differences caught by per-cavity sampling
Situation. A producer in India shipped a batch where one box of sliders jammed on assembly while the rest were fine.
Approach. Per-cavity sampling showed two late-filling cavities produced slightly oversized channel walls. The mould gate balance was corrected and the QC sheet added a per-cavity column.
Outcome. The defect was contained to identifiable boxes and corrected at the mould; assembly jams dropped after the fix.
Frequently Asked Questions
Why do POM sliders come out undersized?
POM shrinks 1.8-2.5% after molding. If the mould cavity was not compensated, the finished slider is undersized. Check the cavity dimensions against the drawing before cutting steel.
How do I measure the slider channel?
Use a fixed go/no-go channel gauge rather than a caliper. The gauge removes operator pressure error and matches the tolerance of the chain fit.
Why does my slider size change between shifts?
Mould temperature drift is the usual cause. The same settings produce different sizes when the mould runs at 65C instead of 80C. Log and stabilize mould temperature in the 60-90C range.
Should I measure parts right after ejection?
No. Let parts cool to room temperature first. Hot parts measure differently and mislead your process decisions.
What is the best functional check for a slider?
Run it on a reference chain sample of the correct size. A slider can pass the caliper and still jam if the channel geometry is wrong.
How tight should the slider fit the chain?
Tight enough to grip without rattling and free enough to slide smoothly. The correct fit is defined by the chain size and the customer feel requirement; test on the reference chain.
How often should I check dimensions?
Full first-piece check at setup from every cavity group, then hourly samples during the run, and a final sample per batch before packing.
How precise do my gauges need to be?
Match the gauge resolution to the tolerance. For critical mating surfaces, 0.02 mm-level measurement or projection gauges are appropriate; calipers alone are not enough for channel geometry.
What Would You Like to Solve?
Send us your slider drawing, the chain size it must fit and your current measurement records, and we can help you set the critical dimensions, choose the right gauges and build the fit test that catches problems before assembly.
Published by QLQ - a complete high-quality zipper manufacturing equipment, moulds and materials solution supplier, and the only supplier in China covering the full process chain from raw material through electroplating and painting as one integrated system. Values cited are project references; confirm with your line supplier before specification.