Why Surface Finishing Defines Your Zipper's Market Value
A metal zipper's raw chain is unfinished. The difference between a $0.05 commodity zipper and a $0.50 premium branded zipper sits in the surface finishing process: chamfering, polishing, electroplating, color fixing, and lacquering. Each step transforms rough stamped metal teeth into smooth, corrosion-resistant, visually consistent fasteners that apparel brands and automotive manufacturers demand. This guide walks through every finishing station and the equipment that powers it.
The Metal Zipper Surface Finishing Workflow
Metal zipper surface treatment follows a strict sequential workflow. Skipping or compromising any stage produces visible defects that buyers reject on first inspection. Here is the complete production chain:
Stage 1: Teeth Chamfering — The Foundation of Smooth Operation
After stamping, metal zipper teeth have sharp burrs and inconsistent edges. Chamfering machines use abrasive media or CNC-controlled grinding heads to deburr every tooth profile uniformly. Without proper chamfering, zippers feel rough during operation and wear out sliders prematurely — the number one complaint from garment manufacturers.
Stage 2: Surface Polishing — Achieving Mirror-Level Consistency
Polishing removes micro-scratches and creates a uniform surface texture that determines how plating chemicals bond to the metal. Intelligent polishing machines with 12 or more wheel stations process zipper chains through progressively finer abrasive grits. Advanced models feature PLC-controlled pressure adjustment, compensating for wheel wear in real-time to maintain consistent finish quality across an entire production shift.
Stage 3: Electroplating — The Color Chemistry
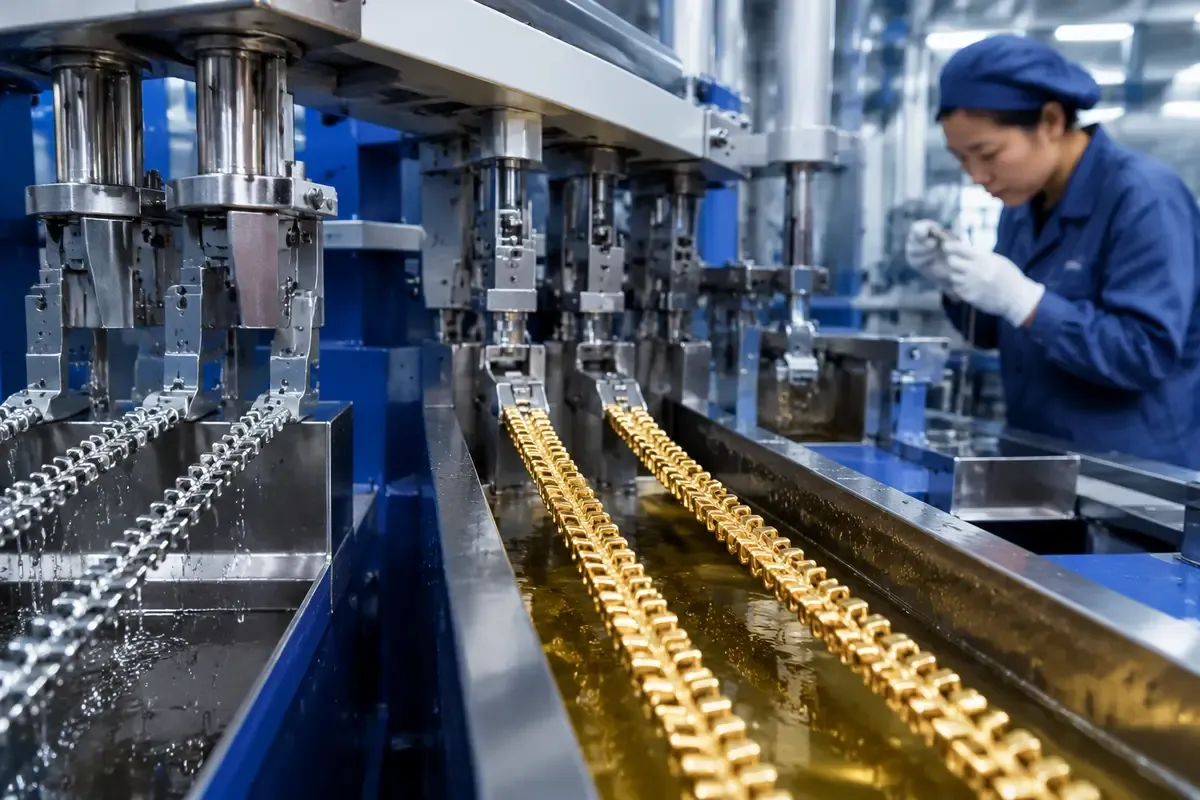
This is where the zipper gets its final appearance: gold, silver, bronze, antique brass, gunmetal, black nickel, and hundreds of custom shades. Chemical cold plating machines run zipper chains through precisely controlled chemical baths — single-tank for single-color production, dual-tank for two-color or gradient finishes.
Single-Tank vs Dual-Tank Plating
| Single-Tank (QLQ-CCPMS) | One color per pass. Ideal for bulk gold or silver orders. Lower chemical cost. Simpler maintenance. |
| Dual-Tank (QLQ-CCPMD) | Two colors or two-step processes in one continuous line. Perfect for antique finishes (base coat + top coat) and two-tone designs. |
Stage 4: Cleaning & Color Fixing — Locking the Finish
Post-plating, residual chemicals can continue reacting with the metal surface, causing uneven color development or premature tarnishing. Cleaning and color-fixing machines run plated zippers through neutralizing baths that halt the chemical reaction at exactly the target shade. This stage is non-negotiable for zippers destined for export markets with strict corrosion-resistance standards (ISO 9227 salt spray testing).
Stage 5: Lacquering — The Protective Seal
The final finishing stage applies a transparent protective lacquer that seals the plated surface against oxidation, UV damage, and mechanical wear. Crystal lacquer machines apply an even coating measured in microns — too thin and protection fails; too thick and the zipper loses its metallic sheen. Modern machines use multi-chamber curing zones to bake the lacquer at controlled temperatures, producing a durable gloss or matte finish.
Production Line Planning: Capacity & Investment
A complete metal zipper surface finishing line capable of 100,000 meters per month requires approximately 150-200 m² of floor space and 3-5 operators. Equipment investment ranges from $80,000 to $250,000 depending on automation level and plating chemistry complexity. The typical payback period for a full finishing line serving export customers is 12-18 months when running at 70%+ capacity.
Pro Tip: Test Your Chemistry with Your Water
Plating chemical formulations are sensitive to local water hardness and mineral content. Before finalizing your equipment order, send a water sample to your chemical supplier for compatibility testing. A plating line optimized for your specific water chemistry runs 23% more efficiently and produces 31% fewer color-rejection batches — verified across our client installations in Southeast Asia, South Asia, and the Middle East.
Ready to build your metal zipper finishing line? Explore our complete range of chamfering, polishing, plating, color-fixing, and lacquering machines — each backed by CE certification, on-site installation, and comprehensive operator training programs tailored to your production goals.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| Wire receiving | Material certificate, gauge and hardness | Every coil | Brass, aluminum or steel wire per order spec |
| Y-teeth stamping | Teeth shape, pitch and burr | Every 30 min | No deformed teeth; uniform pitch across the chain |
| Combining / tape fixing | Teeth alignment and tape lock | Every 2 h | No loose teeth; alignment within tolerance |
| Polishing | Surface finish and media residue | Per batch | No deep scratches; clean media wash before plating |
| Plating | Thickness, adhesion, salt spray | Per batch | Nickel 3–5 µm; 24–48 h salt spray; no bare recesses |
| Finished zipper | Pull force, slider glide, AQL | Per lot | Pull force per BS 3084; AQL 2.5 before packing |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Wire & stamping | 25% | Wire flattening/straightening and Y-teeth stamping close together; dust extraction |
| Polishing | 20% | Centrifugal, vibratory and magnetic machines; water and sludge handling |
| Plating (in-house) | 25% | Isolated line with fume extraction, rectifiers and wastewater treatment |
| Finishing & packing | 30% | Gapping, stops, slider mounting, cutting, QC and packing in one flow |
| Utilities | — | Air compressor, dust collection, wastewater; power per plan (110–280 kW) |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Stamping operators | Die set-up, speed/pitch adjustment, burr inspection | 1–2 weeks | Output per shift; burr defect rate; die change time |
| Polishing staff | Media selection, cycle time, residue wash | 1 week | Surface reject rate; media consumption per kg |
| Plating technician | Bath control, rectifier settings, thickness testing | On-site QLQ training | First-pass plating yield; thickness variance |
| QC inspector | Salt spray, pull force, AQL sampling | 1–2 weeks | Missed-defect rate; test report accuracy |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Plated finish looks dull | Low brightener, high bath temperature, wrong current density, poor pre-cleaning, contamination | Check brightener and bath temperature; verify current density and time; improve pre-cleaning; filter bath |
| Salt spray test fails early | Plating too thin, porosity, no topcoat, base material condition | Increase thickness to 3–5 µm; improve pre-treatment; add anti-oxidation topcoat |
| Teeth misaligned after stamping | Wire hardness variation, worn dies, speed drift | Check wire batch and hardness; inspect dies; stabilize machine speed |
| Aluminum teeth break or chip | Tooling not matched to aluminum, wrong feed | Use aluminum-matched dies and cutters; reduce speed for aluminum |
| Plating rejects at recesses | Complexing agent or brightener imbalance, low agitation | Check bath composition; improve agitation; adjust rack/barrel loading |
| Plating wastewater permit issues | No treatment plan before line design | Design wastewater treatment with the line; confirm local discharge standards early |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Metal Zipper Process Data
Reference values from QLQ project data and standard metal zipper practice. Confirm final parameters with your line supplier.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| Y-teeth stamping speed | Mechanical 60–90 strokes/min; servo 100–150 strokes/min | Higher speed = higher output but demands stable wire gauge; drift = burrs and misaligned teeth |
| Plating thickness (nickel) | 3–5 µm on decorative metal zippers | Below 3 µm = salt spray failure; above range = cost and flexibility issues |
| Salt spray test | 24–48 h neutral salt spray per target | Early rust = thickness, porosity or missing topcoat, not just bath quality |
| Rectifier sizing | Small line 200–400A/12V; medium 600–1000A | Under-sized rectifier = long plating time and uneven thickness |
| Polishing cycle | Match media and cycle to surface target | Over-cycle = thin walls on teeth; under-cycle = scratches visible after plating |
| Aluminum pretreatment | Zincating or anodizing preparation before nickel/color | Skipping pretreatment = poor adhesion and patchy color on aluminum |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Front-end equipment | Wire flattening/straightening, Y-teeth stamping, combining, water wash and ironing |
| Surface treatment | Polishing machines and media; electroplating lines with rectifiers and filter pumps |
| Finishing equipment | Gapping, bottom/top stops, slider mounting, cutting and testing machines |
| Molds & tooling | Teeth dies, stop molds and inserts; 0.02 mm precision, H13/SKD61 steel |
| Materials & consumables | Plating chemicals, lacquer, polishing media, wires and spare parts with long-term supply |
| Services | Layout design, plating line guidance, installation, training and remote support |
Frequently Asked Questions
Can aluminum long-chain zippers be plated?
Yes, but aluminum needs special pretreatment such as zincating before nickel or color plating. Tell QLQ the chain size, finish color and current line configuration for the right process and chemicals.
How do I choose a plating rectifier?
A small line with 4–6 tanks usually needs 200–400A/12V; a medium line with 8–12 tanks needs 600–1000A. Confirm tank count, voltage (usually 12V/24V) and target output.
Centrifugal or vibratory polishing for metal zippers?
Centrifugal barrels are faster and brighter for high volume; vibratory finishing is gentler for delicate parts. Many factories use both: rough polish then fine finish.
Can brass and aluminum Y-teeth share one machine?
The machine frame can be shared, but dies, cutters and forming tools differ because the materials have different hardness and elongation. Plan a separate tooling set per material.
What is a reasonable salt spray target for metal zippers?
Brass Y-teeth with proper nickel plating and topcoat commonly pass 24–48 hours neutral salt spray. Confirm the end product and required hours before specifying the plating combination.
Do I need wastewater treatment for an in-house plating line?
Yes, plating wastewater contains heavy metals and chemicals. QLQ supplies basic precipitation, flocculation and filtering systems; confirm local discharge standards with an environmental consultant.
What testing machines should a metal zipper factory own?
At minimum a pull-force tester, salt spray tester and slider glide tester; add washing and color fastness testers when supplying international brands.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Metal Zipper Production Workshop
Metal zipper production combines stamping, polishing, plating and finishing, so site planning must include wastewater treatment and environmental compliance. The table below summarizes realistic planning figures for a typical mid-size metal zipper line.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | BS 3084 / QB/T 2171 compliance with hourly teeth-shape and pitch gauging; plating thickness control (nickel 3–5 µm); salt-spray resistance of 24–48 hours; pull-force, slider glide and cycling tests on every batch; final AQL 2.5 sampling. |
| Workshop Area Required | 800–2,000 m² production area plus 200–400 m² warehouse; electroplating section isolated with fume extraction and a wastewater treatment area of 100–200 m²; separate polishing and assembly zones. |
| Workforce Needed | 15–35 workers across two shifts: stamping and chain operators, polishing staff, assembly operators, 1–2 plating technicians, 2 QC inspectors and 1 production manager. |
| Power Supply | 180–400 kW connected load (plating rectifiers are the largest consumer); 380V/50Hz three-phase (or 220V/480V 60Hz); 10–30 m³/day of rinse water; compressed air at 0.6–0.8 MPa. |
| Daily Production Capacity | Metal chain: 5,000–12,000 m/day; finished metal zippers: 6,000–15,000 pcs/day for sizes #2–#10, depending on plating capacity and shift pattern. |
| Estimated Gross Margin | 20%–35% on finished metal zippers; in-house plating and lacquering add the highest value and improve margin stability. |
| Typical Investment Range | $180,000–320,000 for a complete mid-size metal line including polishing, plating, rectifier and finishing equipment. |
| Typical Payback Period | 15–28 months at 70% average utilization with steady export orders. |
Quality First
- Gauge teeth pitch and shape hourly during stamping
- Measure plating thickness on every batch
- Run salt-spray tests for 24–48 hours per batch
- Test pull force and slider cycling before packing
Site & Environment
- Isolate the plating line with fume extraction
- Budget for wastewater treatment and permits
- Use stable three-phase power for rectifiers
- Keep polishing area separated from packing
People & Profit
- Certify plating operators and technicians
- Assign QC to plating thickness and adhesion
- Gross margin target: 20%–35%
- Payback target: 15–28 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Planning a metal zipper plant with in-house plating? Contact QLQ Machinery for a complete line layout, environmental-planning guidance, machine list and quotation.