The Production Line That Makes or Breaks Your Business
A zipper factory's profitability is determined not by individual machines, but by how those machines work together. An incorrectly laid-out production line wastes 15-30% of floor space and creates bottlenecks that throttle output. This guide covers the four pillars of production line planning: defining your product mix, selecting the right equipment, designing an efficient layout, and calculating realistic output capacity — so you can commission a line that delivers ROI from day one.
1. Define Your Product Mix Before Buying Any Machine
The single most expensive mistake in production line planning is purchasing universal equipment before defining what you will actually produce. Different zipper types require fundamentally different machine configurations:
Metal Zipper Line
Core Machines: Tooth-forming press, slitter, deburring tumbler, chain assembly machine, top/bottom stop machine, slider mounting machine
Production Speed: 800-1,500 meters per shift
Key Investment: Die sets for each zipper size (#3-#10)
Nylon Coil Zipper Line
Core Machines: Monofilament coiling machine, sewing machine, tape feeding system, cutting & gapping machine
Production Speed: 1,200-2,500 meters per shift
Key Investment: Single-needle vs. double-needle sewing configuration
Plastic Injection-Molded Line
Core Machines: Injection molding machine, mold tooling, ultrasonic welding unit, auto-packaging line
Production Speed: 30,000-80,000 pieces per shift
Key Investment: Multi-cavity molds (8-32 cavities)
Pro Tip: If you plan to produce multiple zipper types, calculate the breakeven volume for each separately. It is often more profitable to run two dedicated lines at 85% capacity than one mixed line at 65% with constant changeovers.
2. Production Line Layout: Three Proven Configurations
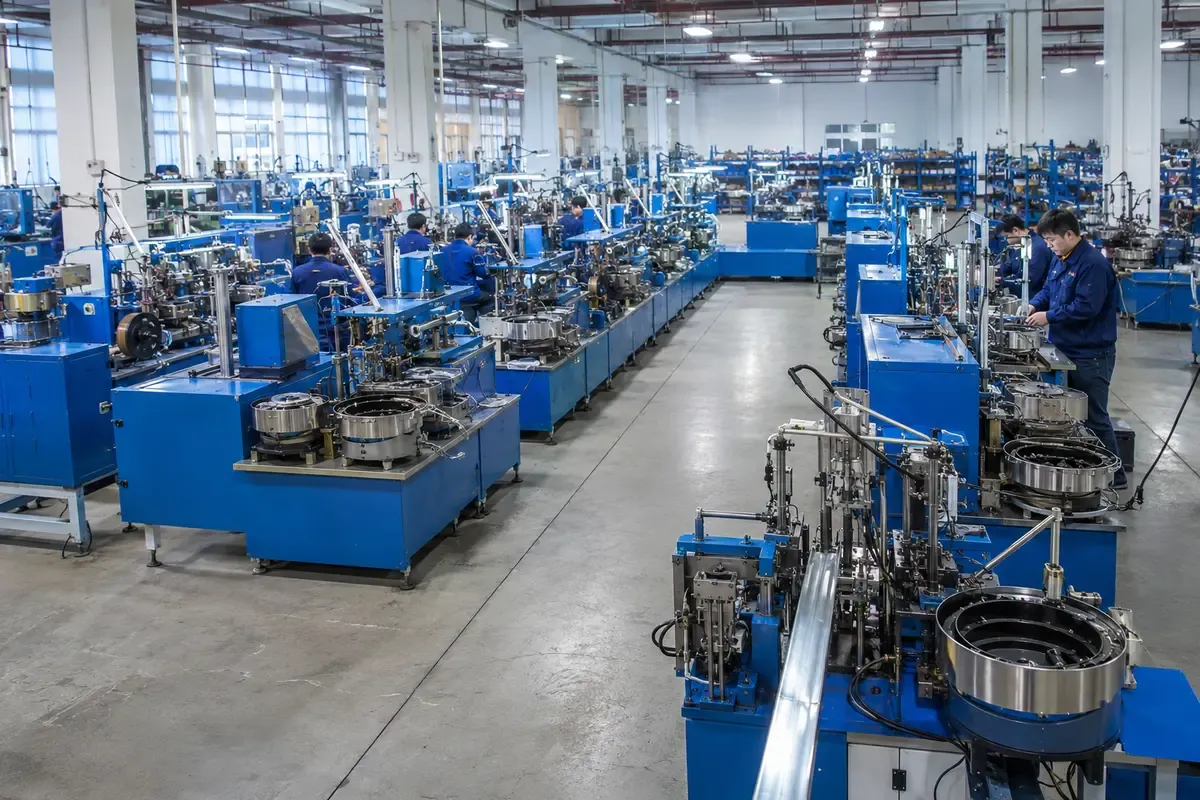
Factory layout directly affects material flow, operator efficiency, and future scalability. Below are three layouts tested across 200+ zipper factories:
| Layout Type | Best For | Space Efficiency | Scalability |
|---|---|---|---|
| U-Shaped | Single zipper type, high volume | Excellent | Moderate |
| I-Shaped (Linear) | Multiple zipper types | Good | Excellent |
| L-Shaped | Limited floor space | Very Good | Limited |
Allocate 18-25 m2 per machine station. Add 30% for material staging, QC stations, and walkways. A 6-machine metal zipper line needs approximately 180-220 m2 of production floor.
Most zipper machines require 380V three-phase power. Plan for 5-15 kW per machine. Compressed air (6-8 bar) is essential for pneumatic components — factor in a 15-30 HP air compressor.
3. Capacity Calculation: From Theory to Production Floor
Brochure speeds are theoretical. Real-world output depends on changeover time, material quality, operator skill, and maintenance downtime. Use this formula:
Daily Output = Rated Speed x Shift Hours x 60 x OEE
OEE = Availability (x0.92) x Performance (x0.85) x Quality (x0.95) = approx 74%
Example: A metal zipper forming machine rated at 1,200 meters/hour, running two 8-hour shifts:
1,200 x 16 x 0.74 = 14,208 meters/day actual output
For a new production line, use 65% OEE for the first three months as operators climb the learning curve. Factor this into your customer delivery commitments.
4. Investment Planning: Budget by Production Scale
300-800 m/day
$25,000-$60,000
1,500-4,000 m/day
$80,000-$180,000
8,000-20,000 m/day
$250,000-$500,000+
Budget allocation rule: 60% machines + 15% installation & commissioning + 10% operator training + 10% first-year spares + 5% contingency. A $100,000 machine budget needs a $165,000 total project budget.
5. Quality Control Integration: Build It Into the Line
Do not treat QC as a post-production afterthought. Integrate inspection stations directly into the production flow:
After tooth forming: +/-0.03mm tolerance on tooth pitch. Use automated optical inspection (AOI) for high-speed lines.
After assembly: test 1 in every 500 zippers. #5 zipper should withstand 60N+ lateral pull force per ISO 1421 standards.
Sample test: 10,000 open-close cycles without failure. Metal zippers should achieve 20,000+ cycles for industrial applications.
6. Automation & Smart Factory Readiness
When specifying machines for a new production line, prioritize equipment that supports IoT integration — even if you do not plan to implement it immediately. Key smart-ready features to look for:
- PLC with Ethernet/IP or Modbus TCP — enables centralized production monitoring
- Cycle counter with digital output — feeds real-time OEE dashboards
- Vibration and temperature sensors — foundation for predictive maintenance
- Remote diagnostics port — allows supplier engineers to troubleshoot without on-site visits
The cost premium for smart-ready machines is typically 5-8%, but the retrofit cost of adding these capabilities later is 3-5x higher. Future-proof your investment.
Key Takeaways for Production Line Planners
Define your zipper type mix first — metal, nylon, and plastic lines require fundamentally different equipment.
Choose a layout (U/I/L-shaped) based on volume, product diversity, and floor space — not aesthetics.
Use 74% OEE for capacity planning on established lines, 65% for new lines during ramp-up.
Budget 40% above machine cost for installation, training, spares, and contingencies.
Insist on smart-ready PLCs and sensors — the 5-8% premium pays for itself in the first year of predictive maintenance.
Integrate QC stations into the production flow, not as a post-process gate. Early defect detection saves material and labor.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| Factory quality system | ISO 9001-style management with QC gates | Continuous | Documented procedures for each process |
| Incoming material | Yarn, wire, pellets, chemicals certificate | Every batch | Material traceability to supplier batch |
| In-process control | Process checkpoints per line | Per shift | Parameters recorded and signed |
| Final inspection | Pull force, slider, appearance, AQL | Per lot | AQL 2.5 sampling; records kept for claims |
| Testing equipment | Pull-force, cycling, salt spray, color fastness | Calibrated | Calibration schedule and records |
| Staff assessment | Skill matrix and first-pass yield per operator | Weekly | Training plan tied to defect data |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Raw material & warehouse | 15% | Yarn, wire, pellets and chemicals with FIFO storage |
| Production zones | 55% | One flow per product line; separate dyeing/plating/painting zones |
| QC & lab | 10% | Pull-force, cycling, salt spray and color fastness equipment |
| Packing & finished goods | 15% | Dust-free packing and storage |
| Utilities & treatment | 5% | Air, cooling water, wastewater and exhaust |
| Planning reference | — | Small 200–400 m²/150–250 kW; medium 600–1,000 m²/300–500 kW |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Line operators | Machine operation and process checks | 1–2 weeks per station | Output/shift; defect rate; stop time |
| Technicians | Mechanical, electrical and mold maintenance | 2–4 weeks + on-site | MTTR; preventive maintenance compliance |
| Process engineer | Parameter setting, problem solving, training | Project-based | First-pass yield; complaint rate |
| QC inspectors | Inspection, testing, AQL sampling | 1–2 weeks | Missed-defect rate; report accuracy |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Capacity mismatch after start-up | Line designed without real product mix | Define sizes and mix first; start one line, stabilize, then expand |
| Color contamination between materials | Different fibers dyed in same machine | Separate dyeing by material; acid dyes for nylon, disperse for polyester, reactive for cotton |
| Wastewater/environment approval delays | Treatment planned too late | Plan dyeing/plating/painting permits before line design |
| Power instability | No power plan before installation | Confirm local voltage/frequency and total kW; add stabilizers if needed |
| Operator quality varies | No training or assessment system | Use skill matrix, weekly defect review and first-pass-yield targets |
| Machine downtime high | No spare parts stock | Keep critical wear parts in stock; QLQ supplies spares with long-term support |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Factory Planning Data
Reference values from QLQ new-factory quick tables and real customer projects. Confirm with your line supplier before specification.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| Small factory reference | 10,000–20,000 pcs/day: USD 80k–150k equipment; 200–400 m²; 150–250 kW; 15–35 staff | Under-budgeting utilities or staff = slow start-up and quality swings |
| Medium factory reference | 30,000–50,000 pcs/day: USD 150k–300k equipment; 600–1,000 m²; 300–500 kW; 30–90 staff | Scope creep on product mix raises both area and power needs |
| First-line rule | Start with one complete line for one product type | Mixed lines at start = training gaps and higher defect rates |
| Stabilization period | 3–6 months before adding capacity | Expanding too early multiplies problems before they are solved |
| Voltage options | 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz, 480V/60Hz | Confirm before order; wrong voltage costs installation time |
| On-site support | 1–2 engineers for 7–15 days; longer support by arrangement | First factories benefit most from on-site commissioning and training |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Complete equipment line | Front-end, finishing and surface treatment machines for nylon, metal and plastic zippers |
| Molds & tooling | Slider, teeth and stop molds with 0.02 mm precision and long-life steel |
| Materials & consumables | Chemicals, lacquer, polishing media, films, wires and spare parts with long-term supply |
| Full-process capability | From raw material through weaving, forming, finishing, electroplating and painting - one responsible supplier |
| Turnkey services | Layout design, installation, commissioning, operator/technician training and remote support |
| Proven delivery | 10,000 m² self-owned plant, 35 senior engineers, export to 60+ countries |
Frequently Asked Questions
Where should a new zipper factory start?
Start with a clear product plan: product type, target daily output, workshop size, power supply and whether you have technical staff. QLQ prepares a customized machine list, layout and quotation from these answers.
How much investment does a new factory need?
A small factory at 10,000–20,000 pieces/day is around USD 80,000–150,000 for equipment; a medium factory at 30,000–50,000 pieces/day is around USD 150,000–300,000. This excludes building, utilities and working capital.
Should I buy one line at a time or the full line?
For a first factory, buy one complete line for one product type, run it 3–6 months, train the team, then expand. QLQ supports phased investment.
Can QLQ send engineers to install and train?
Yes. Online support is free; on-site commissioning with 1–2 engineers for 7–15 days is recommended for new factories, and longer technical support can be arranged. The customer covers visa, flights, hotel and meals.
Do zipper factories need environmental approval?
Usually yes when dyeing, plating or painting is in-house. Small factories can outsource plating/dyeing; medium factories should plan wastewater treatment and exhaust with the line design.
Can machines be customized for our voltage and frequency?
Yes. Common options include 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz and 480V/60Hz three-phase. Confirm the local standard and it is included in the PI.
What support is available after delivery?
Installation and commissioning, operator/technician training, spare parts and consumables supply, process optimization and remote troubleshooting form a closed support loop.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Zipper Production Workshop
Whether you produce nylon, metal or plastic zippers, every profitable factory starts with the same planning data: quality standards, space, people, power and output targets. The table below summarizes realistic planning figures for a typical mid-size multi-type zipper workshop.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | ISO 9001 quality system with BS 3084 / ASTM D2061 / QB/T 2171 testing; incoming material inspection; in-process QC at each station; pull-force, slider cycling and color-fastness tests per batch; final AQL 2.5 sampling before packing. |
| Workshop Area Required | 1,000–2,500 m² for a complete multi-type line (nylon and plastic, or metal), plus 200–400 m² warehouse; ceiling height above 4.5 m; separate dyeing, plating (if any), assembly and packing zones. |
| Workforce Needed | 20–50 workers across two shifts: line operators, 2–4 machine technicians, 2–4 QC inspectors and 1–2 production managers; more staff are required when plating is done in-house. |
| Power Supply | 150–400 kW connected load depending on line type; 380V/50Hz three-phase (or 220V/480V 60Hz); compressed air at 0.6–0.8 MPa; water supply for dyeing, cooling or plating. |
| Daily Production Capacity | Finished zippers: 8,000–20,000 pcs/day across sizes #3–#10; chain production: 5,000–15,000 m/day, depending on the number and type of lines. |
| Estimated Gross Margin | 18%–30% on finished zippers; in-house dyeing, finishing and a balanced product mix support the higher end of the range. |
| Typical Investment Range | $150,000–350,000 for a complete mid-size multi-type line, excluding building construction and local environmental permits. |
| Typical Payback Period | 18–30 months at 70% average utilization with steady order volume. |
Quality First
- Test pull force and slider cycling on every batch
- Run incoming material inspection on all yarns and parts
- Keep in-process QC records at every handover
- Use AQL 2.5 sampling before shipping
Workshop & Power
- Plan production, warehouse and utility zones clearly
- Provide stable three-phase power with surge protection
- Ensure ventilation for dyeing, heating or plating areas
- Keep a dust-free packing and storage zone
People & Profit
- Train operators and technicians before production starts
- Assign QC inspectors to each major process
- Gross margin target: 18%–30%
- Payback target: 18–30 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Planning a new zipper factory or upgrading an existing workshop? Contact QLQ Machinery for a complete line design, equipment list and quotation matched to your target capacity.