How to Make Plastic Open-end Finished Zipper with Pin Box (Solution 2)
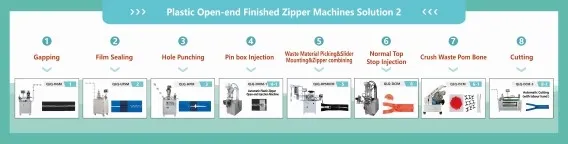
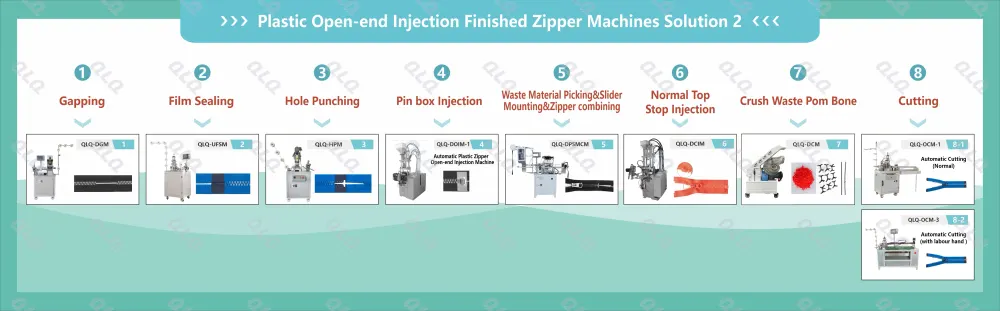
1-Process Flow Chart
2-Process Video
3-Process Details
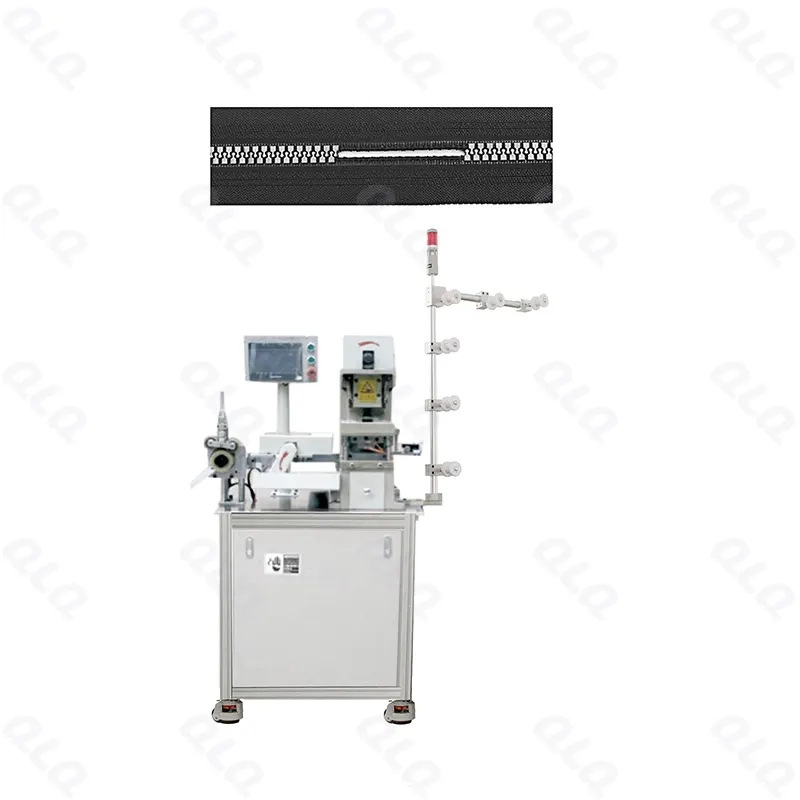
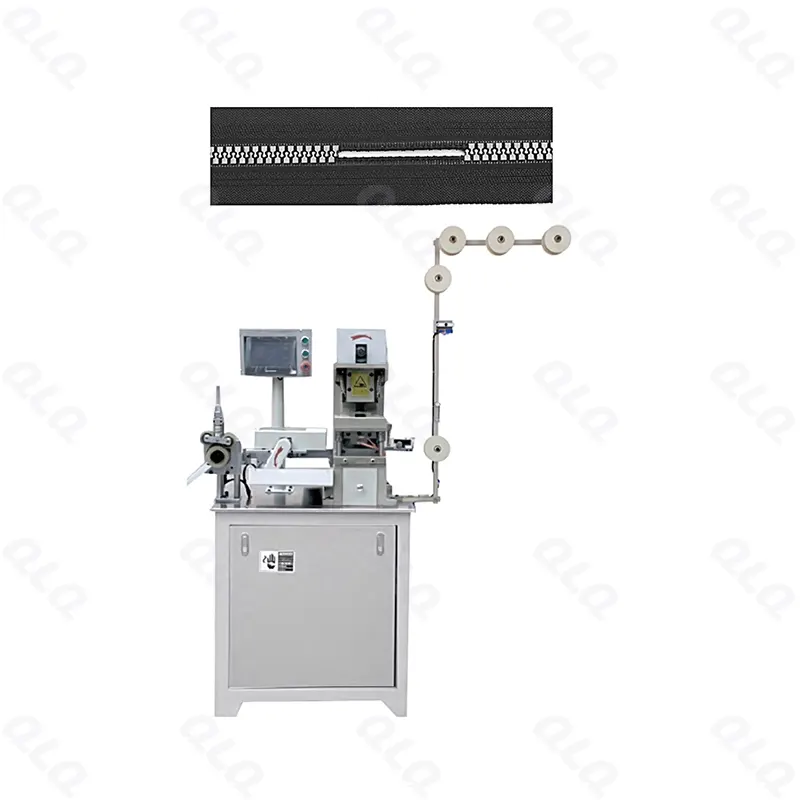
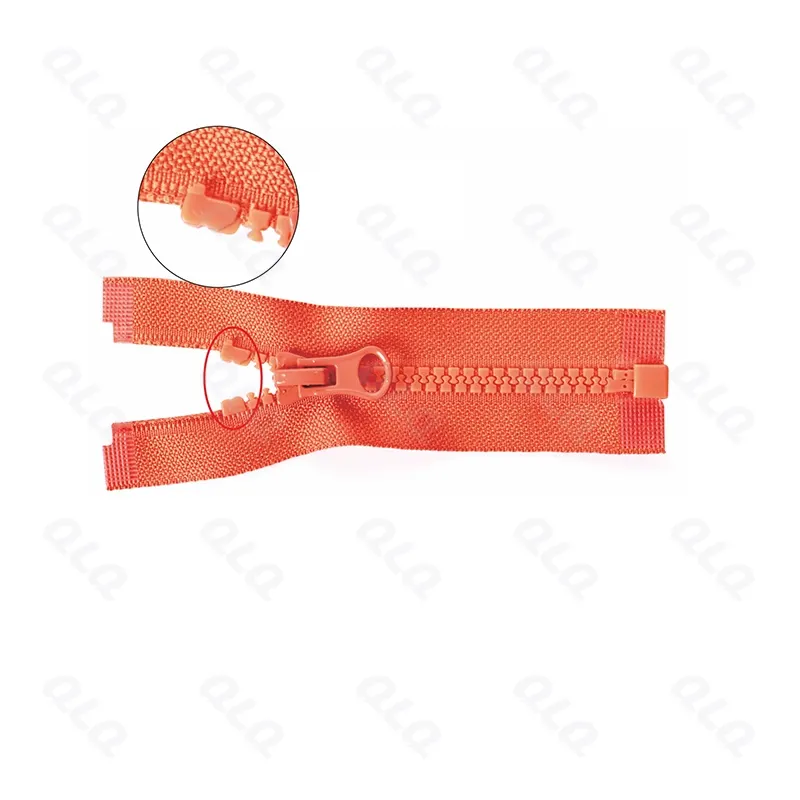
Step 1: Gapping
Machine: QLQ-DGM Material: Plastic Long-chain Zipper
Please click the following photos for more details.
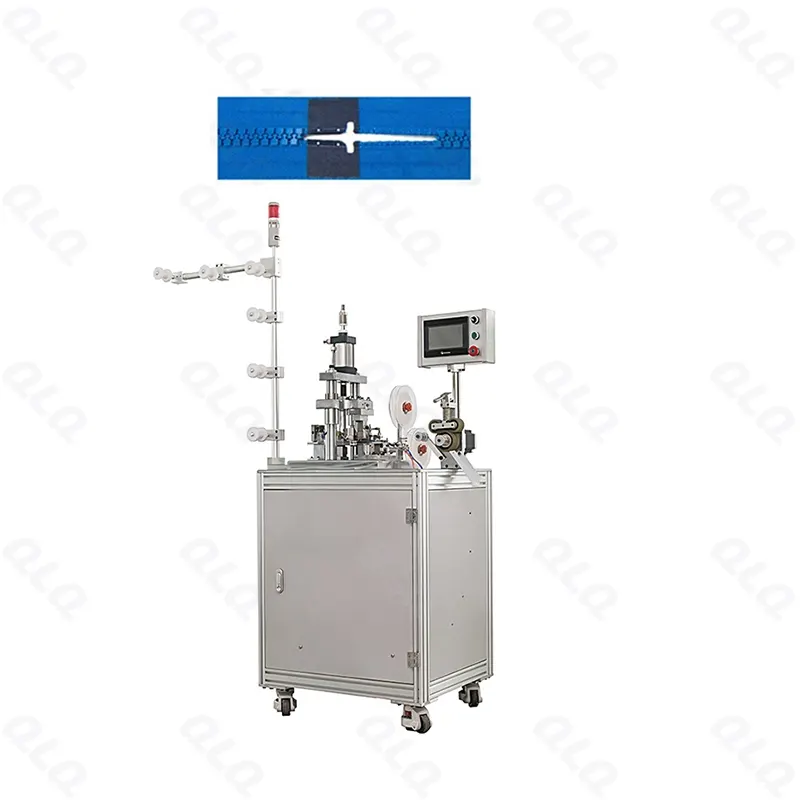
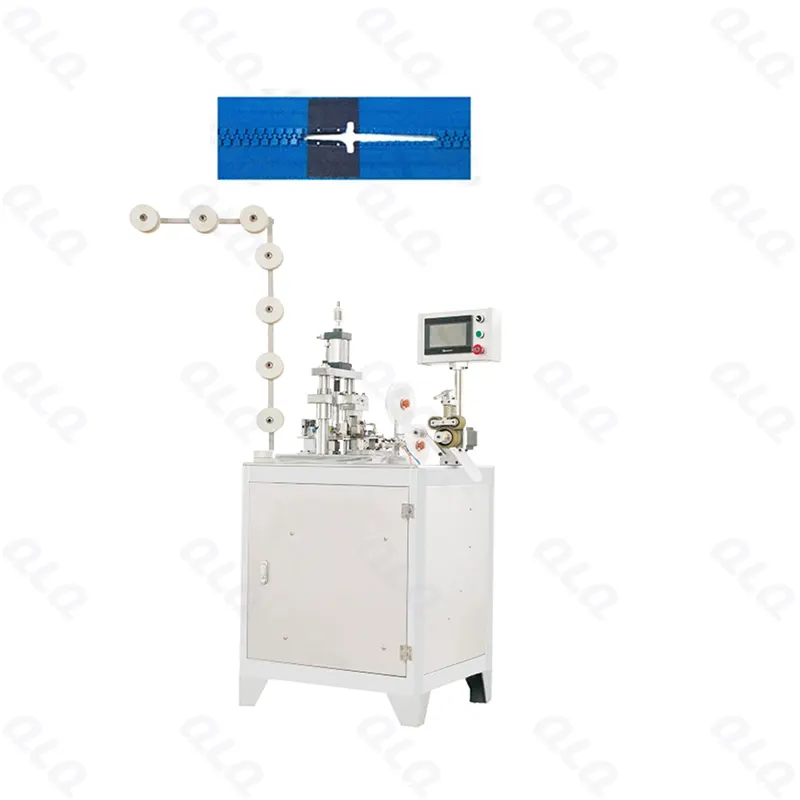
Step 2: Film Sealing
Machine: QLQ-UFSM Material: Transparent Film, Semi-Transparent Film, Fabric Film, Tafeta Film
Please click the following photos for more details.
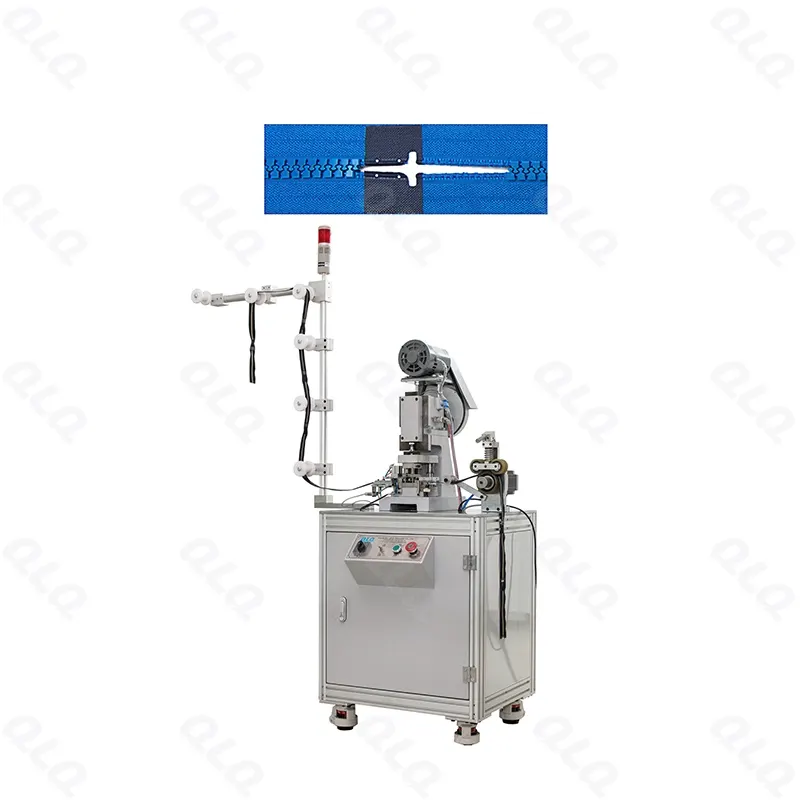
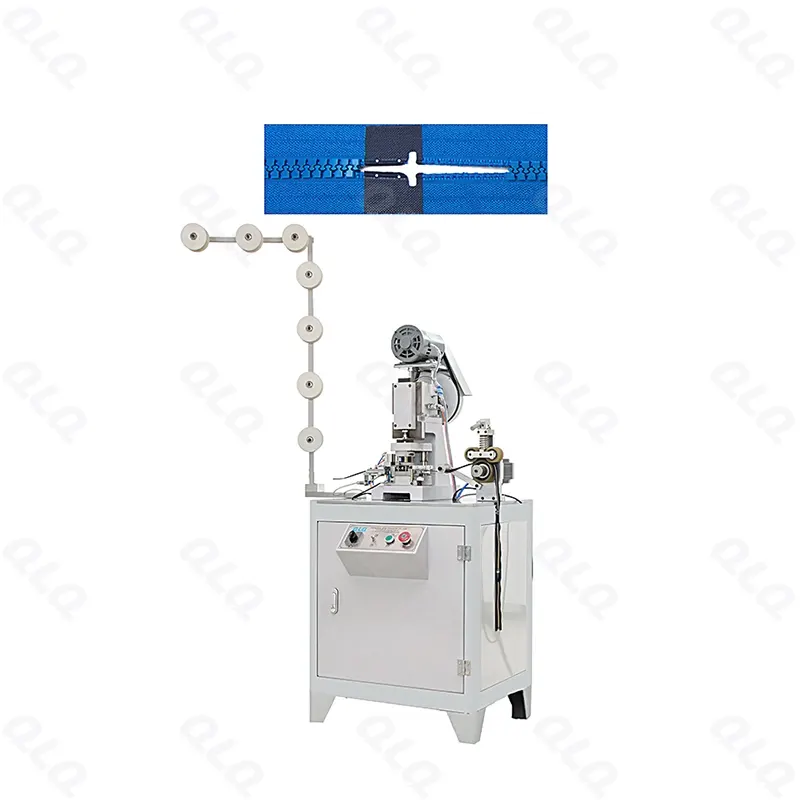
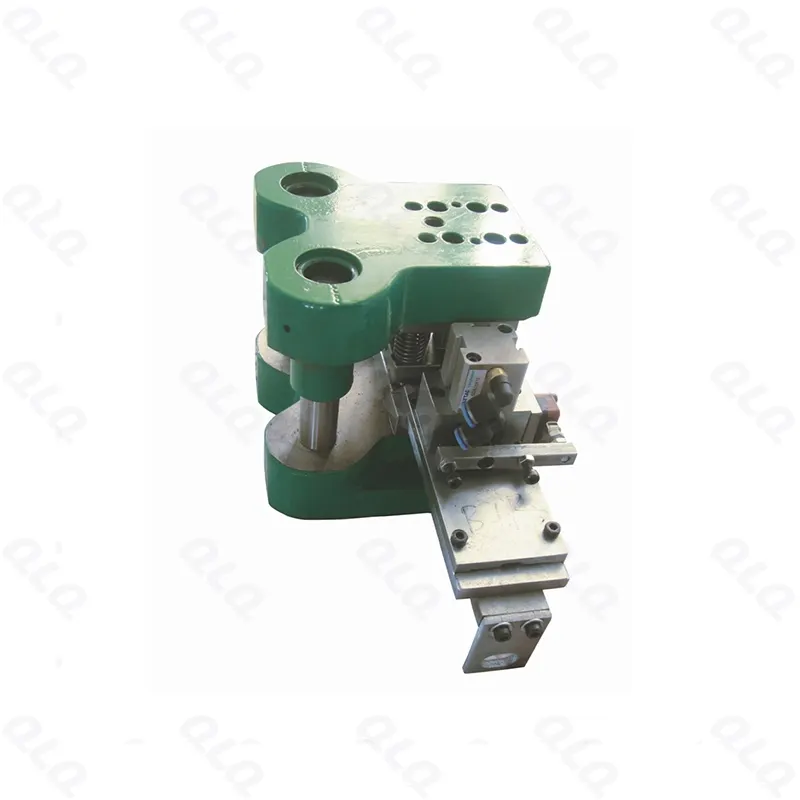
Step 3: Hole Punching
Machine: QLQ-HPM and Hole Punching Mould
Please click the following photos for more details.
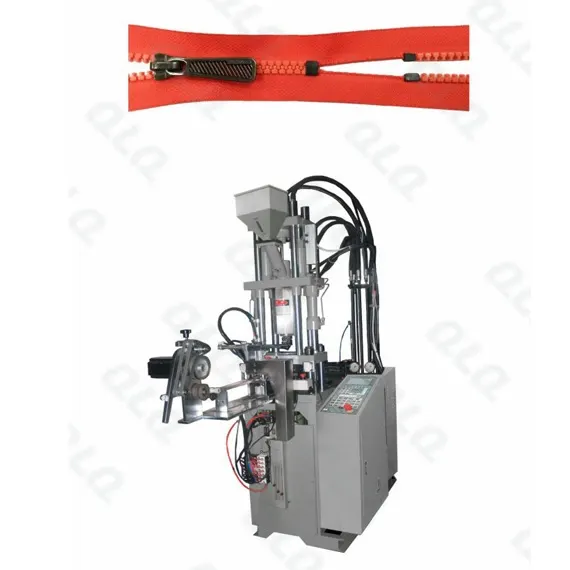
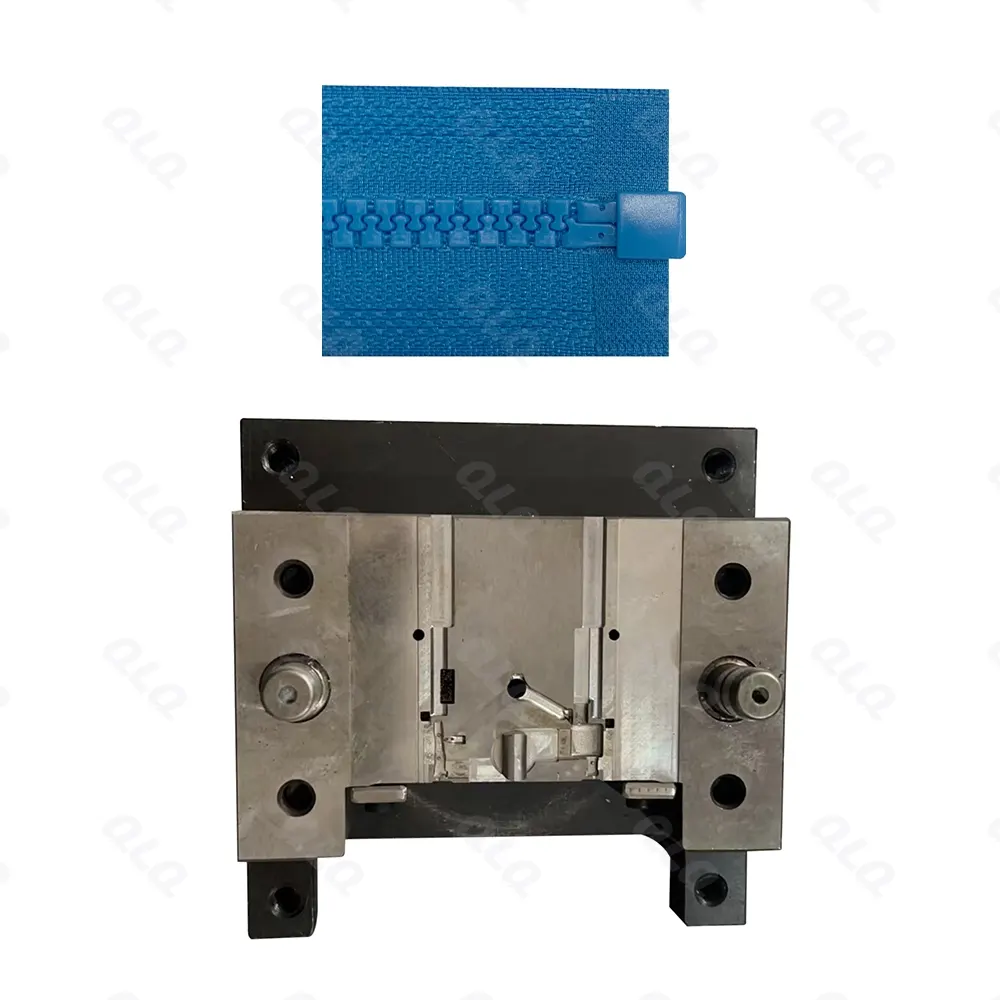
Step 4: Pin Box with Side Insert Top Stop Injection
Machine: QLQ-DOIM-1 Material: POM Material
Please click the following photos for more details.
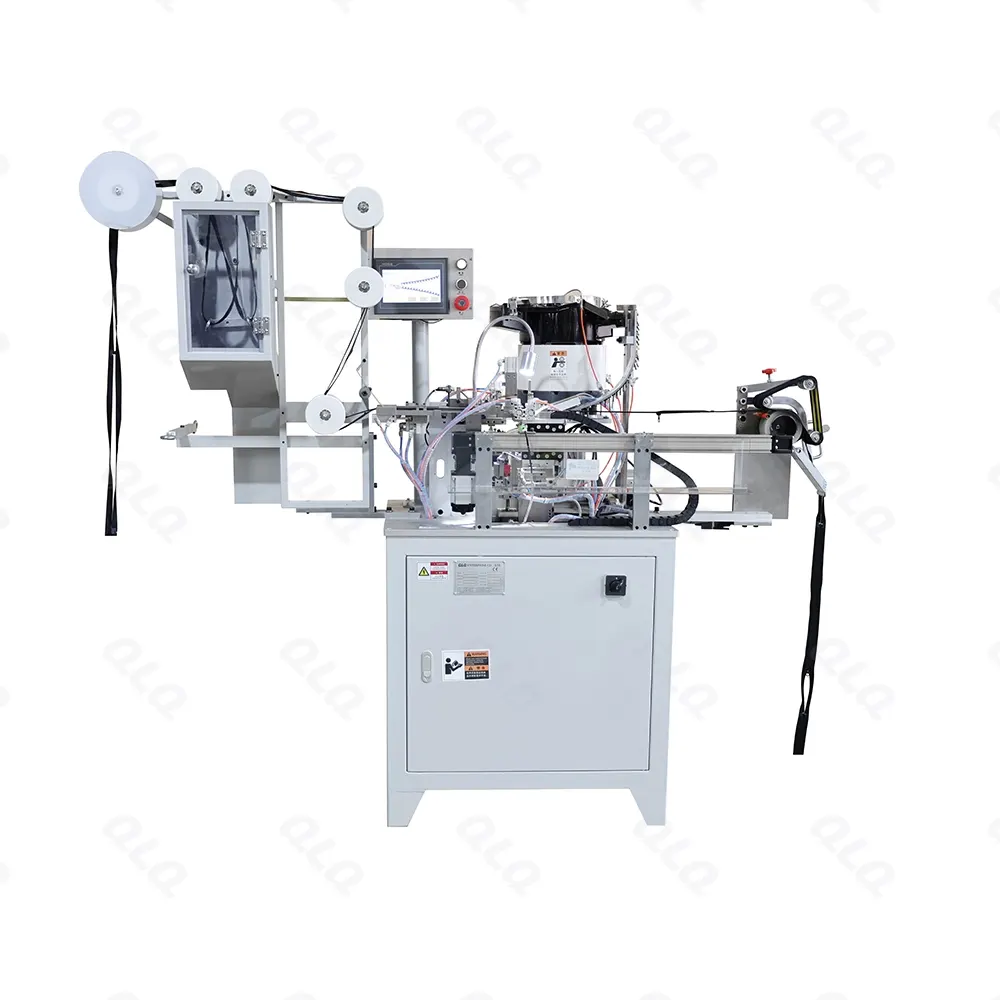
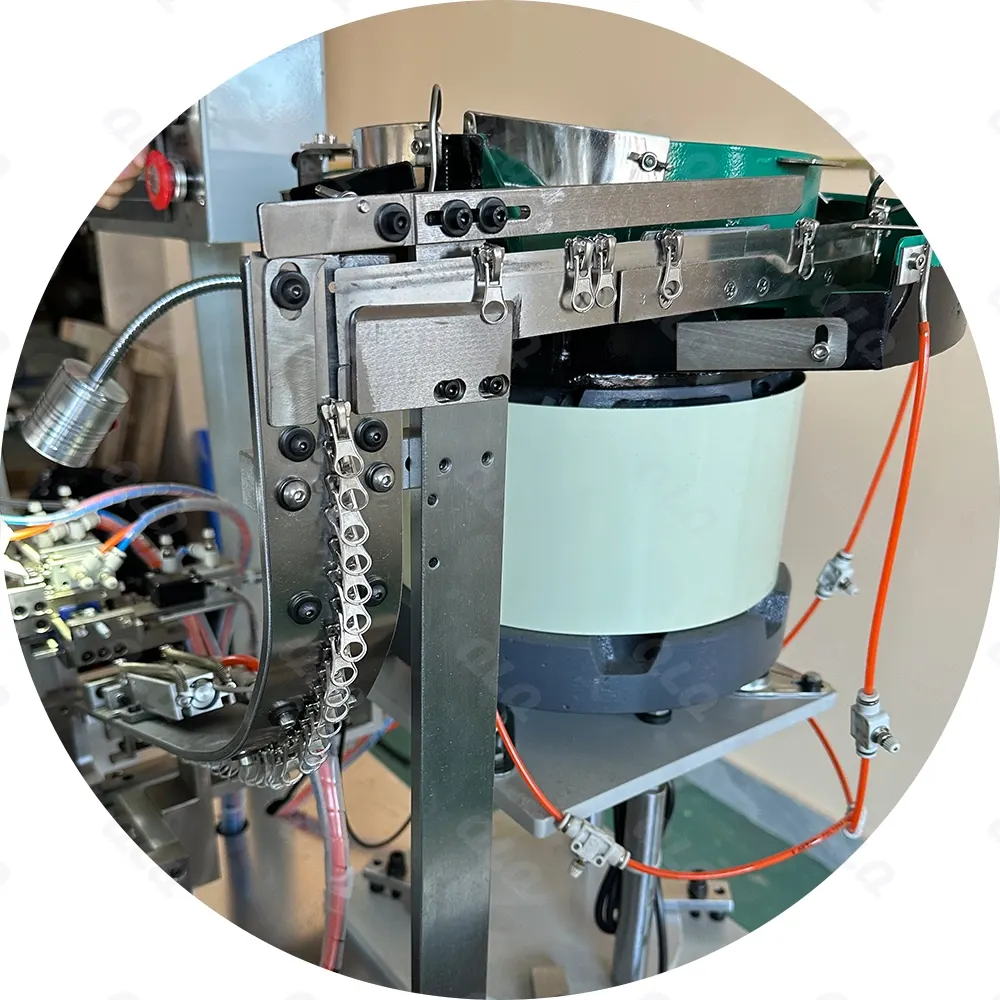
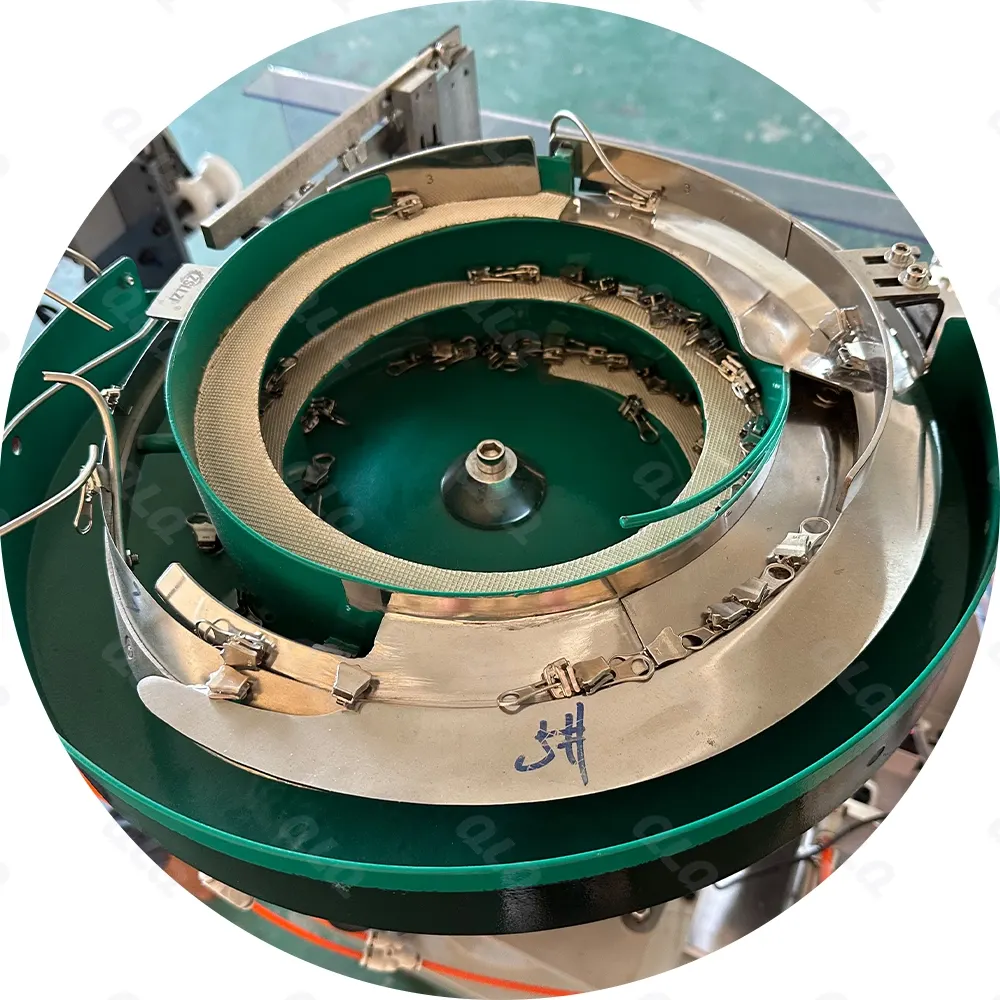
Step 5: Waste Material Picking Slider Mounting & Zipper Combining
Machine: QLQ-DPSMCM
Please click the following photos for more details.
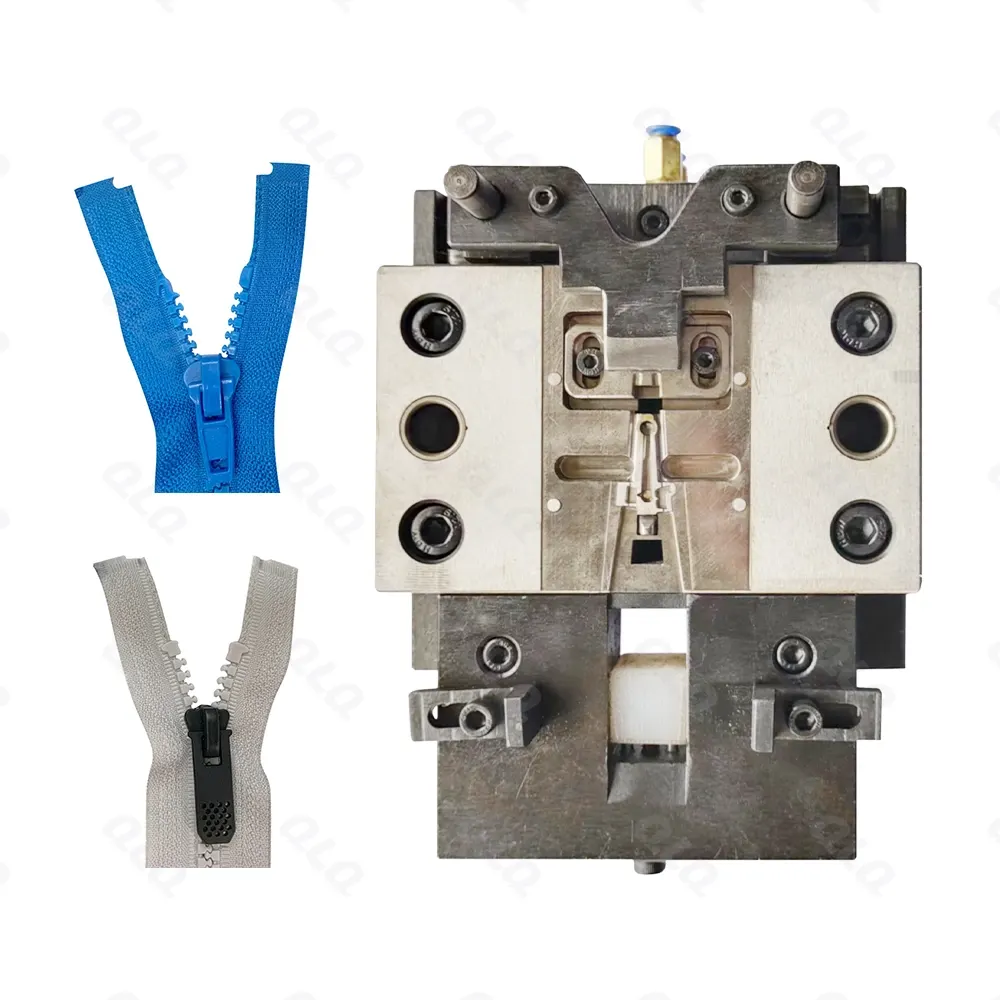
Step 6: Normal Top Stop Injection
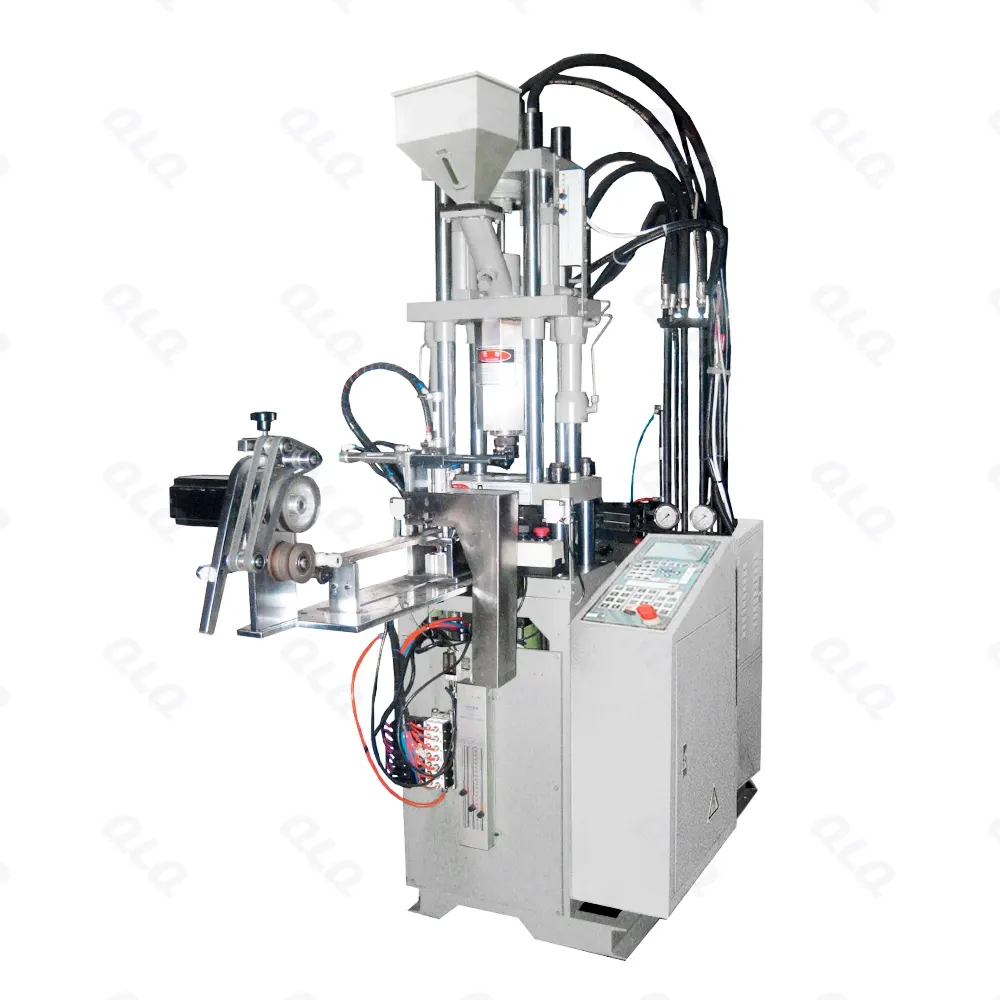
Machine: QLQ-DCIM
Please click the following photos for more details.
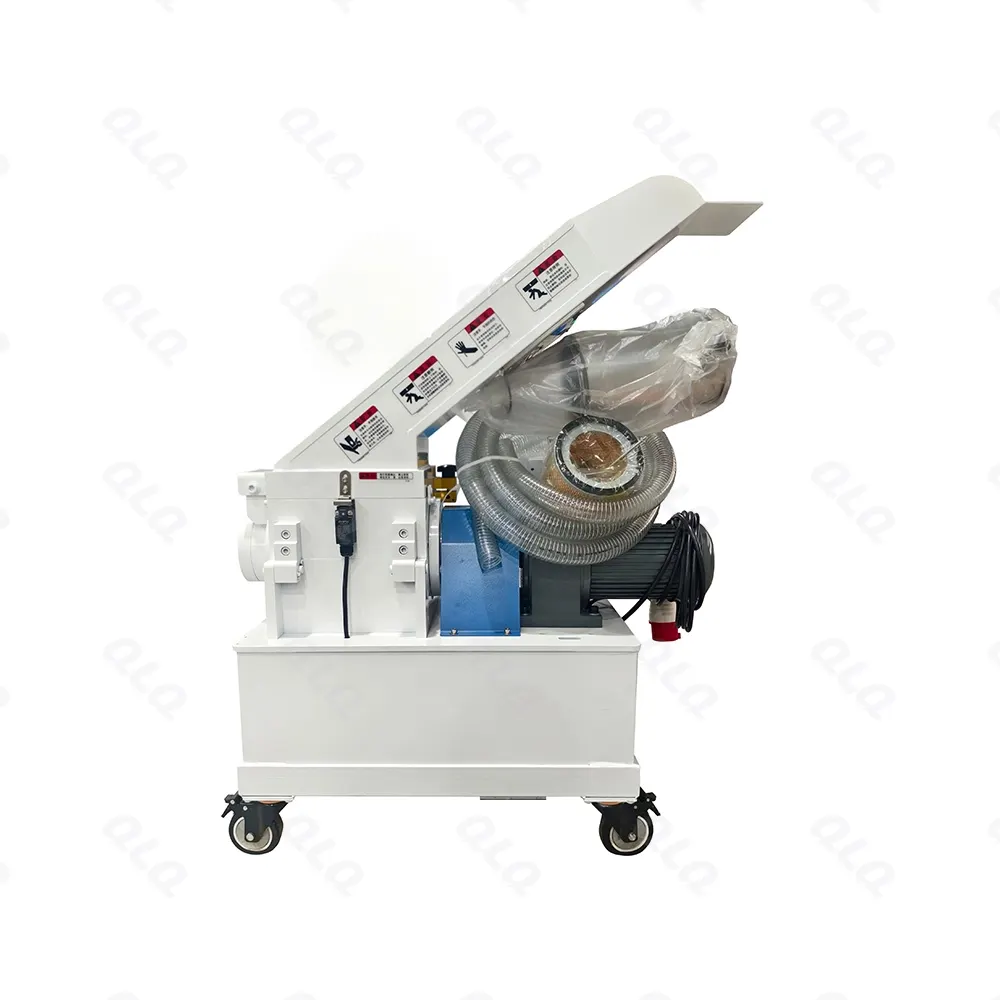
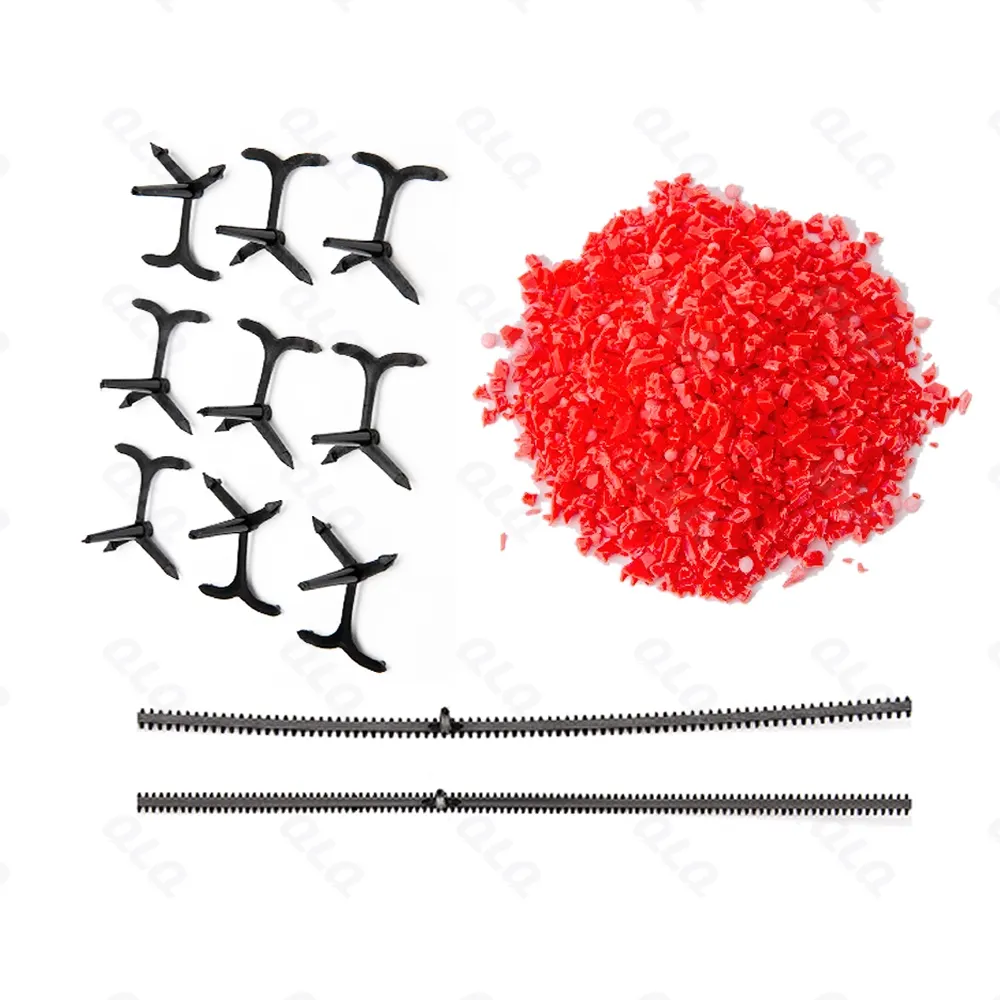
Step 7: POM Crushing
Machine: QLQ-DCM
Please click the following photos for more details.
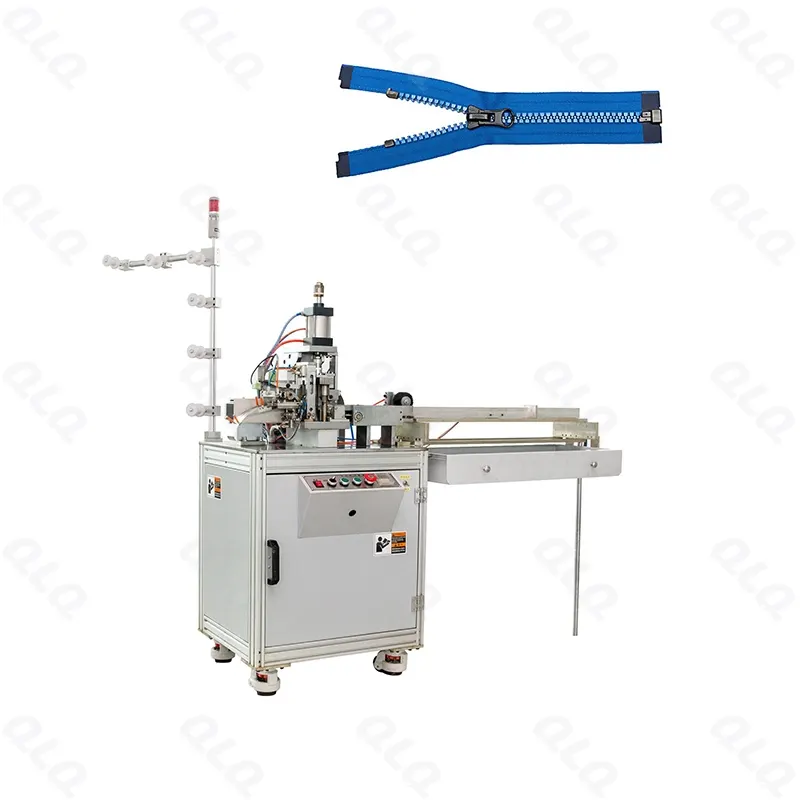
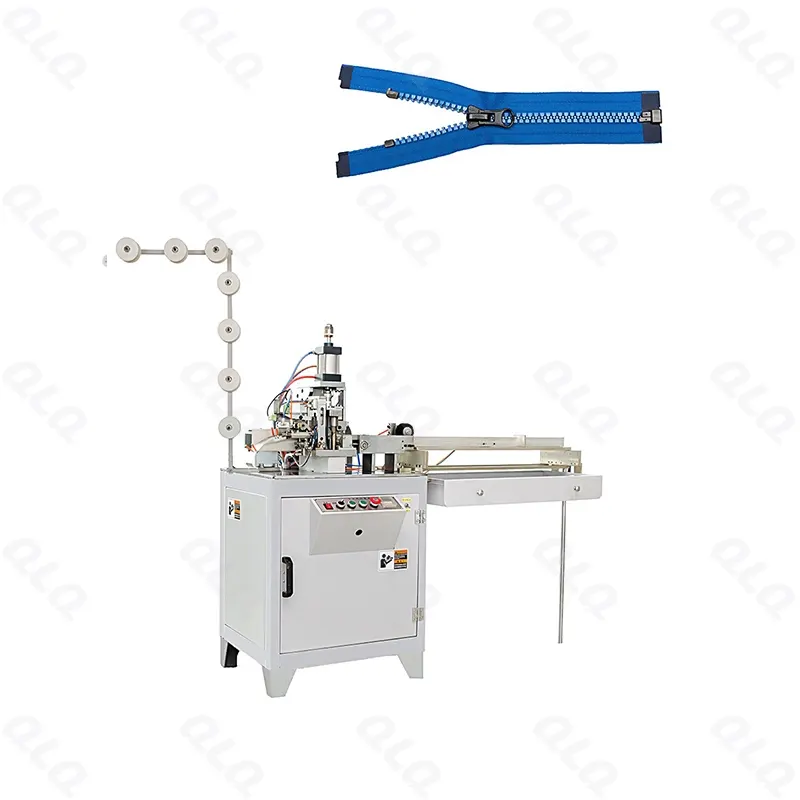
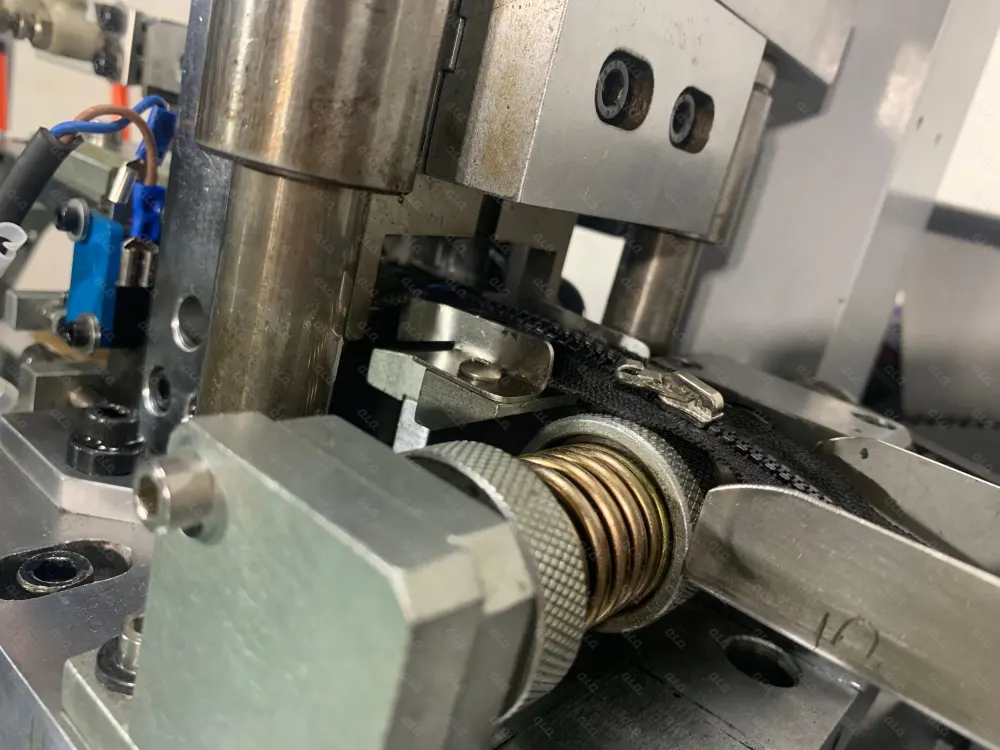
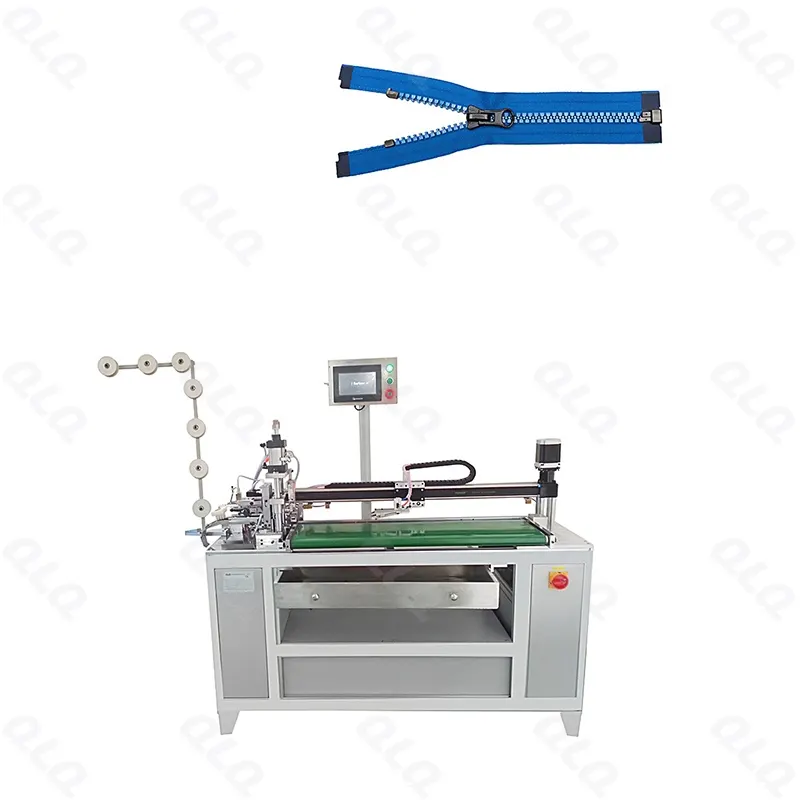
Step 8: Cutting
Machine: QLQ-OCM-1
Please click the following photos for more details.
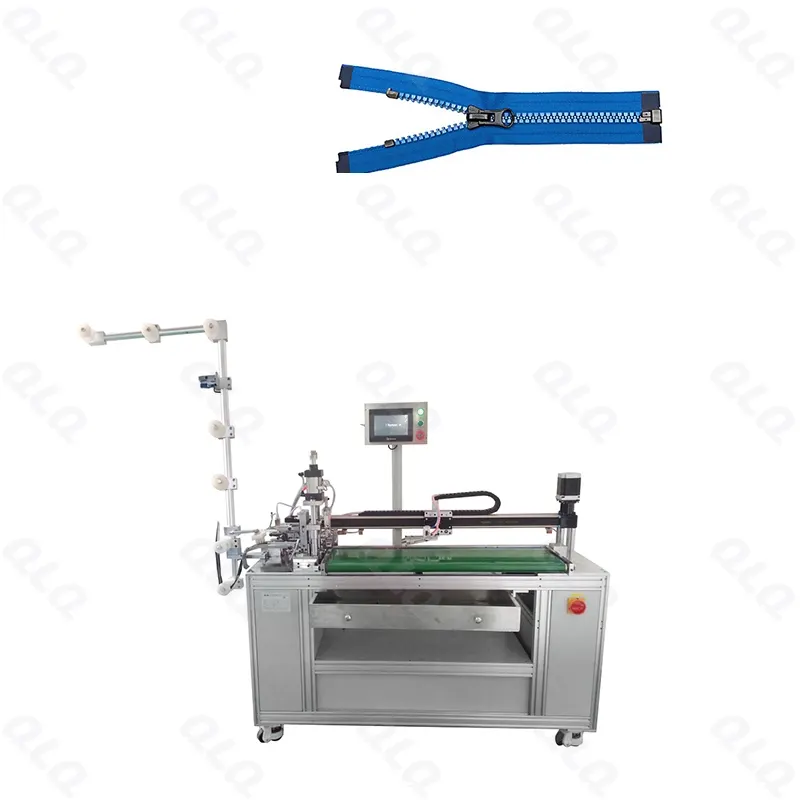
Machine: QLQ-OCM-3
Please click the following photos for more details.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| POM material receiving | Batch certificate, moisture check | Every batch | Dry pellets before injection; consistent supplier |
| Injection forming | Tooth dimensions, pitch, flash | Every 30 min | No flash, no short shot; pitch within tolerance |
| Cooling & annealing | Cooling time and temperature | Per mold | Complete cooling before handling to prevent warp |
| Gapping & finishing | Gap position and stop fit | Every 2 h | Clean gap; stop fits without force |
| Color & surface | Shade vs masterbatch standard | Per batch | ΔE ≤ 1.0; no streaks or dull areas |
| Finished zipper | Pull force, slider fit, AQL | Per lot | Per BS 3084; AQL 2.5 |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Material & drying | 15% | POM storage with drying hoppers; dust-controlled |
| Injection area | 35% | Injection machines with cooling water loop; mold rack nearby |
| Finishing | 30% | Gapping, stops, slider mounting, cutting, inspection |
| Packing & QC | 20% | Testing, packing and finished-goods storage |
| Utilities | — | Air compressor, cooling water, granule crusher for sprue recycling |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Injection operators | Mold change, temperature control, shot inspection | 1–2 weeks | First-pass yield; flash/short-shot rate; mold change time |
| Mold technician | Mold maintenance, cavity cleaning, insert change | 2–4 weeks | Mold downtime; preventive maintenance compliance |
| Color controller | Masterbatch ratio, shade checking | 1 week | Color reject rate; batch consistency |
| QC inspector | Pitch, pull force, slider fit, AQL | 1–2 weeks | Missed-defect rate; report accuracy |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Color inconsistent between batches | POM not dried, temperature drift, masterbatch ratio wrong, cooling time short | Use drying hopper; stabilize temperature zones; control masterbatch ratio; keep supplier consistent |
| Flash or short shot on teeth | Clamp force, injection pressure, mold venting, material moisture | Check clamp and pressure; clean vents; dry material; verify mold fit |
| Tooth warp after cooling | Cooling time too short, mold temperature uneven | Extend cooling; balance mold temperature; check annealing step |
| Slider does not fit plastic chain | Tooth profile or pitch drift, slider mouth mismatch | Verify pitch gauge; check mold wear; match slider to chain sample |
| Mold wears early | Poor cooling design, lack of maintenance, wrong steel | Follow maintenance schedule; clean and lubricate; upgrade inserts |
| 72-hour dimension changes | Shrinkage allowance not applied to moving core | Machine core to final-product size minus shrinkage; confirm drawing before machining |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Plastic Zipper Process Data
Reference values from QLQ project data and standard plastic zipper practice. Confirm final parameters with your line supplier.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| POM drying | Drying hopper before injection; consistent moisture | Wet pellets = steam streaks, flash and brittle teeth; keep drying continuous |
| Injection temperature zones | Stable zones per material grade | Temperature drift = color change and dimension variation between batches |
| Cooling time | Complete cooling per mold before ejection | Short cooling = warp and delayed shrinkage; 72-hour dimension check recommended |
| Mold cavity count | 2-cavity typical; 4-cavity for high volume | More cavities = higher output but longer fill; cooling must be balanced |
| Masterbatch ratio | Consistent ratio per shade | Ratio drift = ΔE shift; record ratio per batch |
| Tooth pitch check | Pitch gauge every 30 min | Pitch drift = slider jamming and pull-force failure; check mold wear first |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Front-end equipment | Plastic zipper injection machines (mono and two-color), tape feeding and cooling |
| Finishing equipment | Gapping, stop injection, slider mounting, cutting and testing machines |
| Molds & tooling | Vislon teeth molds, injection molds and inserts; 0.02 mm precision, H13/SKD61 steel |
| Materials & consumables | POM sourcing guidance, color masterbatch, films and spare parts with long-term supply |
| Surface treatment | Shiny film sealing, lacquer and UV coating equipment for finished chain |
| Services | Layout design, mold plan, installation, training and remote support |
Frequently Asked Questions
Do I need injection machines or dedicated forming machines for plastic zippers?
Plastic/vislon zippers are made by injection molding. You need injection machines, one mold per size and tooth type, tape feeding/cooling, then gapping, stops, slider mounting and cutting machines.
How much does a plastic zipper mold cost and how long does it last?
Mold price depends on size and cavity count; life is typically 100,000–300,000 shots with H13/SKD61 steel and regular maintenance. One mold is dedicated per size, with inserts for left/right variants.
Why is the color different between batches?
Usually POM moisture, injection temperature drift, masterbatch ratio or cooling time. Use a drying hopper, stabilize temperature zones and record the ratio per batch.
What equipment is needed for two-way open-end plastic zippers?
An open-end injection mold with two insert pins, slider mounting that handles two sliders, and box-pin/insert-pin assembly. QLQ supports #5, #8 and #10 two-way open-end sizes.
Can plastic zipper teeth machines also run metal parts?
No. Metal Y-teeth use stamping machines with different dies and materials. Plastic teeth use injection machines with POM and dedicated molds.
Why do finished dimensions change after a few days?
Plastic parts shrink after molding. The mold core must be machined to final-product size minus shrinkage allowance. Confirm the drawing before machining to avoid rework.
What should a new plastic zipper factory test?
At minimum pitch and dimension checks, pull-force tester, slider fit and color comparison. Add washing and fastness testing when supplying garments or brands.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Plastic Zipper Production Workshop
Plastic zipper production is injection-based, so material drying, mold maintenance and stable power are the key planning factors. The table below summarizes realistic planning figures for a typical mid-size plastic zipper line.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | BS 3084 / QB/T 2171 compliance with hourly teeth-dimension and pitch checks; POM material batch records; slider smoothness and pull-force tests on every batch; color consistency checks against retained samples; final AQL 2.5 sampling. |
| Workshop Area Required | 500–1,200 m² production area plus 150–250 m² warehouse; dust-controlled injection zone; separate sealing, lacquering, cutting and packing areas with ventilation. |
| Workforce Needed | 10–22 workers across two shifts: injection and chain operators, finishing-line operators, 1–2 mold technicians, 1–2 QC inspectors and 1 production manager. |
| Power Supply | 100–220 kW connected load; 380V/50Hz three-phase (or 220V/480V 60Hz); compressed air at 0.6–0.8 MPa; cooling water loop for injection machines. |
| Daily Production Capacity | Plastic chain: 8,000–20,000 m/day; finished plastic zippers: 10,000–25,000 pcs/day for sizes #3–#10, depending on mold count and shift pattern. |
| Estimated Gross Margin | 18%–30% on finished plastic zippers; in-house dyeing or lacquering and a larger mold inventory support higher utilization and margin. |
| Typical Investment Range | $100,000–180,000 for a complete mid-size plastic line including injection machines, molds, sealing and cutting equipment. |
| Typical Payback Period | 12–24 months at 70% average utilization with steady order volume. |
Quality First
- Dry POM material before every injection run
- Check teeth dimensions and pitch hourly
- Test slider glide and pull force per batch
- Keep color samples and lot records for traceability
Workshop & Power
- Keep injection area dust-controlled and ventilated
- Provide a stable cooling water loop
- Store molds in a clean, dry rack system
- Use stable three-phase power with surge protection
People & Profit
- Train mold-change and maintenance staff
- Schedule QC checks at every process handover
- Gross margin target: 18%–30%
- Payback target: 12–24 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Planning a plastic zipper plant? Contact QLQ Machinery for a complete line layout, mold recommendation, machine list and quotation based on your target daily output.