How to Make Invisible Closed-end Finished Zipper
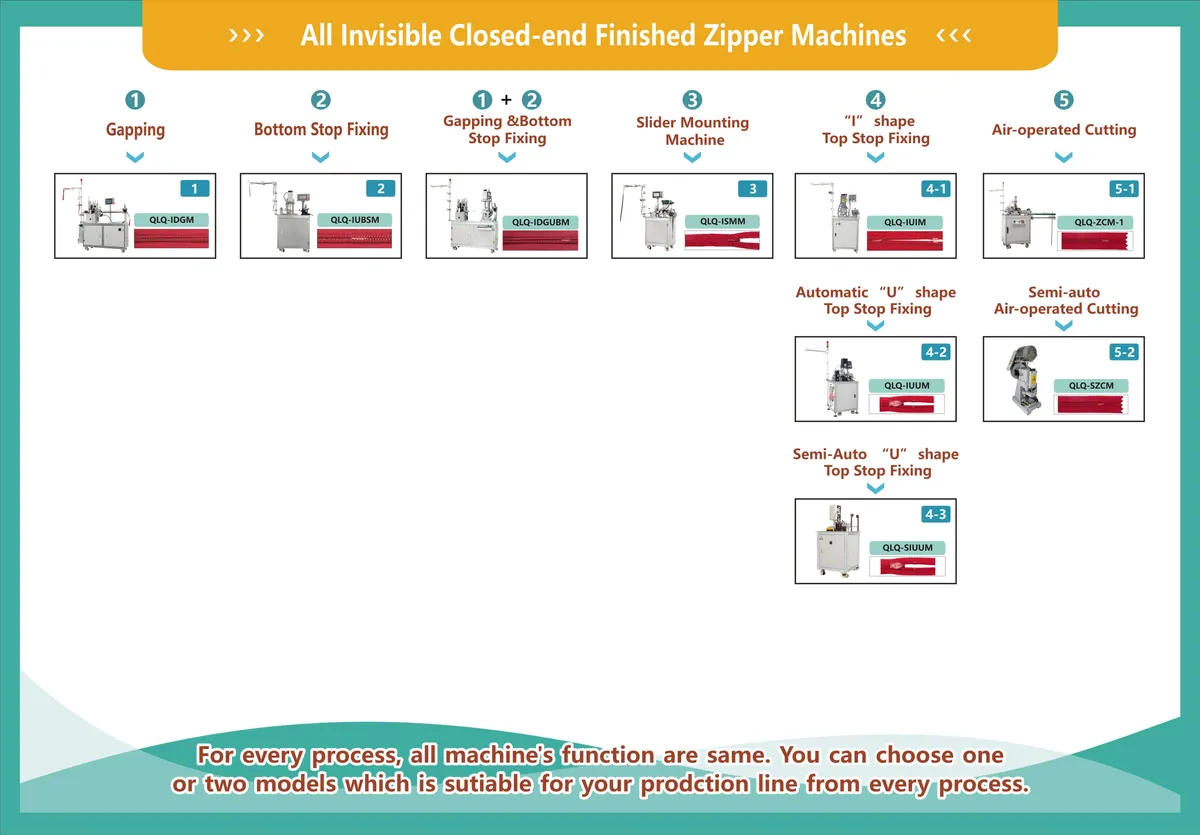
1-Process Chart
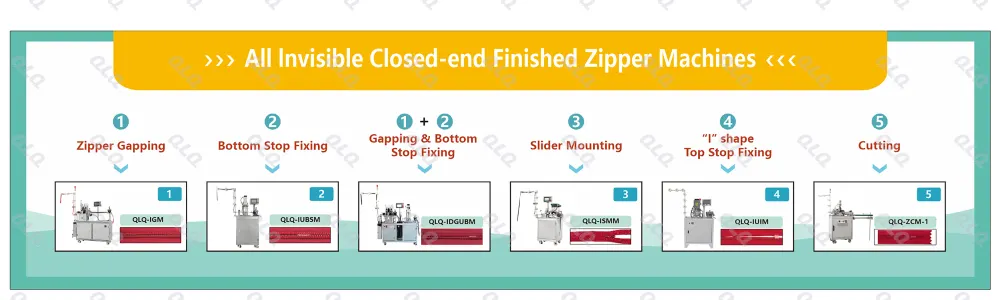
2-Process Video
3-Process Details
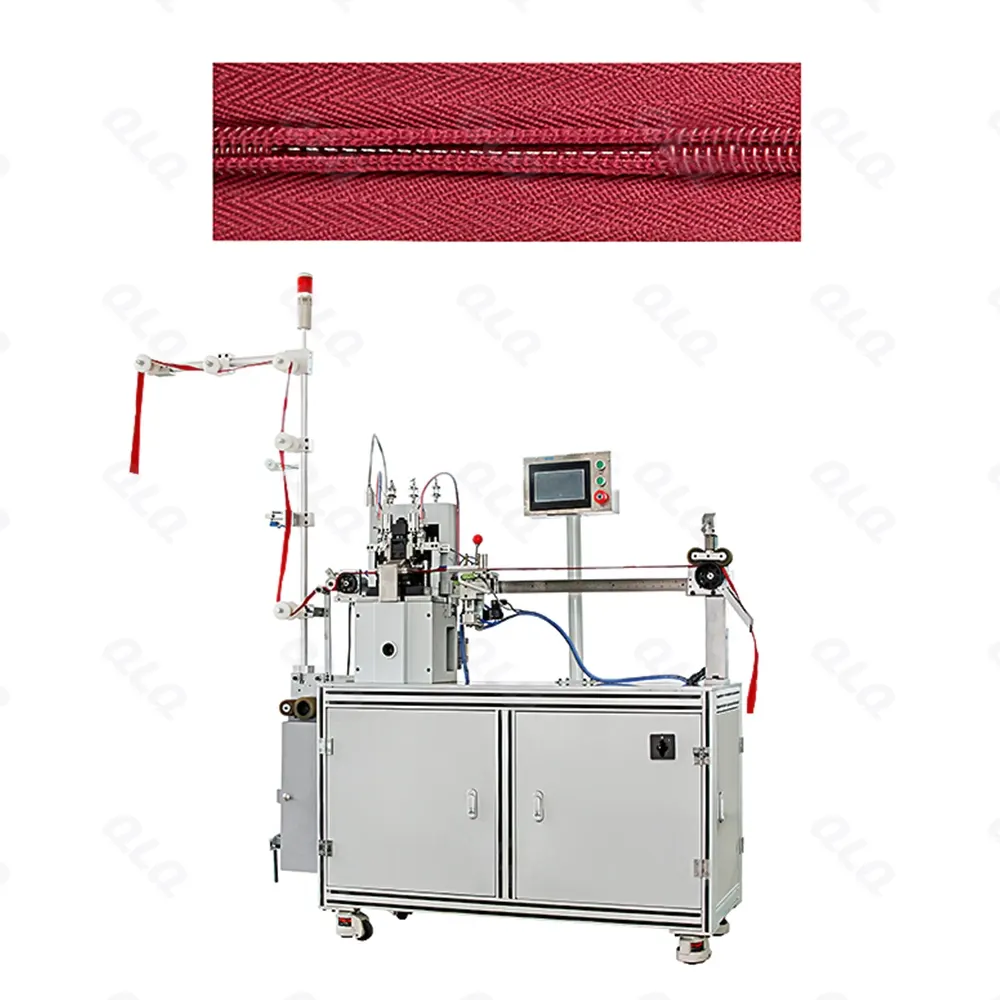
Step 1: Gapping
Machine: QLQ-IGM Material: Invisible Long-chain Zipper
Please click the following photos for more details.
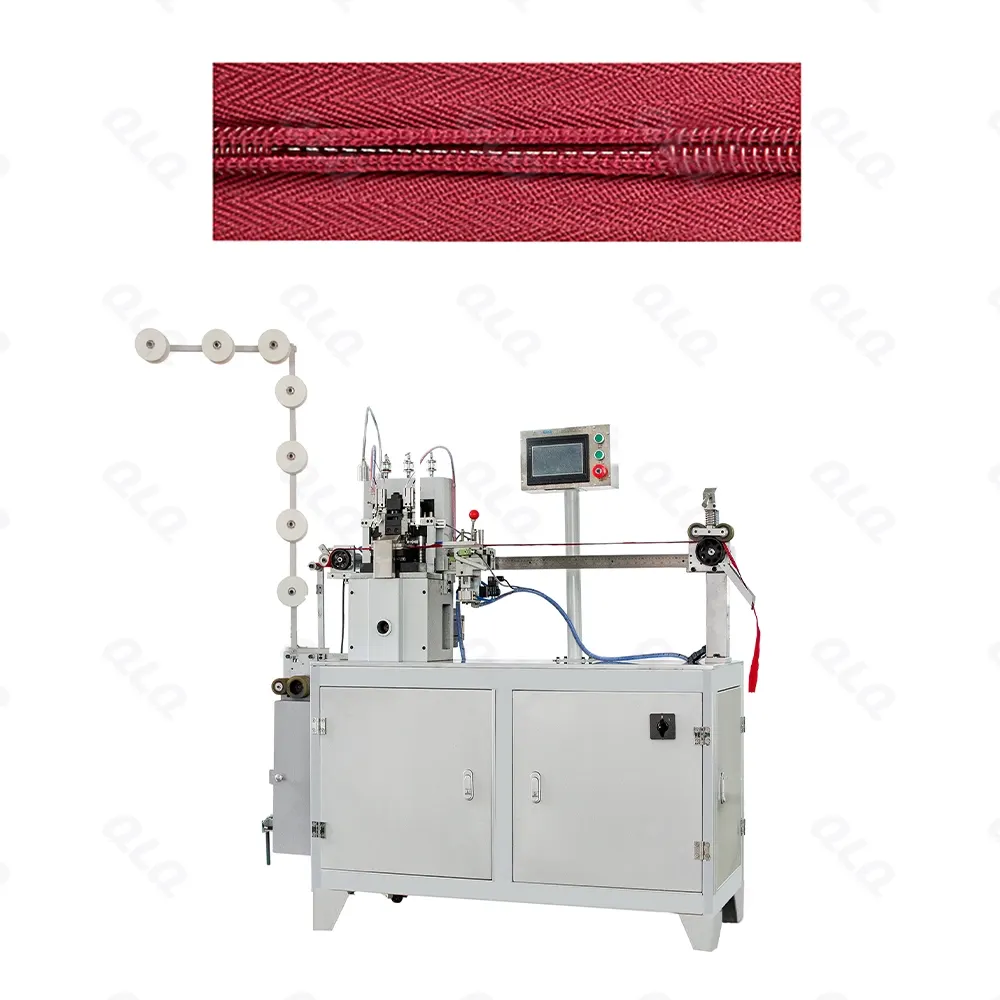
Step 2: Bottom Stop Fixing
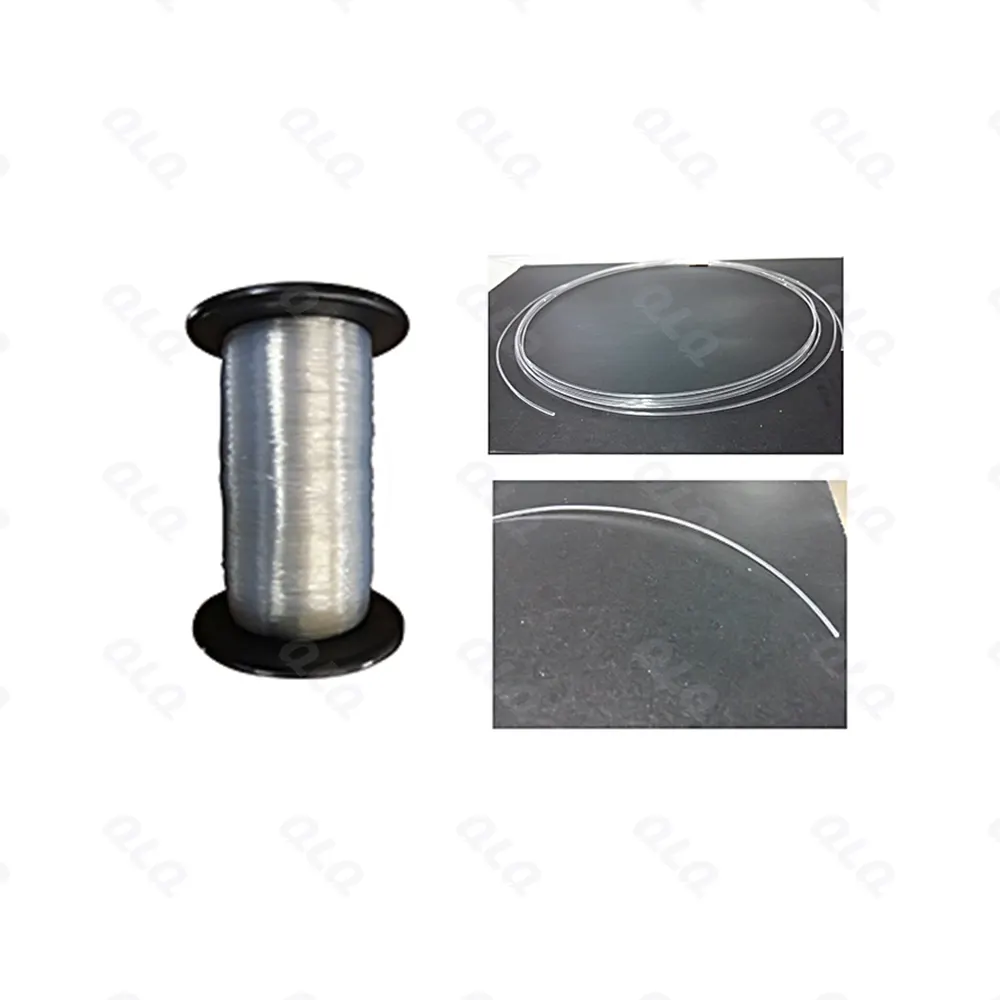
Machine:QLQ-IUBSM Material: Transparent Bottom Stop Wire
Please click the following photos for more details.
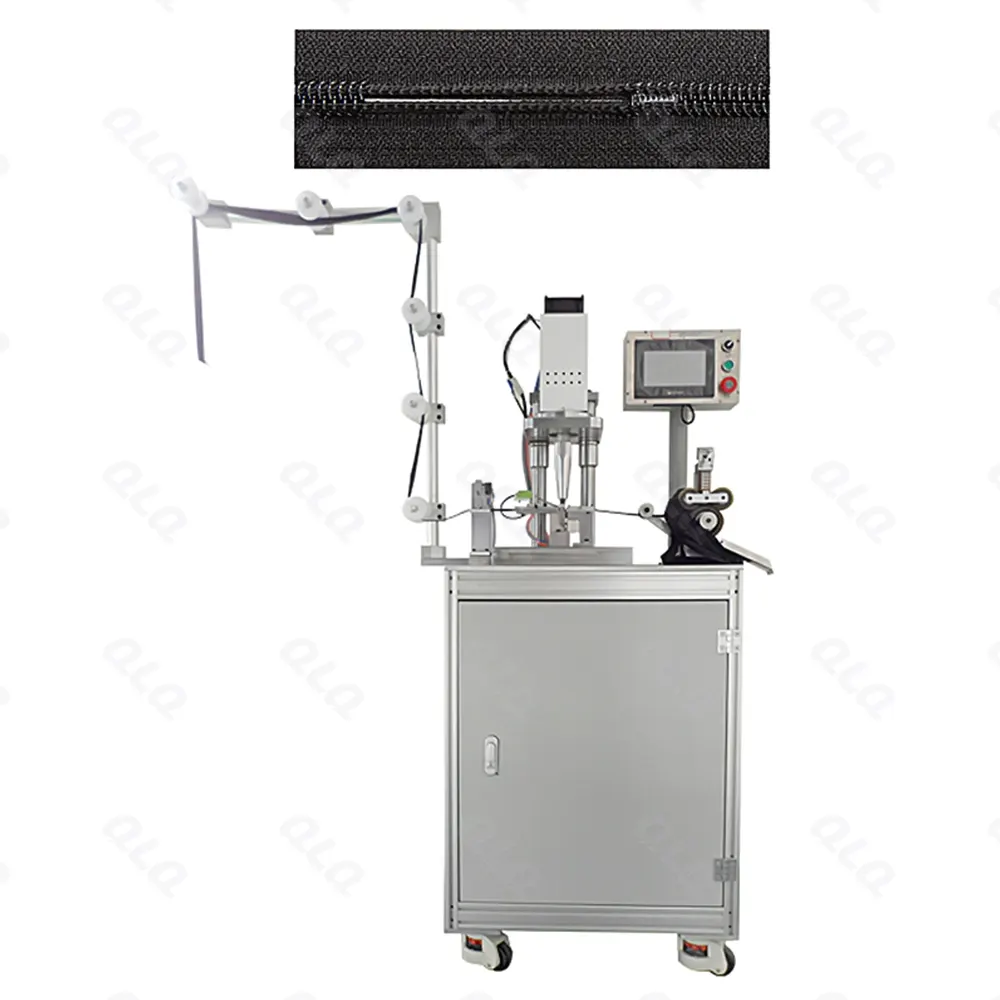
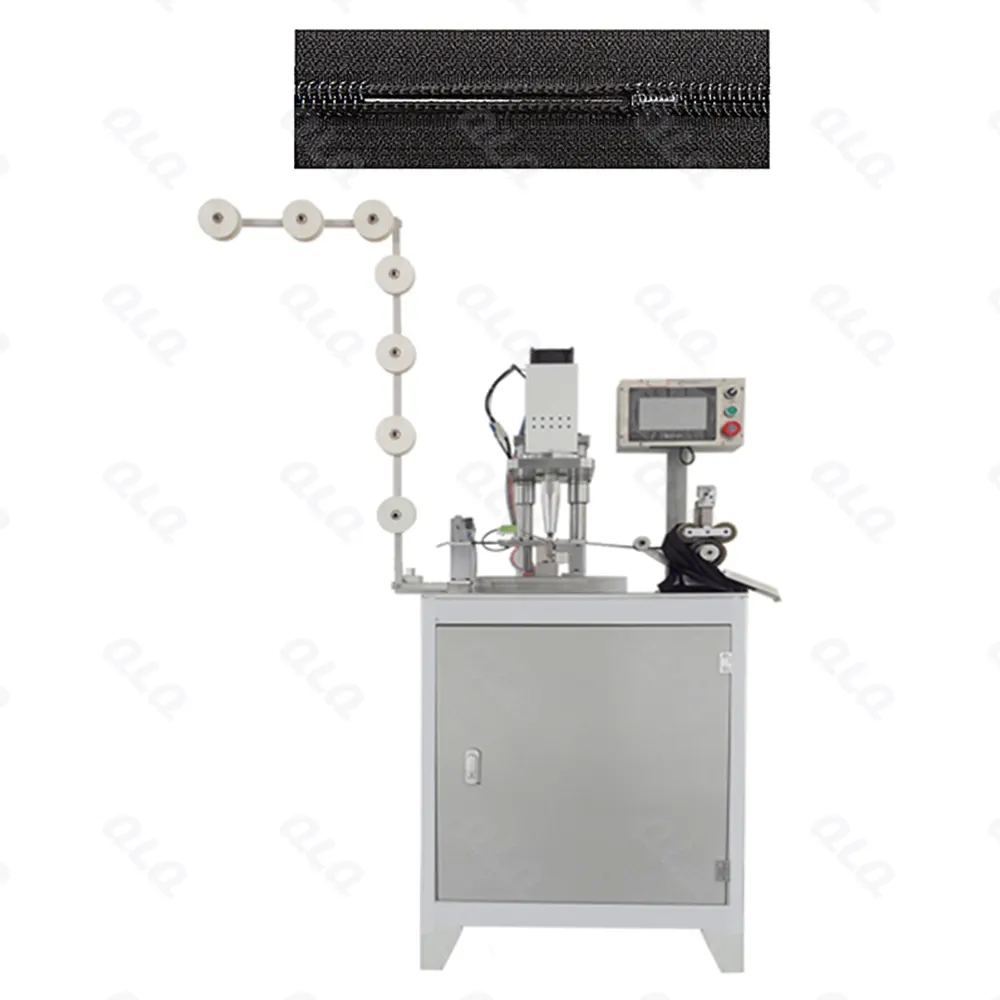
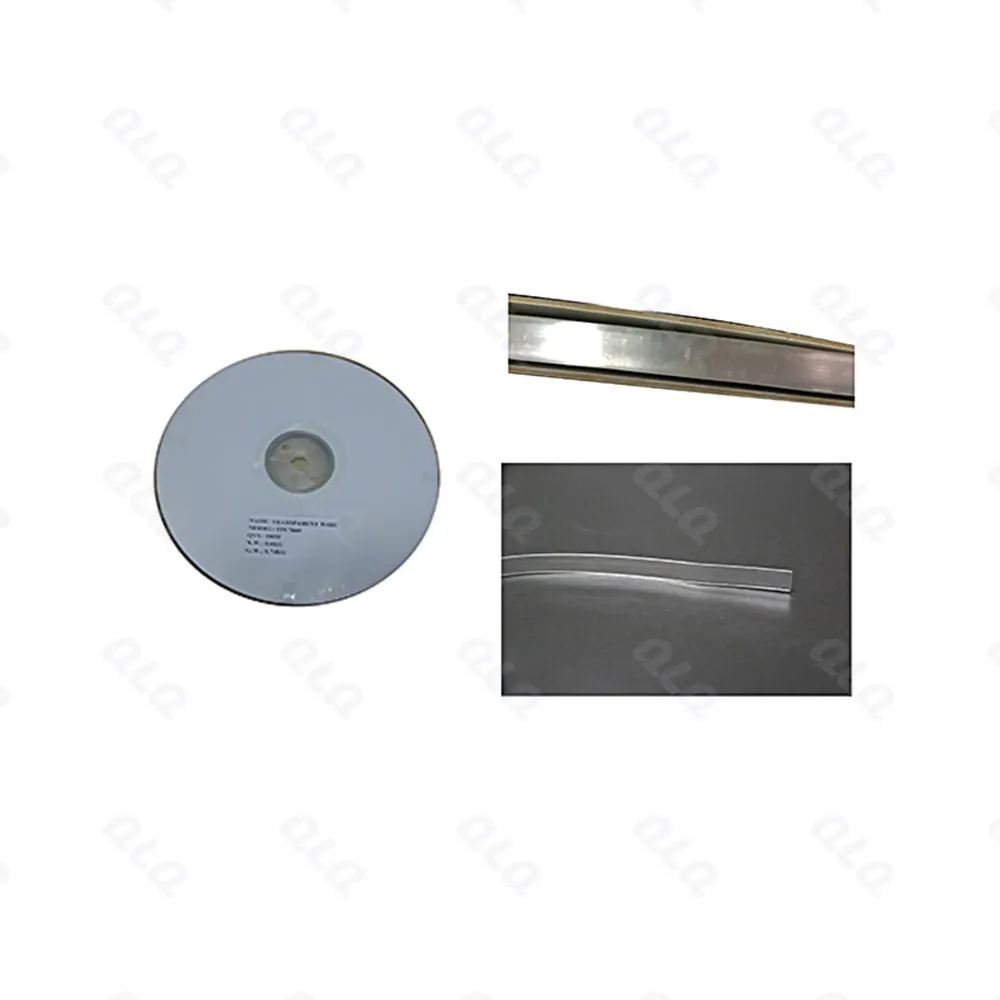
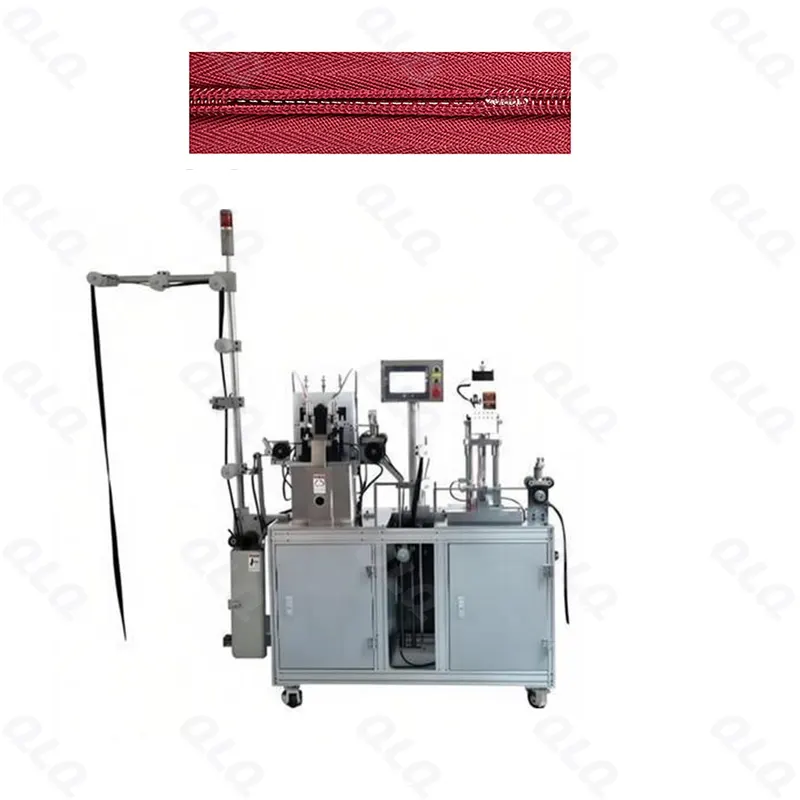
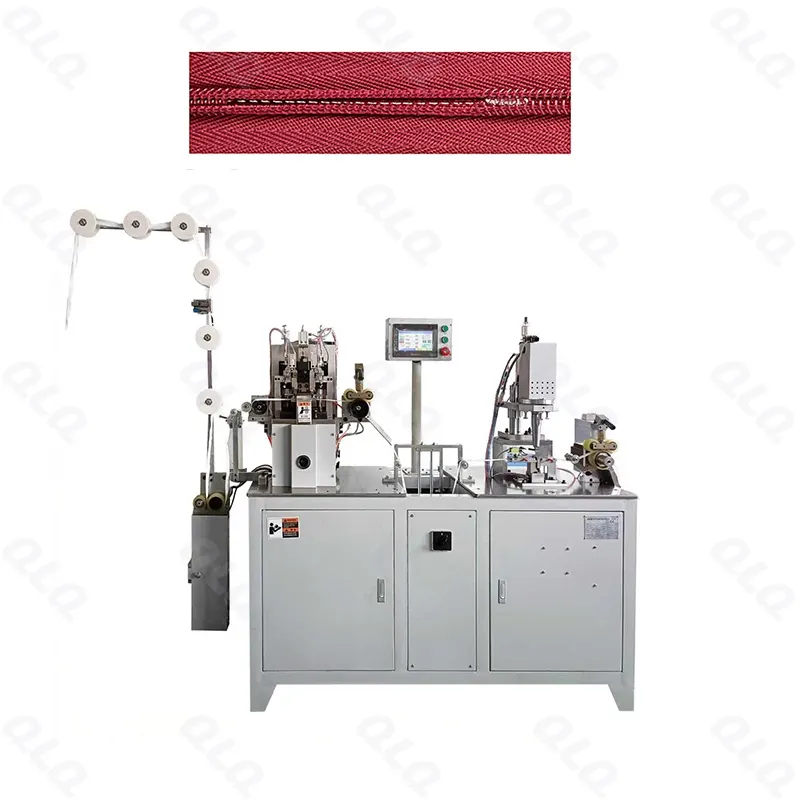
Gapping & Bottom Stop Fixing
Machine: QLQ-IDGUBM
Please click the following photos for more details.
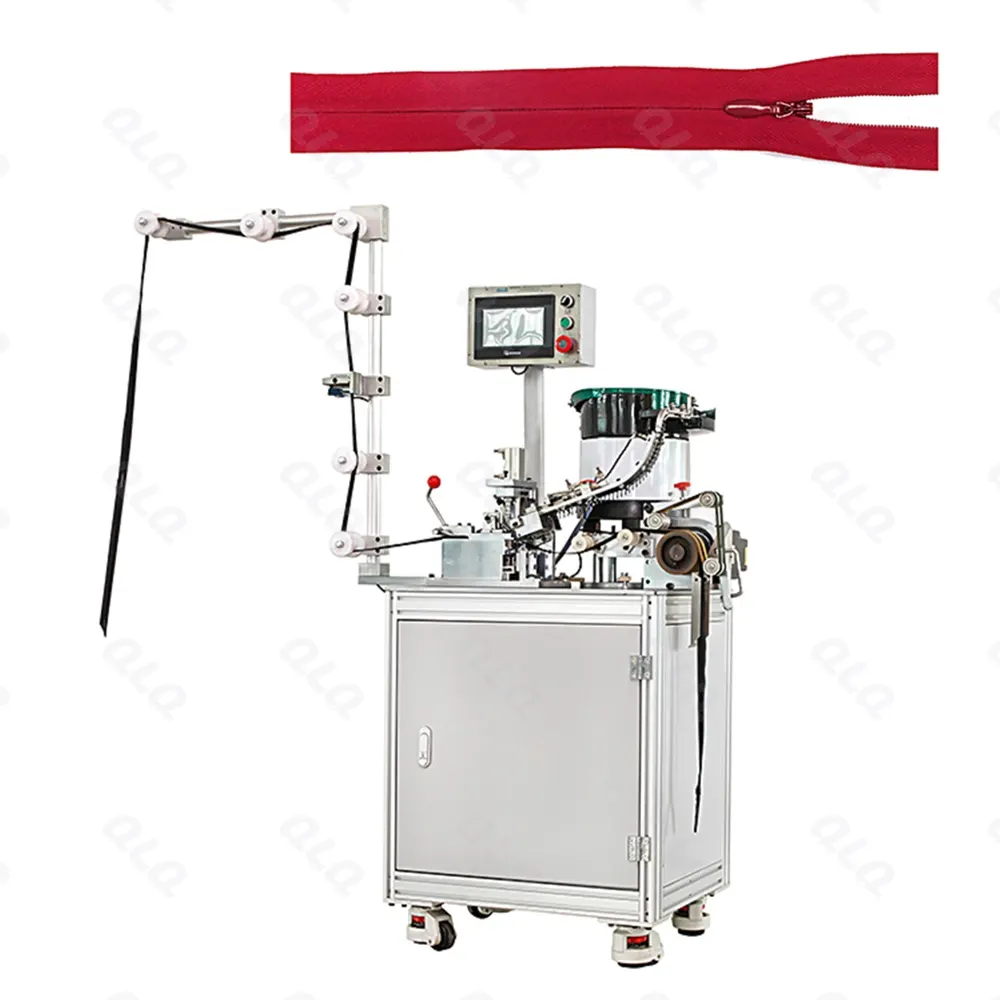
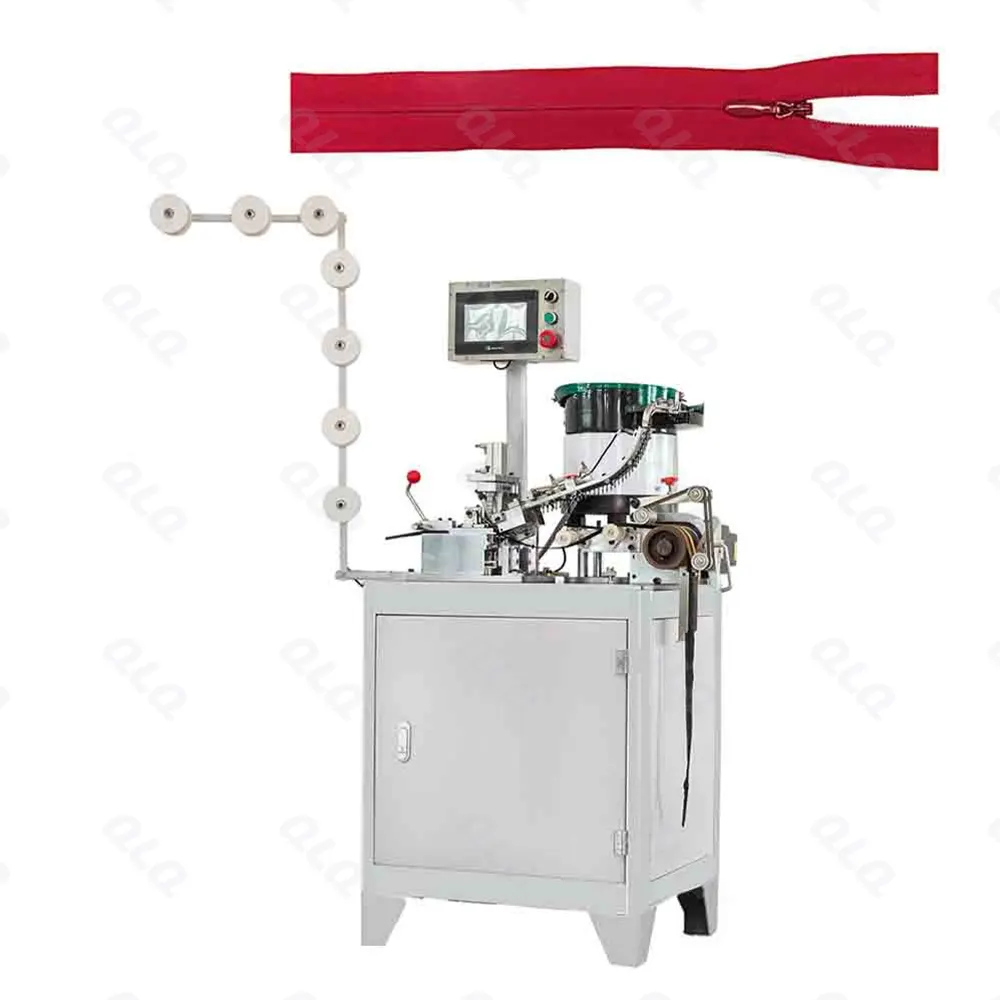
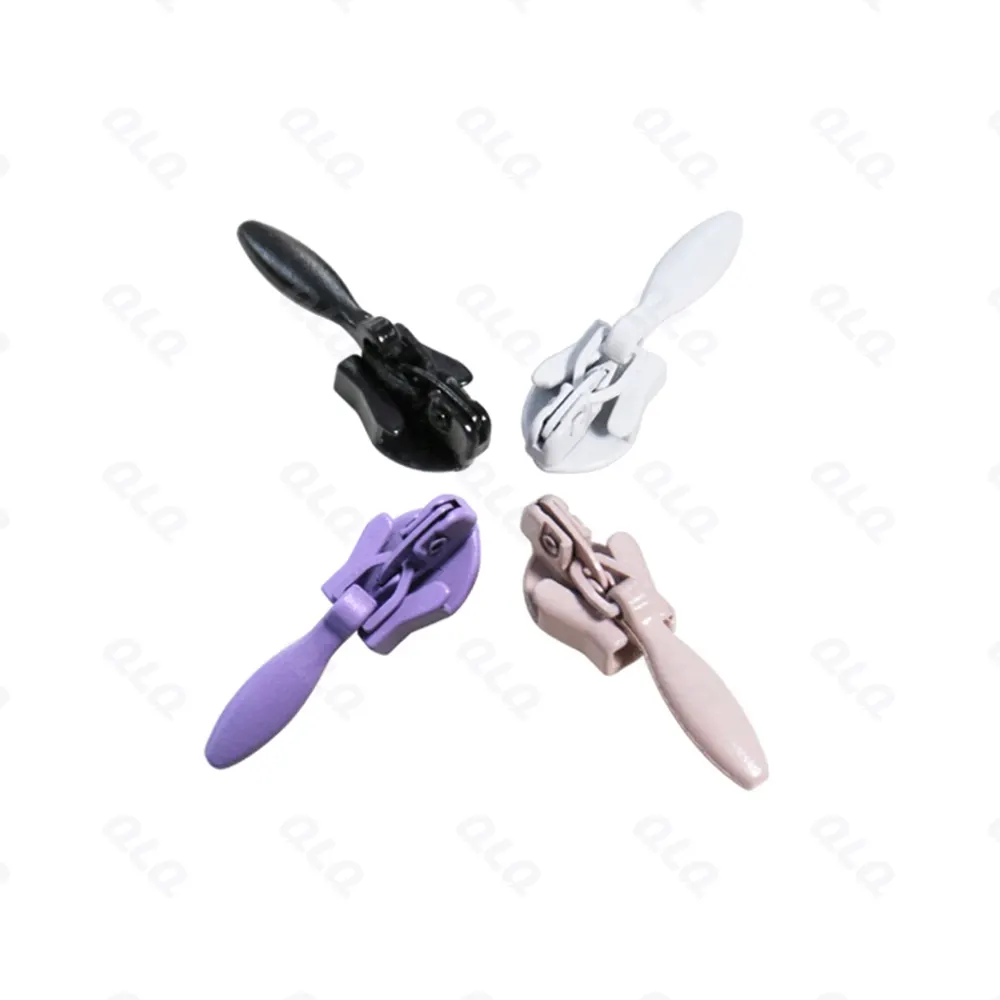
Step 3: Slider Mounting
Machine: QLQ-ISMM Material: Invisible Slider
Please click the following photos for more details.
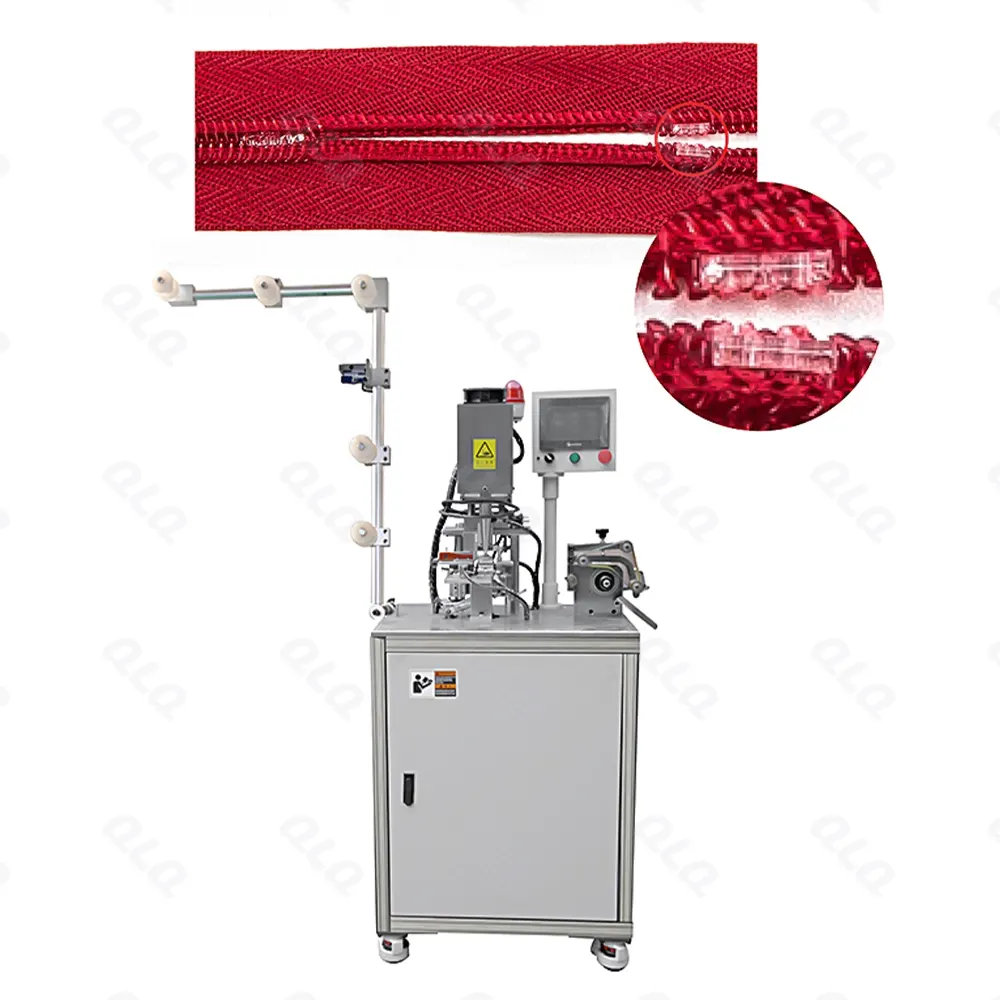
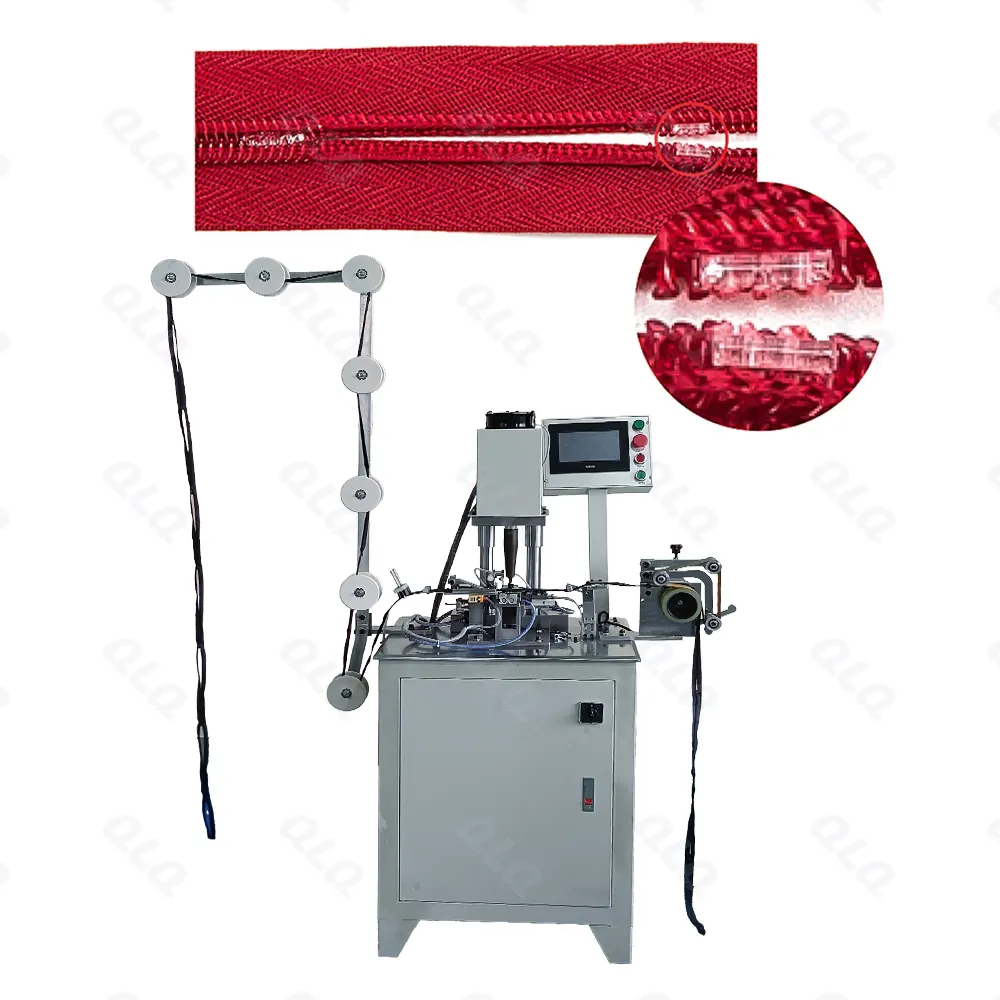
Step 4: "I" Shape Top Stop Fixing
Machine: QLQ-IUIM Material: Transparent Top Stop Round Wire
Please click the following photos for more details.
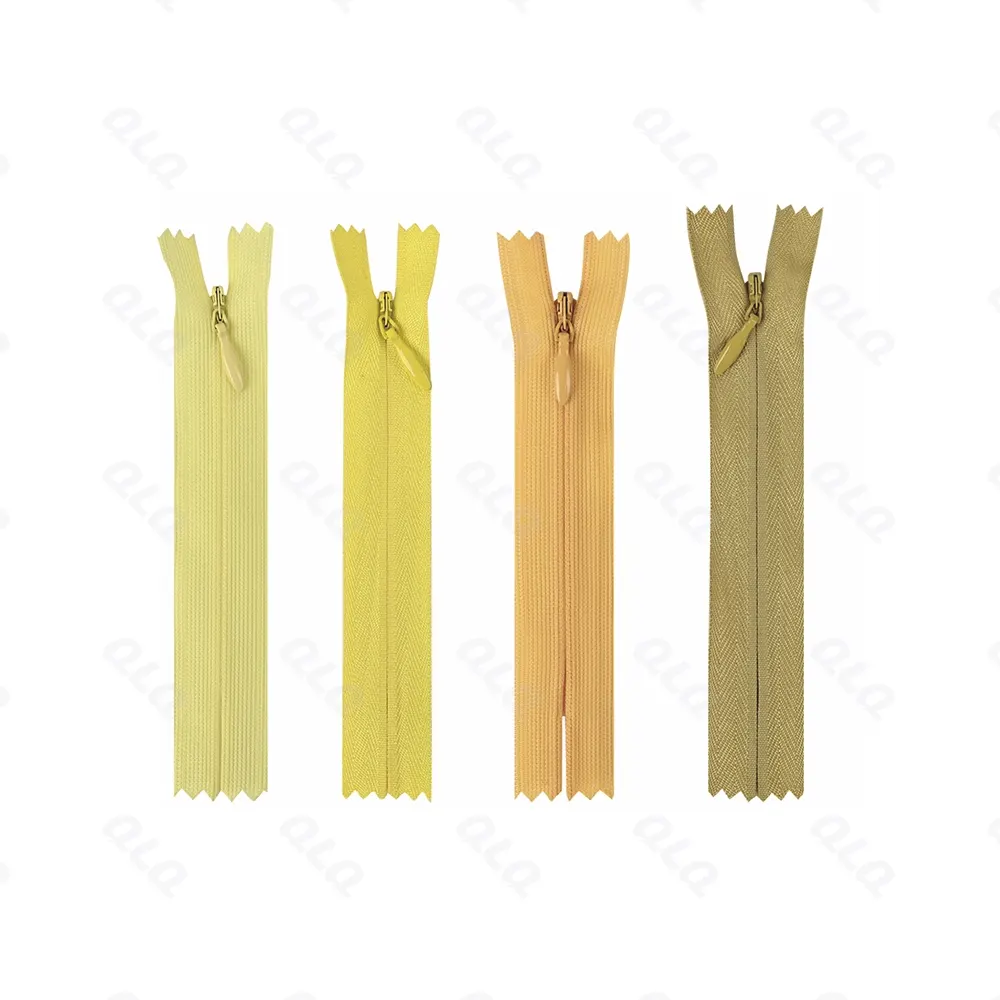
Step 5: Cutting
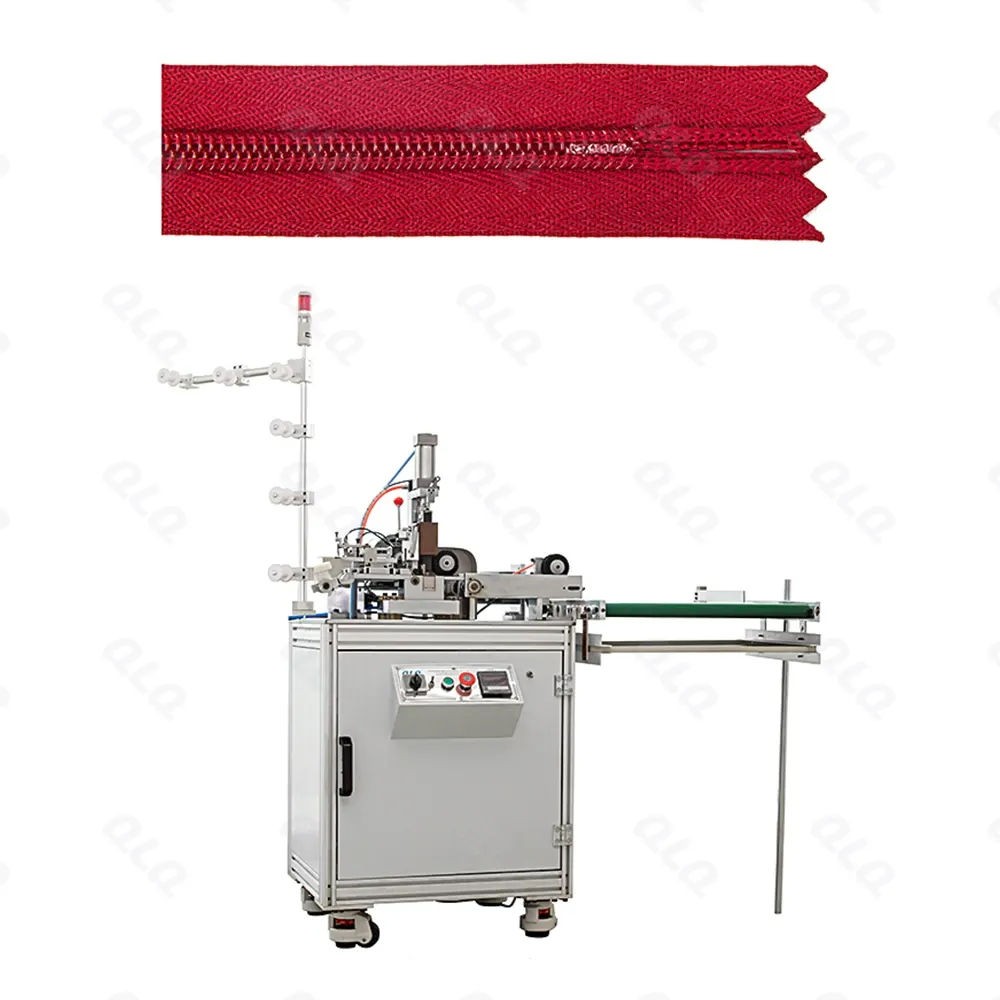
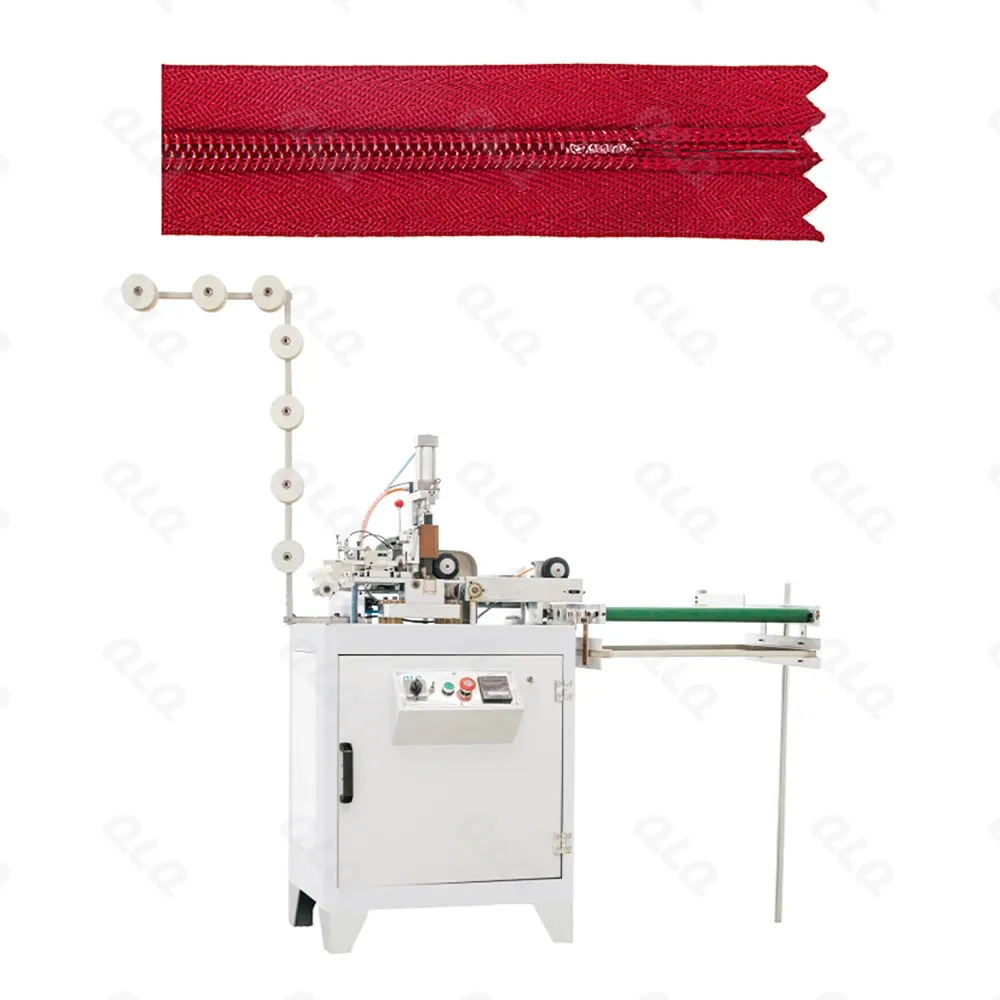
Machine: QLQ-ZCM-1
Please click the following photos for more details.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| Incoming tape / coil | Pitch and width gauge; material batch record | Every batch | Pitch tolerance ±0.05 mm; no flat or deformed teeth |
| Coil forming | Teeth shape, pitch and burr check | Every 30 min | No flat teeth, no burrs, uniform coil profile |
| Stitching / sewing | Stitch density and tape alignment | Every 2 h | Consistent stitch count; no skipped stitches |
| Dyeing | Shade vs lab-dip; color fastness | Every batch | ΔE ≤ 1.0; fastness grade 4+ before packing |
| Heat setting / ironing | Temperature, speed and shrinkage sample | Every 4 h | Shrinkage within customer limit; no over-heated tape |
| Finished zipper | Pull force, slider cycling, AQL sampling | Per lot | Pull force per BS 3084; 20,000-cycle slider test; AQL 2.5 |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Raw material & weaving | 20% | Yarn, monofilament and tape stock; weaving area with stable humidity |
| Coil forming & stitching | 30% | Keep forming and stitching close; cooling water trough beside coil machines |
| Dyeing & heat setting | 25% | Separate zone with water, steam and drainage; exhaust for dye vapor |
| Finishing & packing | 25% | Gapping, stops, slider mounting, cutting, inspection and packing in one flow |
| Utilities | — | Air compressor, cooling tower, dyeing effluent treatment; power per plan (120–300 kW) |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Line operators | Machine operation, tension setting, basic fault call-out | 1–2 weeks per station | Output per shift; defect rate ≤ 2%; machine stop time |
| Machine technician | Mechanical + electrical maintenance, calibration | 2–4 weeks + on-site training | Mean time to repair; preventive maintenance compliance |
| Dyeing master | Recipe, temperature/time control, shade matching | On-site with QLQ training | First-pass shade acceptance ≥ 90% |
| QC inspector | Pull force, cycling, fastness, AQL sampling | 1–2 weeks | Inspection accuracy; missed-defect rate |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Color fastness unstable | Dye recipe, temperature/time control, drying too hot, hard water | Control dyeing temperature and time; check water hardness; verify drying temperature; keep lab-dip standard |
| Yarn breakage on loom | Warp tension, yarn quality, worn heddles/reed, speed too high | Adjust warp tension and let-off; check yarn count; replace worn parts; reduce speed for fine yarn |
| Tape shrinkage too high | Weaving tension, aggressive dyeing, insufficient heat setting | Stabilize weaving tension; control dyeing; run heat setting at 120–140°C with fixed tension |
| Slider jamming on chain | Slider mouth mismatch, unstable chain tension, worn feeder rail | Match slider mouth to chain; stabilize tension; clean/replace rail; check slider orientation |
| Finished length inconsistent | Worn cutter/rollers, tension variation, dirty sensor, dyeing shrinkage | Calibrate sensor every 2–4 weeks; check feeding rollers; fix tension; re-test after dyeing |
| Coil teeth flat or burred | Forming temperature/speed wrong, material variation | Verify forming temperature and speed; check material batch; adjust cooling |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Nylon Zipper Process Parameters
Reference values from QLQ project data and standard nylon zipper practice. Confirm final settings with your line supplier.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| Monofilament line output | 0.48–0.70 mm: 30–60 m/min; 15,000–30,000 m/day per line | Lower speed usually means better diameter consistency; drift above range = gauge variation and coil defects |
| Line-to-machine ratio | 1 monofilament line supports 4–6 stitching machines | More machines per line than supported = starvation and inconsistent coil supply |
| Heat setting temperature | 120–140°C for nylon coil tape | Too low = shrinkage returns; too high = tape stiffening and shade change |
| Dyeing pH (nylon/acid dyes) | pH 4–6, controlled temperature ramp and circulation | pH drift = uneven exhaustion and poor fastness; keep dosing automatic |
| Drying temperature | Below dye-safe limit with airflow | Over-drying = hard hand feel and fastness loss; under-drying = moisture and later shrinkage |
| Slider cycling test | 20,000 cycles per specification | Early failure usually means slider/chain fit or spring quality, not the chain alone |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Front-end equipment | Tape weaving, monofilament extrusion, coil forming, stitching, dyeing, heat setting |
| Finishing equipment | Gapping, hole punching, pin/box fixing, top/bottom stops, slider mounting, cutting |
| Surface treatment | Dyeing, ironing, waterproof film sealing; electroplating and painting lines for metal parts |
| Molds & tooling | Chain teeth molds, slider molds and inserts; 0.02 mm machining precision, H13/SKD61 steel |
| Materials & consumables | Chemicals, lacquer, polishing media, wires, films and spare parts with long-term supply |
| Services | Layout design, installation, commissioning, operator/technician training, remote support |
Frequently Asked Questions
How much space and power does a 50,000-pieces-per-day nylon zipper line need?
A medium nylon line typically needs about 850 m² of production space, 300 kW installed power and 60–90 staff on two shifts. Confirm your exact size mix and whether you weave tape in-house, and QLQ will issue a machine list and layout.
What causes unstable color fastness in nylon zipper dyeing?
Common causes are dye recipe, temperature and time control, drying temperature, tape pretreatment and hard water. Keep a lab-dip standard, control pH 4–6 for acid dyes and check drying temperature before blaming the machine.
Why does the loom keep breaking yarn?
Usually warp tension, yarn quality or worn heddles and reed, sometimes speed too high for the yarn count. Adjust tension and let-off, verify yarn count and replace worn parts; QLQ needle looms have adjustable electronic let-off.
Can I start with finished zipper machines and outsource dyed chain?
Yes. For a first factory, start with finishing machines and buy dyed long chain, then add coil forming, stitching and dyeing after 3–6 months. QLQ supports phased investment so you do not over-invest early.
What testing should a nylon zipper factory own?
Start with a pull-force tester, slider cycling tester and color fastness equipment. Add washing and dry-cleaning testers when supplying international brands. BS 3084 / QB/T 2171 are the common references.
Can machines be built for our local voltage?
Yes. Common options are 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz and 480V/60Hz three-phase. Confirm voltage, frequency and plug type, and it is included in the PI.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Nylon Zipper Production Workshop
Before purchasing equipment, factory owners need clear planning data on quality control, workshop area, workforce, power supply and daily output targets. The table below summarizes realistic planning figures for a typical mid-size nylon zipper line covering tape weaving, coil forming, dyeing and finishing.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | ISO 9001 quality system with BS 3084 / ASTM D2061 / QB/T 2171 testing; pull-force, slider cycling and color-fastness (grade 4+) tests on every batch; hourly chain-pitch and teeth-shape checks during coil forming; final AQL 2.5 sampling before packing. |
| Workshop Area Required | 600–1,500 m² production area plus 150–300 m² for raw material and finished-goods storage; ceiling height above 4.5 m; separate dyeing, ironing and packing zones with proper ventilation. |
| Workforce Needed | 12–25 workers across two shifts: line operators, 1–2 machine technicians, 1–2 QC inspectors and 1 production manager; allow 1–2 weeks of on-site operator training per station. |
| Power Supply | 120–260 kW connected load; 380V/50Hz three-phase (or 220V/480V 60Hz); compressed air at 0.6–0.8 MPa; 5–15 m³/day of water for dyeing and cooling. |
| Daily Production Capacity | Coil forming: 5,000–15,000 m/day; finished nylon zippers: 8,000–20,000 pcs/day for sizes #3–#8, depending on machine speed, size mix and shift pattern. |
| Estimated Gross Margin | 18%–32% on finished zippers; margins increase when tape weaving, dyeing and finishing are done in-house instead of buying pre-dyed tape. |
| Typical Investment Range | $120,000–220,000 for a complete mid-size nylon line (coil forming, stitching, dyeing, ironing and finishing machines). |
| Typical Payback Period | 12–24 months at 70% average utilization with steady export orders. |
Quality First
- Test pull force and slider cycling on every batch
- Keep heat-setting records at 160–200°C per material
- Check chain pitch and teeth shape hourly
- Confirm color fastness grade 4+ before shipping
Workshop & Power
- Floor load capacity of 500 kg/m² or more for heavy machines
- Stable three-phase power with surge protection
- Dry, ventilated dyeing area with clean water supply
- Dust-free packing zone for finished zippers
People & Profit
- Train operators for 1–2 weeks per station
- Assign dedicated QC inspectors before packing
- Gross margin target: 18%–32%
- Payback target: 12–24 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Need a complete nylon zipper line layout, machine list and quotation for your target daily output? Contact QLQ Machinery — we design, supply, install and commission full production lines with operator training and after-sales support.