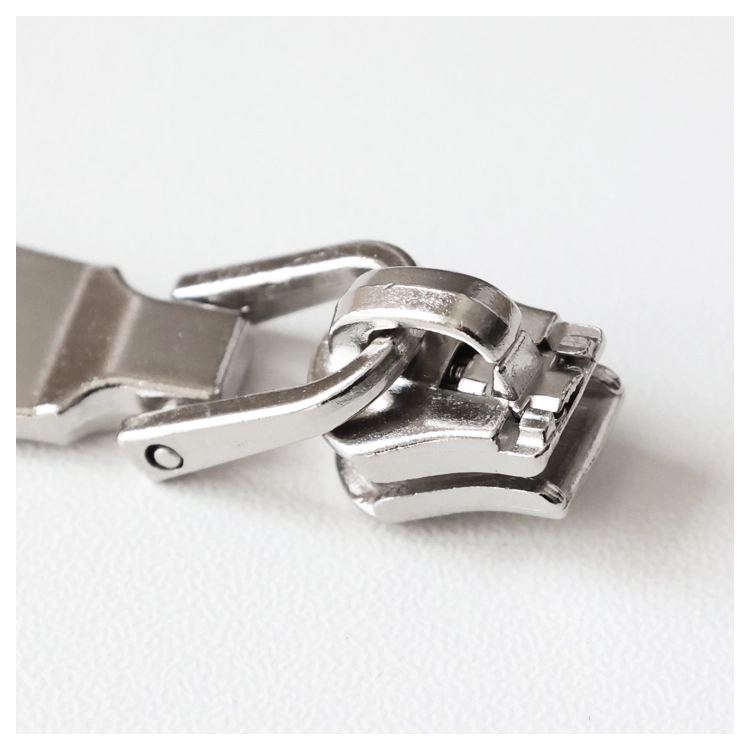
Not all stainless steel is the same, and a slider that survives a jeans wash may fail on a boat cover. The difference is usually the grade: 304 resists general corrosion well, 316 adds molybdenum for salt-water resistance, and magnetic grades such as 420/430 serve special needs where magnetism or heat treatment matters.
This guide helps zipper and slider buyers compare stainless grades for sliders - 304, 316 and magnetic series - covering corrosion behavior, typical marine and outdoor uses, and the incoming material checks that prevent the wrong coil from reaching the stamping press.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Buying stainless by price only | Cheap coils can be low-grade or mislabeled | Require a material certificate and grade marking per coil |
| 2. Using 304 where salt water is constant | Pitting appears on marine exposure | Choose 316 for seawater and constant salt exposure |
| 3. Assuming all stainless is non-magnetic | 420/430 are magnetic by design | Confirm the magnetic requirement before selecting the grade |
| 4. No hardness check on incoming coil | Stamping and springback change with hardness | Test hardness and record per coil |
| 5. Mixing grades in one batch | Corrosion and forming behavior differ | Keep grade lots separate and labeled |
| 6. Ignoring surface quality | Scratches and scale transfer to the slider | Check surface finish on incoming strip |
| 7. Storing coils poorly | Surface contamination causes later spots | Store covered, dry and protected |
| 8. No salt spray baseline | You cannot judge a grade change without a test | Run salt spray samples on every new coil lot |
| 9. Choosing grade after the tool is built | Harder grades wear dies faster | Confirm the grade before tooling and die material selection |
| 10. Copying a 304 part into 316 without re-testing | Forming limits differ slightly | Re-trial and test when the grade changes |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Require material certificates and grade marks per coil
- Use 316 for seawater and constant salt exposure
- Confirm magnetic requirements before grade selection
- Test hardness and surface on every incoming coil
- Keep grade lots separate and labeled through production
- Store coils covered and dry
- Run salt spray samples on every new coil lot
- Re-trial tooling when the grade changes
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Stainless grade selection data for sliders
Reference guidance from QLQ stainless notes; confirm the exact grade and hardness with the coil supplier for your part geometry.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| 304 | General stainless, good corrosion resistance | Suitable for most outdoor and garment use; pitting possible under constant seawater |
| 316 | Contains molybdenum for salt-water resistance | Preferred for marine and high-salt environments |
| 420 / 430 | Magnetic, heat-treatable series | Used where magnetism or special hardness is required |
| Salt spray reference | 48-96 hours for quality stainless parts | Confirm the customer hour target; test every new coil lot |
| Hardness effect | Harder strip wears dies faster | Confirm grade before die material selection |
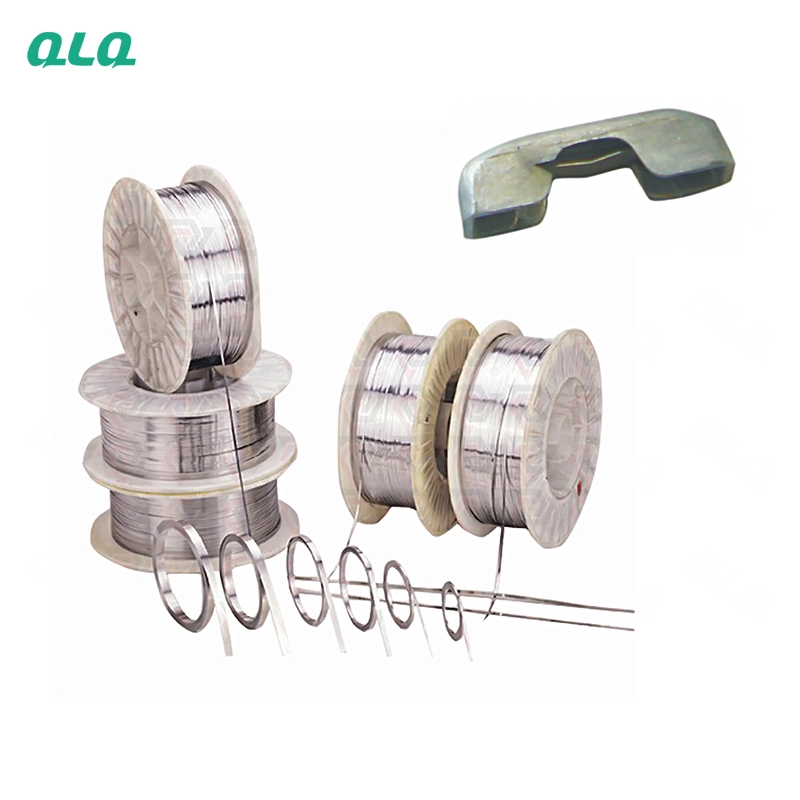
| Incoming check | Certificate, grade mark, hardness, surface | Prevents mislabeled or poor coils reaching the press |
| Formability | Higher grades can be harder to form | Re-trial when the grade changes |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Stainless grade comparison for sliders
| 304 | General purpose | Outdoor, garments, bags | Good balance of corrosion and cost |
| 316 | Salt-water resistant | Marine, diving, boat covers | Higher cost; best corrosion |
| 420/430 | Magnetic series | Special magnetic or heat-treat needs | Check magnetic spec with customer |
Incoming material inspection
| Certificate | Grade and lot from supplier | Required for every coil |
| Grade mark | Visible marking on the coil | Prevents mixing |
| Hardness | Within the spec range | Affects stamping and die life |
| Surface | No scratches, scale or rust | Surface transfers to the part |
| Thickness | Within tolerance | Affects spring force and strength |
Application-driven grade choice
| Jeans and garments | 304 sufficient | General corrosion environment |
| Bags and luggage | 304 standard | Light outdoor exposure |
| Boat covers and marine | 316 preferred | Constant salt exposure |
| Diving and safety gear | 316 | High corrosion requirement |
| Magnetic closures | 420/430 where specified | Customer specification |
Implementation Cases
Case 1 - marine customer moved from 304 to 316
Situation. A customer supplying boat covers saw pitting on 304 stainless sliders after one season in salt water and asked for a corrosion fix.
Approach. The grade was changed to 316 for the slider bodies, spring wire and pullers, with a salt spray baseline test on the new lot before production.
Outcome. The pitting stopped in field use and the factory added a grade confirmation step to its order review for marine customers.
Case 2 - mislabeled coil caught by incoming inspection
Situation. A slider factory in Vietnam received a '304' coil that produced parts with early rust spots and poor forming consistency.
Approach. Incoming inspection with a material certificate check and hardness test flagged the coil before it ran through production, and the supplier replaced the lot.
Outcome. The factory added certificate and hardness checks to every incoming coil and no further mislabeled material reached the press.
Frequently Asked Questions
What is the difference between 304 and 316 stainless for sliders?
304 resists general corrosion well and suits most outdoor and garment use. 316 adds molybdenum for better salt-water resistance, making it the preferred choice for marine exposure.
Is all stainless steel non-magnetic?
No. Austenitic grades like 304 and 316 are usually non-magnetic in the annealed state, while 420/430 are magnetic by design. Confirm the magnetic requirement with your customer.
How do I know which grade I need?
Start from the environment: indoor or general outdoor use usually allows 304; constant seawater and marine use call for 316; special magnetic or heat-treat needs use the 420/430 series.
How should I check incoming stainless coils?
Require a material certificate and grade mark, then check hardness, surface and thickness on each coil. These four checks catch most mislabeled or poor material.
Why does my stainless slider rust in marine use?
Stainless resists corrosion but is not immune. Under constant salt exposure, 304 can pit; 316 is designed for that environment. Surface contamination and poor passivation also cause rust spots.
Does the grade affect my stamping dies?
Yes. Harder grades wear dies faster and change springback. Confirm the grade before building tooling and choose die materials such as tungsten or Cr12MoV for stainless.
What salt spray hours should stainless sliders pass?
Quality stainless parts are often tested at 48-96 hours or more, depending on the customer requirement. Confirm the target and run a baseline on every new coil lot.
Can I switch from 304 to 316 without re-testing?
No. Forming behavior and springback can differ slightly. Re-trial the part and run corrosion samples when the grade changes.
What Would You Like to Solve?
Tell us where the slider will be used, the magnetic requirement and your salt spray target, and we can help you lock the correct grade, thickness and hardness specification before you build tooling or order coils.
Published by QLQ - a complete high-quality zipper manufacturing equipment, moulds and materials solution supplier, and the only supplier in China covering the full process chain from raw material through electroplating and painting as one integrated system. Values cited are project references; confirm with your line supplier before specification.