How to Make Non-lock Slider
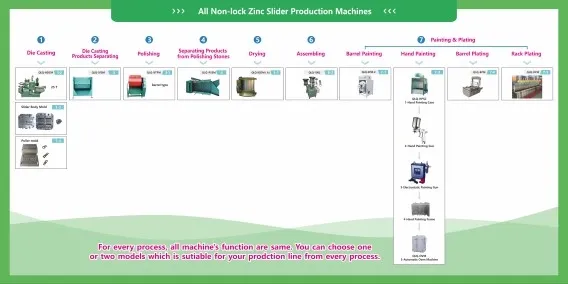
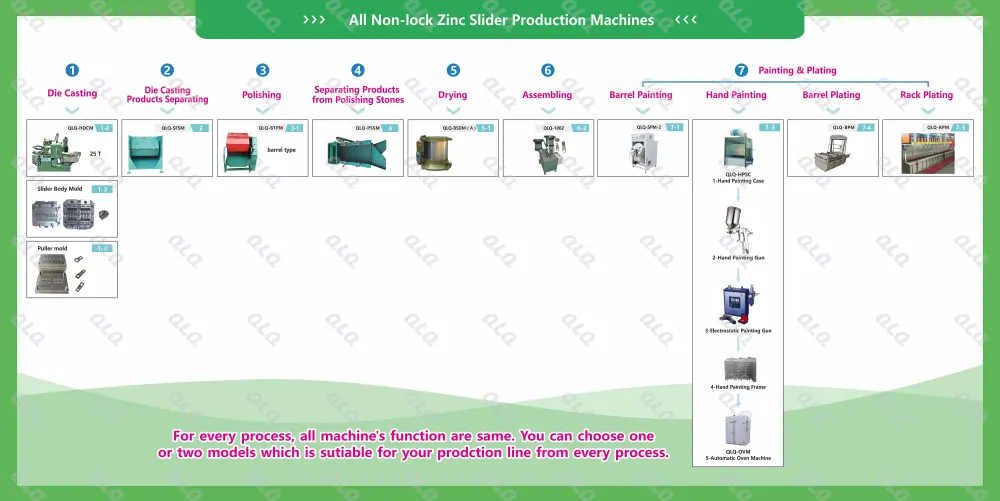
1-Process Chart
2-Process Video
3-Process Details
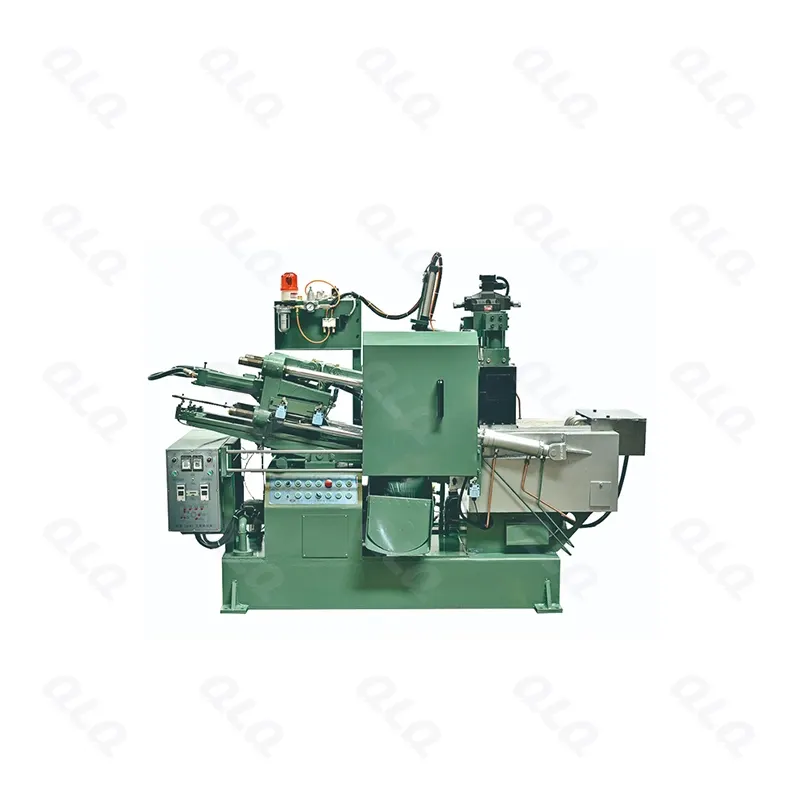
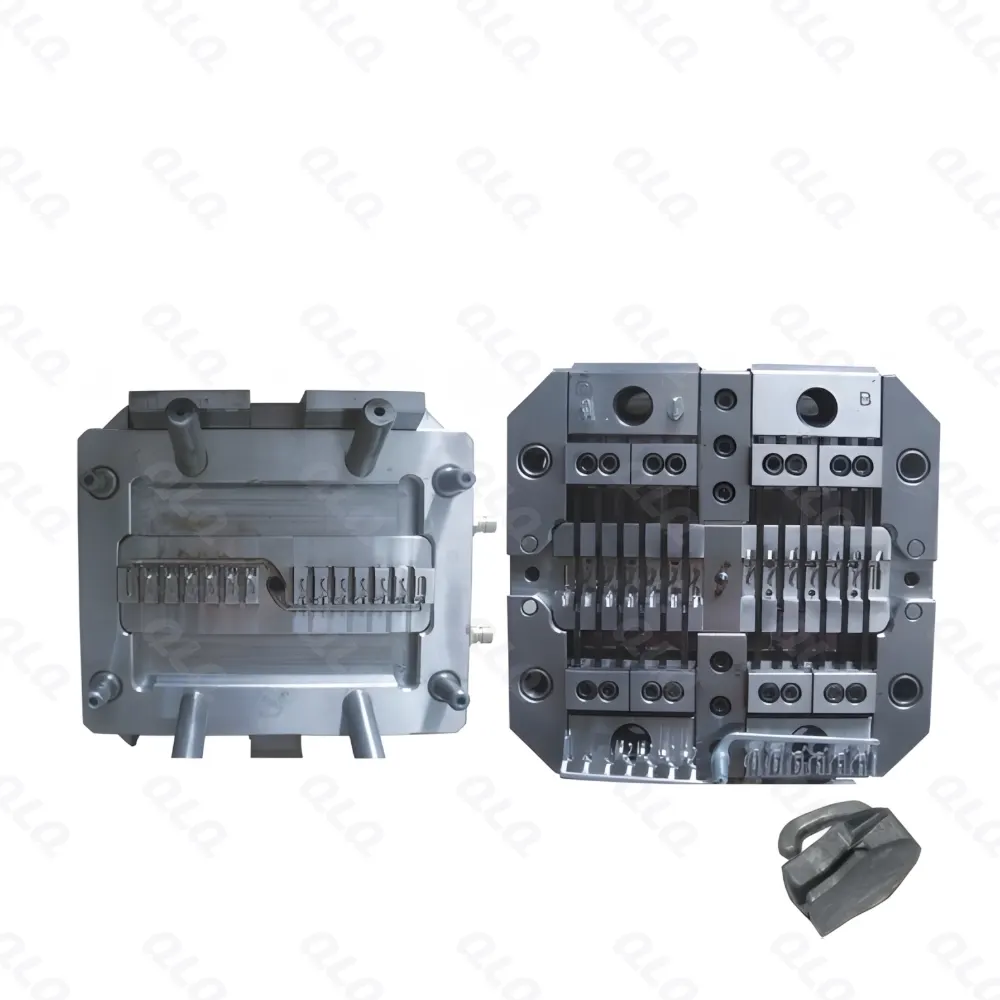
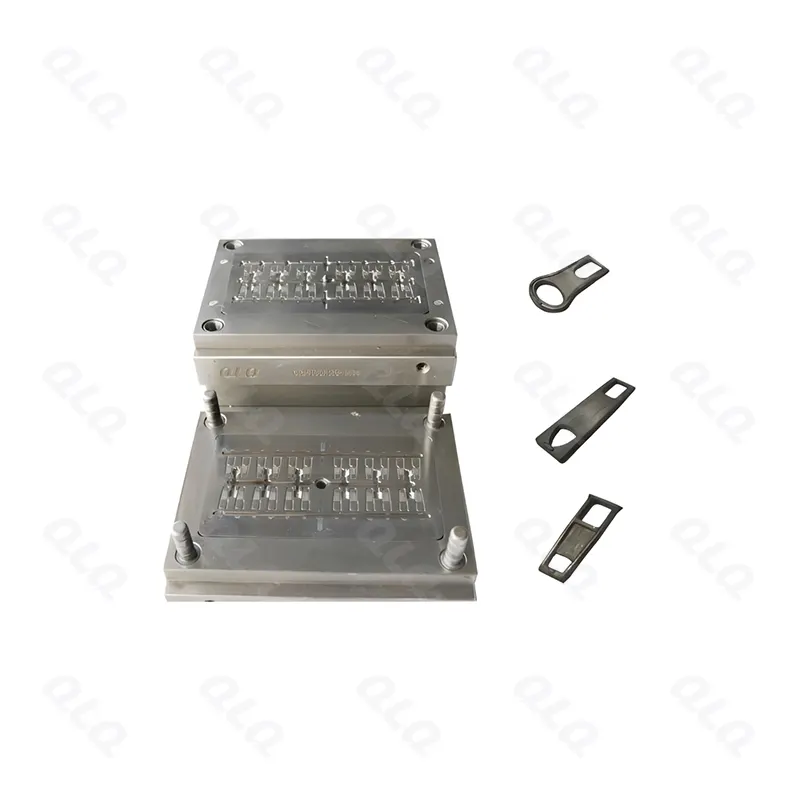
Step 1: Die Casting
Machine: QLQ-HDCM
Please click the following photos for more details.
Step 2: Die Casting Products Separating
Machine: QLQ-SFSM
Please click the following photos for more details.
Description Title
Enter the description here
Step 3: Polishing
Machine: QLQ-BTPM Material: Polishing Stone and Polishing Agent
Please click the following photos for more details.
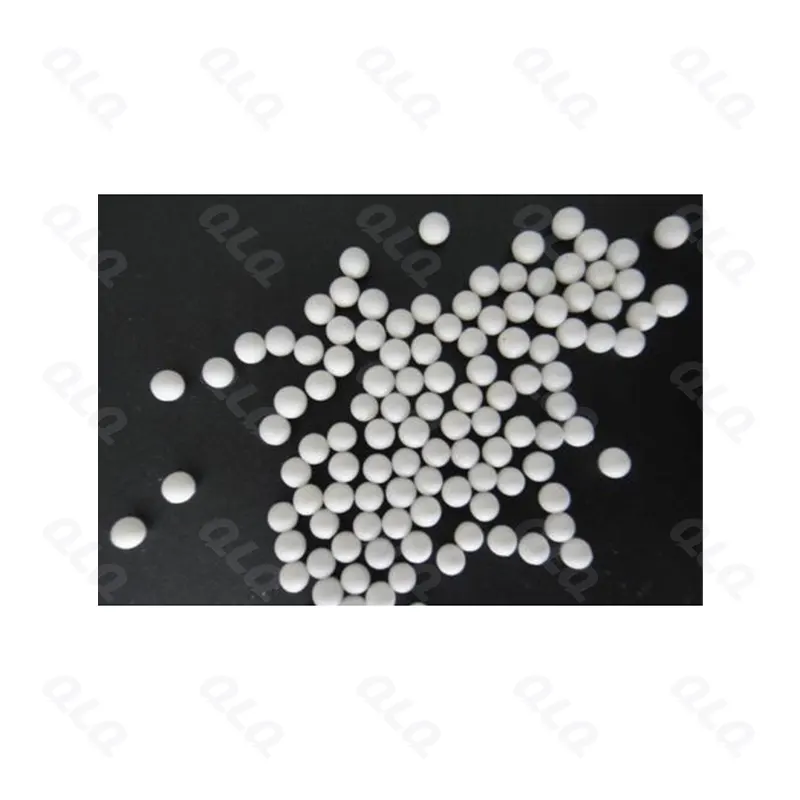
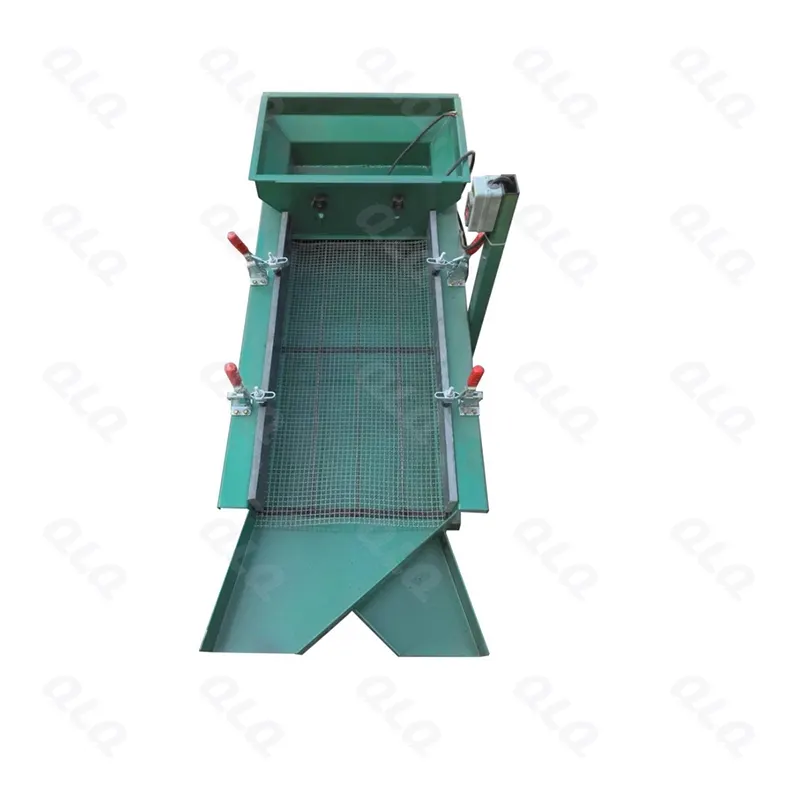
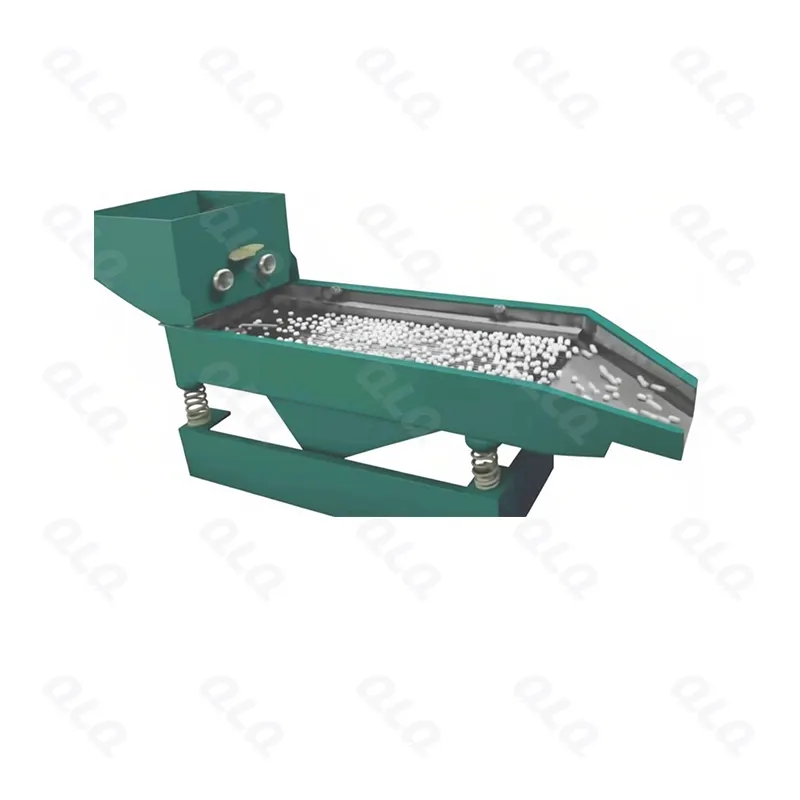
Step 4: Separating Products After Polishing
Machine: QLQ-PSSM
Please click the following photos for more details.
Step 5: Drying
Machine: QLQ-BSDM
Please click the following photos for more details.
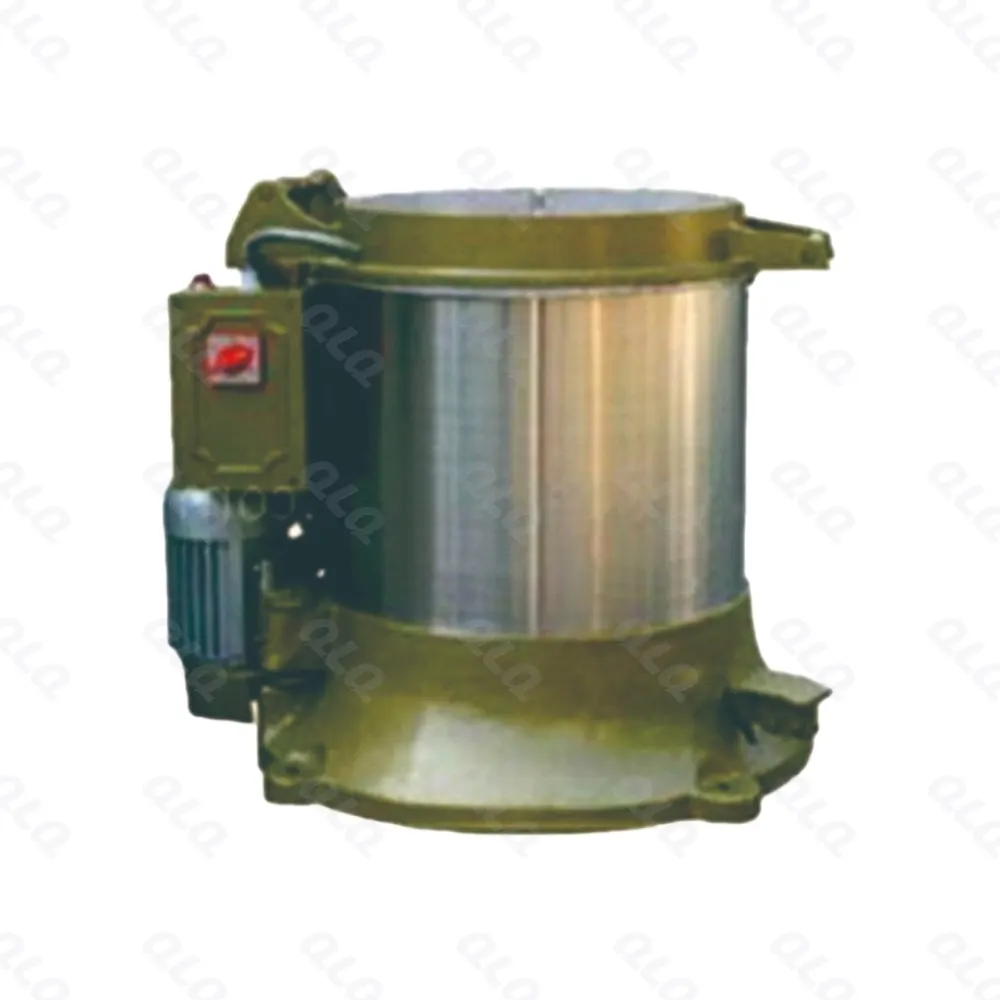
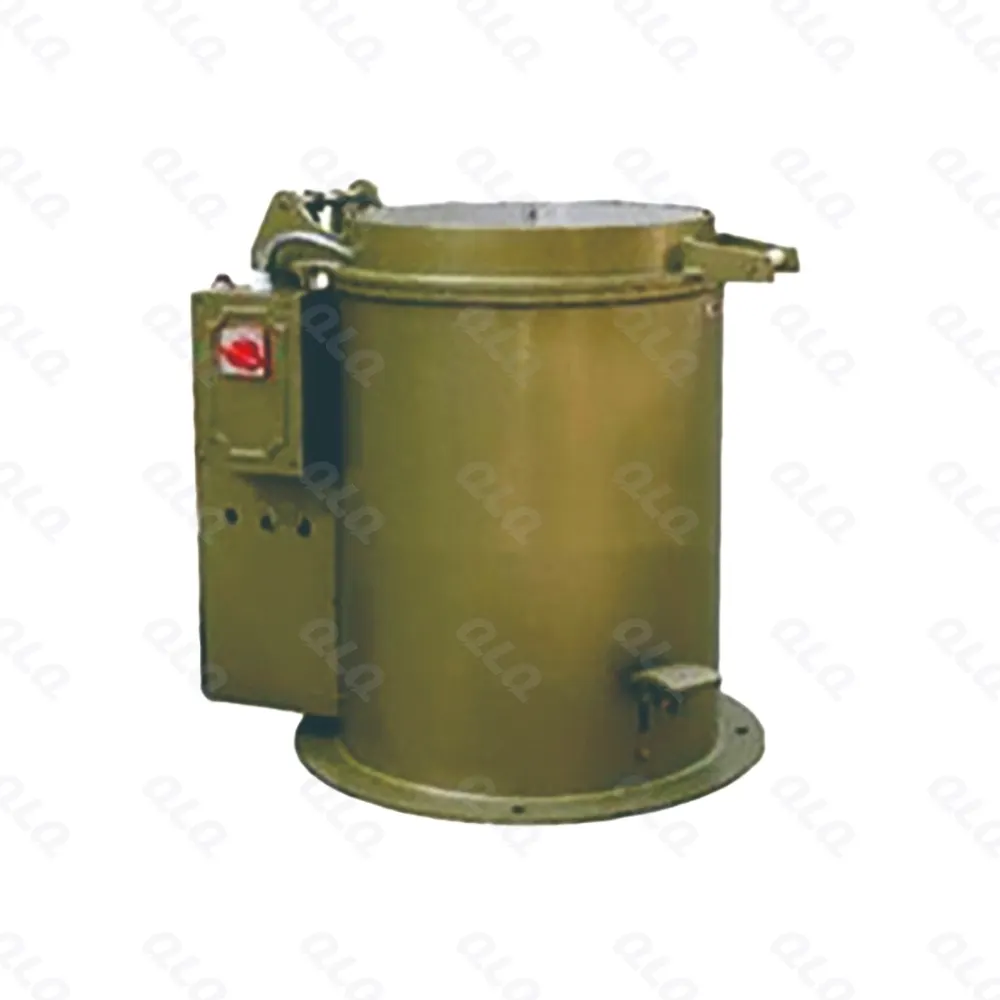
Description Title
Enter the description here
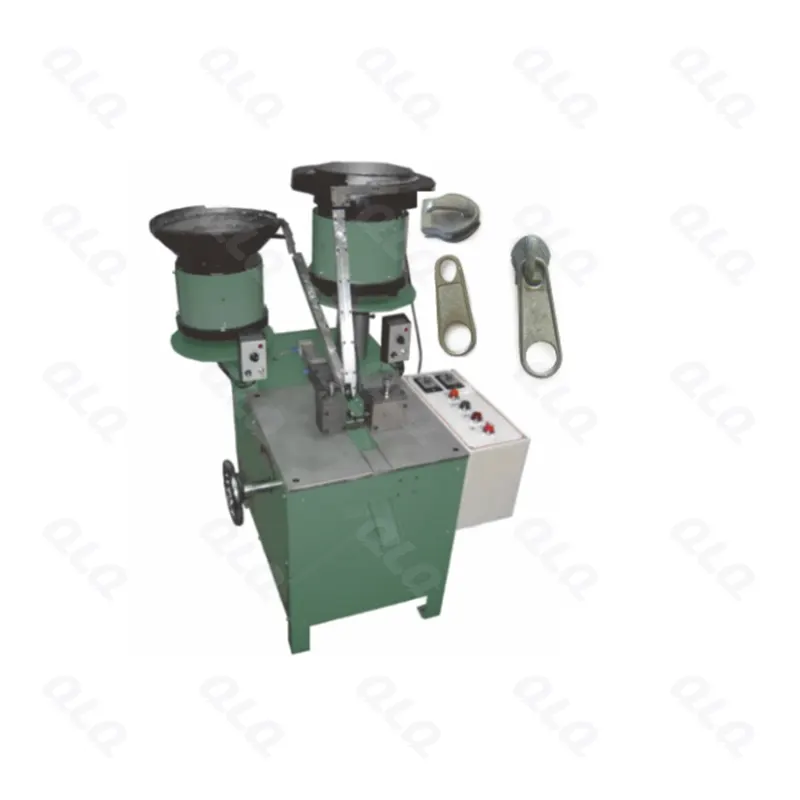
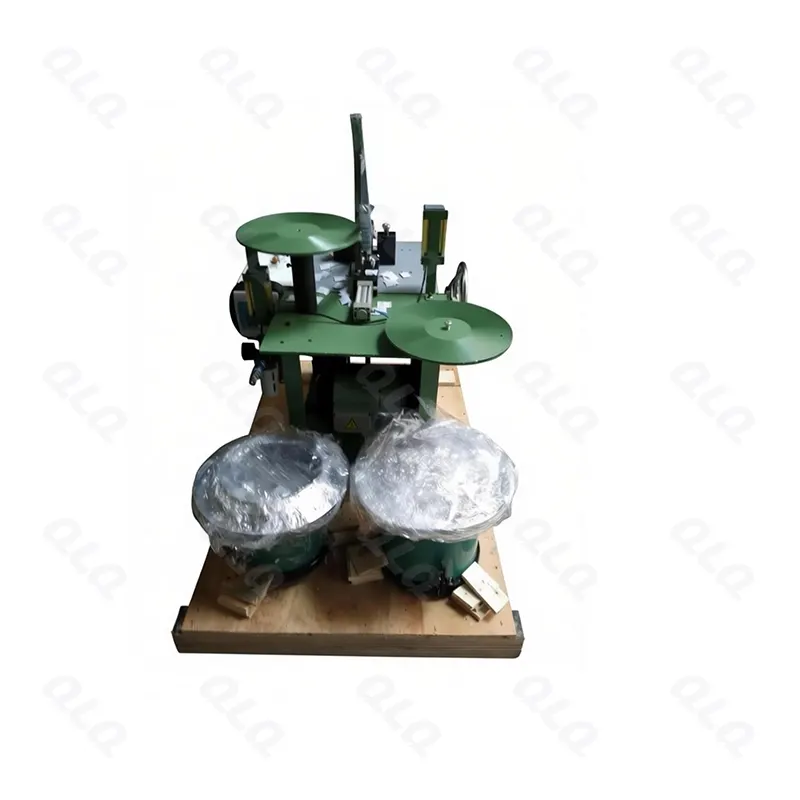
Step 6: Assembling
Machine: QLQ-1002
Please click the following photos for more details.
Step 7: Painting & Plating
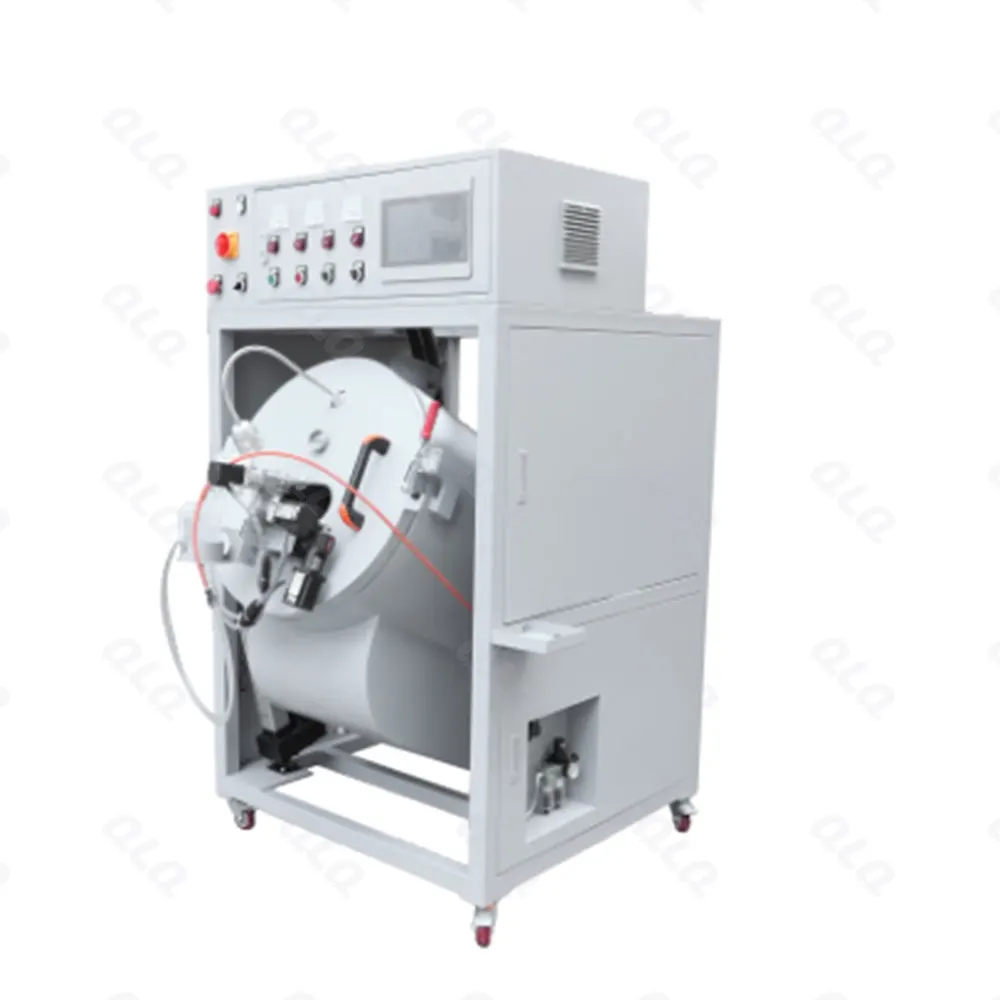
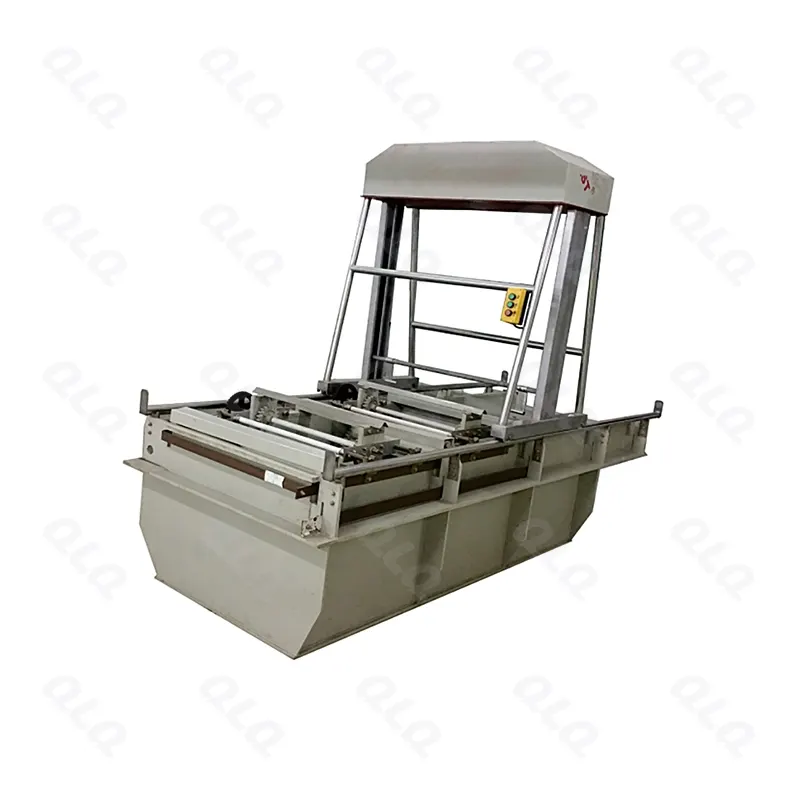
Machines: QLQ-SPM-2, QLQ-BPM and QLQ-RPM
Please click the following photos for more details.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| Zinc alloy incoming | Ingot certificate and composition | Every batch | Consistent alloy for stable casting |
| Die casting | Density, flash, surface porosity | Every 30 min | No porosity at critical sections; flash within trim allowance |
| Trimming & deburring | Gate and flash removal | Every 2 h | Clean edges; no burrs affecting assembly |
| Polishing | Surface smoothness and media residue | Per batch | Plating-ready surface; no deep scratches |
| Plating | Thickness, adhesion, salt spray | Per batch | Multi-layer Cu/Ni/topcoat; 24–48 h salt spray |
| Assembly & lock test | Spring tension, lock function, cycling | Per lot | Auto-lock engages; cycling per ASTM D2061; AQL 2.5 |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Die casting | 30% | Hot-chamber machines 25T–68T; melting area separated with fume extraction |
| Trimming & polishing | 20% | Oil presses and centrifugal/vibratory polishing; dust and water handling |
| Plating / painting | 25% | Isolated surface treatment area with exhaust and wastewater treatment |
| Assembly & QC | 25% | Slider assembly machines, testing and packing in one flow |
| Utilities | — | Air, cooling water, exhaust and fire protection near furnaces |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Die-cast operators | Machine cycle control, die change, shot inspection | 1–2 weeks | Casting yield; flash rate; die change time |
| Polishing staff | Media selection, cycle, residue wash | 1 week | Surface reject rate; media consumption |
| Plating technician | Bath control, rectifiers, thickness test | On-site QLQ training | First-pass plating yield; thickness variance |
| Assembly & QC | Spring assembly, lock test, AQL sampling | 1–2 weeks | Assembly yield; missed-defect rate |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Slider body porosity | Melt temperature, shot speed, gate design, alloy | Adjust shot profile; check melt temperature; review gate and venting |
| Slider too tight or too loose on chain | Mouth size, lock pin height, body shape | Adjust mouth or specification; match to chain and tape sample |
| Spring/lock fails cycling test | Spring material, assembly depth, cap fit | Check spring temper and assembly depth; verify cap seating |
| Plating dull or patchy on sliders | Bath imbalance, pre-cleaning, current density | Check brightener and temperature; improve cleaning; verify rectifier settings |
| Mold wears early | Cooling design, maintenance, steel grade | Follow maintenance schedule; clean cooling channels; upgrade inserts |
| Exhaust/ventilation insufficient | No local hood above machines | Add local exhaust per machine; separate melting area with strong extraction |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Slider Production Data
Reference values from QLQ project data and standard die-casting practice. Confirm final parameters with your line supplier.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| Die-cast tonnage selection | 25T small parts; 30T medium fast-cup; 38T core #3–#8; 50–68T large sliders | Under-tonnage = flash and porosity; over-tonnage = wasted energy and tool stress |
| Mold life | H13 80,000–150,000 shots; premium 200,000+ | Regular cleaning, polishing and cooling-channel checks extend life 30–50% |
| Wear part intervals | Gooseneck 300k–500k; plunger tip 50k–150k; nozzle 100k–200k shots | Keep 1–2 sets in stock per machine to avoid downtime |
| Plating layers | Copper + nickel + topcoat for decorative sliders | Missing layers = adhesion failure and early salt spray corrosion |
| Salt spray target | 24–48 h neutral salt spray | Failure = thickness, porosity or topcoat issue; check bath and pre-cleaning |
| Cavity count | 2-cavity typical; 4–6 cavity on 38T for high volume | Output scales 1.6–1.8× per doubling with balanced cooling |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Die-casting equipment | Hot-chamber machines 25T–68T, mold temperature controllers, melting furnaces |
| Molds & tooling | Slider body molds, puller molds, inserts; 0.02 mm precision, H13/SKD61 steel |
| Surface treatment | Polishing machines and media; barrel/rack plating; painting and lacquer lines |
| Assembly equipment | Slider assembly machines for auto-lock, non-lock and special sliders |
| Materials & consumables | Zinc alloy guidance, chemicals, lacquer, polishing media and spare parts |
| Services | Layout design, mold plan, installation, training and remote support |
Frequently Asked Questions
How do I choose between a 25T and 38T die-casting machine?
25T suits small sliders, badges and samples under 30,000 pieces/day. 38T is the main model for #3–#8 slider bodies and multi-cavity molds. QLQ usually recommends 2–3 units of 38T plus one 25T/30T for small parts.
How long does a slider mold last?
Standard H13 molds last 80,000–150,000 shots; premium heat-treated steel exceeds 200,000. Insert-type molds replace only inserts. Maintenance can extend life by 30–50%.
Why is my slider too tight or too loose on the zipper?
It is usually the mouth size, lock pin height or body shape. QLQ adjusts the mouth or specification and matches the slider to your chain and tape sample.
Can sliders be made nickel-free for EU and baby products?
Yes. QLQ controls zinc alloy composition, plating chemicals and topcoat to meet REACH, OEKO-TEX and CPSIA requirements. Confirm the target market and test standard.
How often should gooseneck and plunger tips be replaced?
Gooseneck/shot sleeve 300,000–500,000 shots, plunger tip 50,000–150,000, nozzle 100,000–200,000. Keep 1–2 sets in stock per machine.
Centrifugal or vibratory polishing for sliders?
Centrifugal barrels are faster and brighter for high volume; vibratory is gentler for delicate parts. Many factories run both: rough polish, then fine finish.
What testing does a slider line need?
Pull-force tester, slider cycling tester and salt spray tester as the core set; add washing/fastness testing for brand customers.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Zipper Slider Production Workshop
Zipper slider production covers zinc-alloy die casting, polishing, plating and assembly, which makes site planning, power supply and environmental permits critical. The table below summarizes realistic planning figures for a typical mid-size slider workshop.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | BS 3084 / ASTM D2061 / QB/T 2171 testing with casting density and surface inspection; spring tension and lock-function checks; plating thickness and adhesion tests; slider cycling tests (20,000–50,000 cycles per specification); salt-spray resistance of 24–48 hours; final AQL 2.5 sampling. |
| Workshop Area Required | 800–1,800 m² production area plus 200–300 m² warehouse; separate die-casting, polishing, assembly and plating sections; fume and dust extraction; wastewater treatment area for the plating line. |
| Workforce Needed | 20–45 workers across two shifts: die-casting operators, polishing staff, assembly operators, 1–2 plating technicians, 2–3 QC inspectors and 1–2 production managers. |
| Power Supply | 200–450 kW connected load (die-casting machines and plating rectifiers dominate); 380V/50Hz three-phase (or 220V/480V 60Hz); compressed air at 0.6–0.8 MPa; 10–30 m³/day of process water. |
| Daily Production Capacity | 50,000–150,000 slider pieces/day from die casting; 30,000–80,000 assembled sliders/day per assembly line, depending on slider type and automation level. |
| Estimated Gross Margin | 22%–38% on finished sliders; in-house die casting, polishing and plating provide the strongest margin control. |
| Typical Investment Range | $200,000–400,000 including die-casting machines, molds ($15,000–60,000 per slider type), polishing, plating and assembly equipment. |
| Typical Payback Period | 18–30 months at 70% average utilization with steady slider supply contracts. |
Quality First
- Inspect casting density and surface for porosity
- Test spring tension and lock function per batch
- Measure plating thickness and adhesion
- Run cycling tests before final packing
Workshop & Power
- Separate die casting, polishing and plating areas
- Install fume and dust extraction systems
- Provide wastewater treatment for plating lines
- Ensure stable power for rectifiers and die casters
People & Profit
- Train die-casting and plating operators thoroughly
- Use dedicated QC for assembly stations
- Gross margin target: 22%–38%
- Payback target: 18–30 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Building a slider production workshop? Contact QLQ Machinery for a complete line design, mold planning, machine list and quotation tailored to your target slider types and output.