Every Hour of Downtime Costs You Real Money
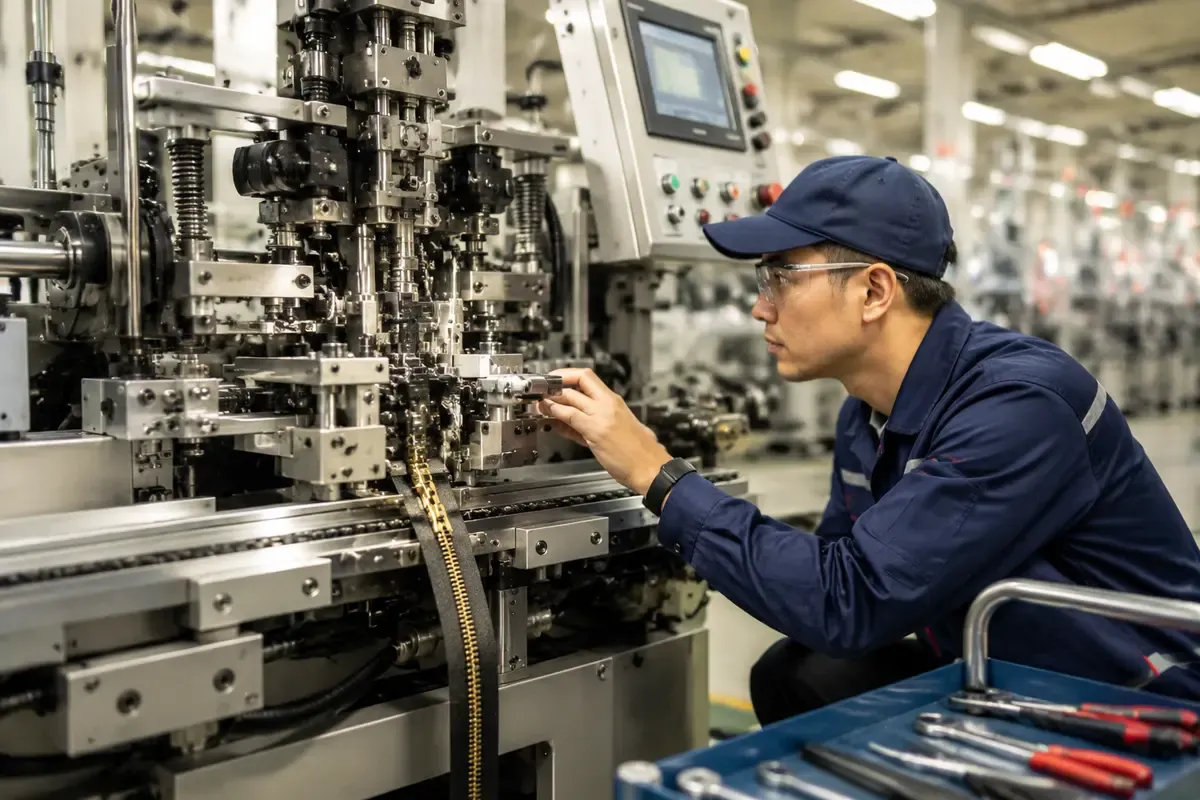
A single unplanned shutdown on a metal zipper forming press can cost $800-2,500 in lost production. Over a year, factories without structured maintenance programs lose an average of 18-22 production days to preventable failures. The difference between a 5-year machine and a 15-year machine is not the brand — it's the maintenance routine. This guide provides actionable preventive care schedules for every major zipper machine type, built from real-world service data across 200+ factory installations.
Why Preventive Maintenance Matters More Than Repairs
Reactive maintenance — waiting for a machine to break before fixing it — is the most expensive approach to factory management. Studies from the textile machinery sector show that preventive maintenance reduces total maintenance costs by 25-35% compared to breakdown maintenance, because you avoid cascading damage: a worn bearing left unchecked destroys the shaft, then the gear set, then the entire drive train.
Universal Daily Maintenance Checklist (All Machine Types)
These 10-minute checks apply to every zipper production machine on your floor — forming presses, coiling machines, sewing stations, cutting machines, injection molders, and finishing lines. Train every shift operator to complete this list before starting production:
- Visual inspection: Walk around the machine. Look for loose fasteners, oil leaks, frayed cables, or unusual wear marks on moving parts.
- Clean contact surfaces: Wipe down zipper tape guides, feed rollers, and die surfaces. Tape dust and metal particles act as abrasive contaminants.
- Check lubrication points: Verify oil levels in central lubrication reservoirs and confirm oil is reaching all grease nipples. Dry bearings fail within hours.
- Test emergency stops: Press each E-stop button and verify the machine halts instantly. This is a safety requirement, not optional.
- Listen for abnormal sounds: Run the machine at low speed for 30 seconds. Grinding, clicking, or rhythmic knocking indicates developing faults.
- Check air pressure (pneumatic machines): Verify the pressure gauge reads within the machine's specified operating range — typically 0.5-0.8 MPa.
Weekly Maintenance by Machine Type
Metal Zipper Tooth-Forming Machines (QLQ-YTSM Series)
These high-impact stamping machines experience the most mechanical stress in any zipper factory. Weekly care is non-negotiable:
- Inspect die surfaces under magnification for micro-cracking. Replace dies showing any surface fatigue — one cracked die can destroy an entire batch of teeth and damage the mating die.
- Check punch-to-die alignment with a feeler gauge. Misalignment beyond 0.02mm causes asymmetric tooth forming and accelerates die wear.
- Flush and replace stamping oil in the recirculation system. Metal particulate accumulates rapidly in high-pressure forming environments.
- Verify Y-wire feed tension — inconsistent tension produces teeth with variable dimensions that fail QC inspection.
Nylon Coiling & Sewing Machines (QLQ Sewing Series)
Coiling and sewing stations handle flexible materials at high speed, making them susceptible to alignment drift and thread path wear:
- Clean monofilament guides and heating elements — nylon residue buildup alters coil geometry and causes irregular tooth spacing.
- Check needle condition — replace sewing needles every 40-50 production hours, or sooner if the machine operates on abrasive tapes.
- Verify stitch tension balance between top and bottom threads. Imbalanced tension produces wavy zipper tape that fails flatness inspection.
- Lubricate all sewing head moving parts per manufacturer oil specification (typically ISO VG 32 spindle oil).
Cutting & Gapping Machines (QLQ-ZCM / QLQ-DGM / QLQ-MDGM Series)
Cutting machines rely on blade sharpness and precise stop-position control. Degraded cutting edges produce frayed tape ends and inconsistent gap lengths — the top two rejection reasons from garment factories:
- Sharpen or replace cutting blades every 2 weeks under normal load, weekly under high-volume production (>15,000 pieces/day).
- Clean the cut-length sensor (optical or mechanical encoder) — dust on the sensor causes measurement drift, producing batches of zippers 1-3mm off-spec.
- Inspect pneumatic cylinders for smooth actuation. Sticky cylinder movement creates inconsistent cut pressure and ragged edges.
- Verify stop-position repeatability by measuring 10 consecutive cuts with calipers. Deviation should stay within ±0.5mm.
Injection Molding Machines (QLQ-DCIM Series)
Plastic injection machines for zipper stops and pin boxes operate at high temperatures and pressures. Neglected maintenance leads to material degradation inside the barrel and mold cavity damage:
- Purge the barrel at the end of each production week, especially when switching between POM colors or between POM and ABS materials.
- Clean mold cavities with approved mold cleaners — never use metal scrapers that scratch the polished cavity surface.
- Check heating band connections for tightness. Loose electrical connections on barrel heaters cause temperature fluctuation, resulting in incomplete mold filling.
- Inspect the clamping unit for parallel alignment. Misaligned platens cause uneven mold closure and produce flash on molded parts.
Monthly & Quarterly Maintenance Schedule
Spare Parts Inventory: What to Stock and Why
One of the most common factory mistakes is waiting until a part fails to order a replacement. International shipping on urgent spare parts adds $200-800 in express freight and 5-10 days of downtime that proper planning eliminates entirely.
- Die sets (forming machines) — 1 backup set per size produced
- Drive belts — 2 sets for each machine model
- Cutting blades — minimum 4-6 blades per cutting machine
- Heating elements/bands (injection machines) — 2 complete sets
- Common bearings and seals — 2 sets per machine model
- PLC power supplies and I/O modules — 1 backup of each
- Sensors and limit switches — 2 of each type used in your factory
Building Your Maintenance Culture
Equipment lasts as long as the people maintaining it care about the outcome. The most successful zipper factories we work with share three organizational practices:
1. Operator Ownership
The person who runs the machine every day is the first line of defense. Give operators the authority to stop production when they hear or see something wrong — and reward them for doing so, not penalize them for "lost output."
2. Maintenance Log, Not Maintenance Memory
Every lubrication, every belt change, every sensor calibration gets recorded with date, technician name, and part serial number. When a pattern emerges — "the #3 forming press needs belt tensioning every 45 days instead of 90" — you can schedule proactively instead of reacting to another breakdown.
3. Annual Overhaul Budget
Set aside 5-8% of each machine's replacement cost annually for comprehensive overhaul: complete disassembly, wear-part replacement, repainting, and recalibration. Factories that budget for annual overhauls see 3x longer equipment life compared to those that run machines until something catastrophic fails.
When to Call for Professional Service
Some maintenance tasks require factory-trained technicians with specialized tools and diagnostic equipment:
- PLC reprogramming or firmware updates — incorrect parameters can cause safety hazards
- Major bearing or spindle replacement — requires precision alignment tools and torque specifications
- Hydraulic system overhaul — high-pressure systems demand certified service procedures
- Annual comprehensive calibration — ensures all stations meet original factory specifications
Maintenance as a Competitive Advantage
In a commodity-driven industry where zipper prices fluctuate within narrow bands, the factory with higher machine uptime and longer equipment lifespan has a structural cost advantage that competitors cannot easily replicate. A well-maintained QLQ forming press running at 95% uptime over 15 years delivers roughly 40% lower cost per meter than a neglected machine replaced every 6 years. That margin compounds across every machine on your floor.
Want a customized maintenance schedule for your specific machine configuration? Our service engineers can develop a machine-specific preventive maintenance plan based on your production volume, shift structure, and operating environment. Download the technical documentation for any machine on our product pages to access full lubrication specifications, spare parts lists, and service interval tables.
Production Standards & Quality Gates
The checkpoints a zipper factory should run to keep output consistent and traceable.
| Stage | Check | Frequency | Acceptance Limit |
|---|---|---|---|
| Factory quality system | ISO 9001-style management with QC gates | Continuous | Documented procedures for each process |
| Incoming material | Yarn, wire, pellets, chemicals certificate | Every batch | Material traceability to supplier batch |
| In-process control | Process checkpoints per line | Per shift | Parameters recorded and signed |
| Final inspection | Pull force, slider, appearance, AQL | Per lot | AQL 2.5 sampling; records kept for claims |
| Testing equipment | Pull-force, cycling, salt spray, color fastness | Calibrated | Calibration schedule and records |
| Staff assessment | Skill matrix and first-pass yield per operator | Weekly | Training plan tied to defect data |
Workshop Layout & Material Flow
Zone planning keeps material moving one way and keeps dyeing, plating and painting separated from packing.
| Zone | Space Share | Planning Notes |
|---|---|---|
| Raw material & warehouse | 15% | Yarn, wire, pellets and chemicals with FIFO storage |
| Production zones | 55% | One flow per product line; separate dyeing/plating/painting zones |
| QC & lab | 10% | Pull-force, cycling, salt spray and color fastness equipment |
| Packing & finished goods | 15% | Dust-free packing and storage |
| Utilities & treatment | 5% | Air, cooling water, wastewater and exhaust |
| Planning reference | — | Small 200–400 m²/150–250 kW; medium 600–1,000 m²/300–500 kW |
Personnel Training & Assessment
A practical skill matrix with training time and measurable KPIs per role.
| Role | Core Skills | Training | Assessment KPI |
|---|---|---|---|
| Line operators | Machine operation and process checks | 1–2 weeks per station | Output/shift; defect rate; stop time |
| Technicians | Mechanical, electrical and mold maintenance | 2–4 weeks + on-site | MTTR; preventive maintenance compliance |
| Process engineer | Parameter setting, problem solving, training | Project-based | First-pass yield; complaint rate |
| QC inspectors | Inspection, testing, AQL sampling | 1–2 weeks | Missed-defect rate; report accuracy |
Common Problems and How to Fix Them
The failures that show up most often in real projects, with the cause and the practical fix.
| Problem | Why It Happens | Practical Fix |
|---|---|---|
| Capacity mismatch after start-up | Line designed without real product mix | Define sizes and mix first; start one line, stabilize, then expand |
| Color contamination between materials | Different fibers dyed in same machine | Separate dyeing by material; acid dyes for nylon, disperse for polyester, reactive for cotton |
| Wastewater/environment approval delays | Treatment planned too late | Plan dyeing/plating/painting permits before line design |
| Power instability | No power plan before installation | Confirm local voltage/frequency and total kW; add stabilizers if needed |
| Operator quality varies | No training or assessment system | Use skill matrix, weekly defect review and first-pass-yield targets |
| Machine downtime high | No spare parts stock | Keep critical wear parts in stock; QLQ supplies spares with long-term support |
Step-by-Step Production Guide
A practical sequence that can be adapted to your own project.
Working Data & Formula Notes
Factory Planning Data
Reference values from QLQ new-factory quick tables and real customer projects. Confirm with your line supplier before specification.
| Component / Parameter | Working Value / Role | What Changes Mean |
|---|---|---|
| Small factory reference | 10,000–20,000 pcs/day: USD 80k–150k equipment; 200–400 m²; 150–250 kW; 15–35 staff | Under-budgeting utilities or staff = slow start-up and quality swings |
| Medium factory reference | 30,000–50,000 pcs/day: USD 150k–300k equipment; 600–1,000 m²; 300–500 kW; 30–90 staff | Scope creep on product mix raises both area and power needs |
| First-line rule | Start with one complete line for one product type | Mixed lines at start = training gaps and higher defect rates |
| Stabilization period | 3–6 months before adding capacity | Expanding too early multiplies problems before they are solved |
| Voltage options | 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz, 480V/60Hz | Confirm before order; wrong voltage costs installation time |
| On-site support | 1–2 engineers for 7–15 days; longer support by arrangement | First factories benefit most from on-site commissioning and training |
QLQ Full-Solution Coverage
QLQ supplies the complete set of high-quality zipper manufacturing equipment, molds and materials, and is the only manufacturer in China covering the full process chain from raw materials through electroplating and painting. Machines, molds, chemicals and consumables are matched as one system, so the line starts faster and runs more predictably.
| Scope | What QLQ Provides |
|---|---|
| Complete equipment line | Front-end, finishing and surface treatment machines for nylon, metal and plastic zippers |
| Molds & tooling | Slider, teeth and stop molds with 0.02 mm precision and long-life steel |
| Materials & consumables | Chemicals, lacquer, polishing media, films, wires and spare parts with long-term supply |
| Full-process capability | From raw material through weaving, forming, finishing, electroplating and painting - one responsible supplier |
| Turnkey services | Layout design, installation, commissioning, operator/technician training and remote support |
| Proven delivery | 10,000 m² self-owned plant, 35 senior engineers, export to 60+ countries |
Frequently Asked Questions
Where should a new zipper factory start?
Start with a clear product plan: product type, target daily output, workshop size, power supply and whether you have technical staff. QLQ prepares a customized machine list, layout and quotation from these answers.
How much investment does a new factory need?
A small factory at 10,000–20,000 pieces/day is around USD 80,000–150,000 for equipment; a medium factory at 30,000–50,000 pieces/day is around USD 150,000–300,000. This excludes building, utilities and working capital.
Should I buy one line at a time or the full line?
For a first factory, buy one complete line for one product type, run it 3–6 months, train the team, then expand. QLQ supports phased investment.
Can QLQ send engineers to install and train?
Yes. Online support is free; on-site commissioning with 1–2 engineers for 7–15 days is recommended for new factories, and longer technical support can be arranged. The customer covers visa, flights, hotel and meals.
Do zipper factories need environmental approval?
Usually yes when dyeing, plating or painting is in-house. Small factories can outsource plating/dyeing; medium factories should plan wastewater treatment and exhaust with the line design.
Can machines be customized for our voltage and frequency?
Yes. Common options include 380V/50Hz, 220V/60Hz, 415V/50Hz, 440V/60Hz and 480V/60Hz three-phase. Confirm the local standard and it is included in the PI.
What support is available after delivery?
Installation and commissioning, operator/technician training, spare parts and consumables supply, process optimization and remote troubleshooting form a closed support loop.
What Would You Like to Solve?
Share your product range, target output, workshop size and the process problem you are facing. QLQ engineering will help you check the machine list, layout, parameters and troubleshooting steps for your specific case.
Factory Setup Guide: Zipper Production Workshop
Whether you produce nylon, metal or plastic zippers, every profitable factory starts with the same planning data: quality standards, space, people, power and output targets. The table below summarizes realistic planning figures for a typical mid-size multi-type zipper workshop.
| Planning Item | Recommended Standard for a Typical Mid-Size Line |
|---|---|
| Quality Control Standards | ISO 9001 quality system with BS 3084 / ASTM D2061 / QB/T 2171 testing; incoming material inspection; in-process QC at each station; pull-force, slider cycling and color-fastness tests per batch; final AQL 2.5 sampling before packing. |
| Workshop Area Required | 1,000–2,500 m² for a complete multi-type line (nylon and plastic, or metal), plus 200–400 m² warehouse; ceiling height above 4.5 m; separate dyeing, plating (if any), assembly and packing zones. |
| Workforce Needed | 20–50 workers across two shifts: line operators, 2���4 machine technicians, 2–4 QC inspectors and 1–2 production managers; more staff are required when plating is done in-house. |
| Power Supply | 150–400 kW connected load depending on line type; 380V/50Hz three-phase (or 220V/480V 60Hz); compressed air at 0.6–0.8 MPa; water supply for dyeing, cooling or plating. |
| Daily Production Capacity | Finished zippers: 8,000–20,000 pcs/day across sizes #3–#10; chain production: 5,000–15,000 m/day, depending on the number and type of lines. |
| Estimated Gross Margin | 18%–30% on finished zippers; in-house dyeing, finishing and a balanced product mix support the higher end of the range. |
| Typical Investment Range | $150,000��350,000 for a complete mid-size multi-type line, excluding building construction and local environmental permits. |
| Typical Payback Period | 18–30 months at 70% average utilization with steady order volume. |
Quality First
- Test pull force and slider cycling on every batch
- Run incoming material inspection on all yarns and parts
- Keep in-process QC records at every handover
- Use AQL 2.5 sampling before shipping
Workshop & Power
- Plan production, warehouse and utility zones clearly
- Provide stable three-phase power with surge protection
- Ensure ventilation for dyeing, heating or plating areas
- Keep a dust-free packing and storage zone
People & Profit
- Train operators and technicians before production starts
- Assign QC inspectors to each major process
- Gross margin target: 18%–30%
- Payback target: 18–30 months
Note: figures are planning references for typical QLQ-equipped lines. Actual requirements vary with product mix, automation level, shift pattern, local power standards and environmental regulations.
Planning a new zipper factory or upgrading an existing workshop? Contact QLQ Machinery for a complete line design, equipment list and quotation matched to your target capacity.